Servicios de impresión 3D a medida
Turn CAD models into prototypes and low-volume parts with coordinated process selection, material review, printing, post-processing, and inspection.
- FDM, SLA & SLS
- Metal PBF by Review
- Prototypes & Small Batches
Choose the Right Printing Process
Match the process to geometry, material, accuracy, appearance, load, quantity, and the intended use of the part.
FDM / FFF
Thermoplastic filament printing for economical concept models, fixtures, and functional prototypes.
Review layer direction, infill, supports, bed adhesion, and visible layer lines.
SLA / DLP
Photopolymer printing for fine detail, smooth surfaces, and presentation or functional trials.
Supports, washing, and resin-specific curing influence final size and material behavior.
SLS
Polymer powder-bed printing for complex nylon parts and low-volume functional assemblies.
Surrounding powder supports the build; powder removal, access, and thermal distortion still need review.
Fusión en lecho de polvo metálico
Metal printing for reviewed complex structures, lightweight geometry, and consolidated components.
Confirm alloy availability, orientation, supports, heat treatment, distortion, and feature finishing.
3D Printing Capability References
These planning figures are reviewed for the selected process and machine. Part dimensions, orientation, supports, material, and finishing determine the accepted requirement.
Drawing-Based Parameters
| Build-size reference | Up to 750 × 550 × 550 mm*Platform-specific; this envelope is not available for every process or material. Supports and build clearance also affect usable size. |
|---|---|
| Typical dimensional reference | ±0.10–0.30 mm*Subject to process, feature size, material, orientation, geometry, and inspection condition. |
| Características de precisión seleccionadas | Down to ±0.05 mm*Accepted only after feature-specific review; the finishing and measurement route is agreed before production. |
| Minimum-wall references | SLA: 0.3 mm / FDM: 0.8 mm*Local design references, dependent on material, supported height, span, orientation, and function. |
| Hole-size reference | About 1.5 mm before finishing*Review axis, depth, shape, cleaning access, and any required drilling or reaming. |
| Layer-height reference | 0.05–0.30 mm*Selected platform settings. Layer height is not the same as dimensional accuracy or guaranteed surface roughness. |
Vía de producción controlada
1. Model and Job Review
Confirm revision, units, geometry, process, material, orientation, critical features, and acceptance criteria.
2. Build Control
Manage material condition, approved machine settings, support strategy, and the planned build.
3. Finishing and Inspection
Complete required post-processing before checking critical dimensions, surfaces, and specified function.
4. Release and Packing
Confirm agreed records, cleanliness, identification, surface protection, and packaging.
*Quotation references, not universal limits. Maximum size, minimum features, layer height, and tolerance are reviewed independently and should not be assumed achievable together.
3D Printing Materials
Compare the process, material behavior, typical use, and build controls before selecting an exact grade.
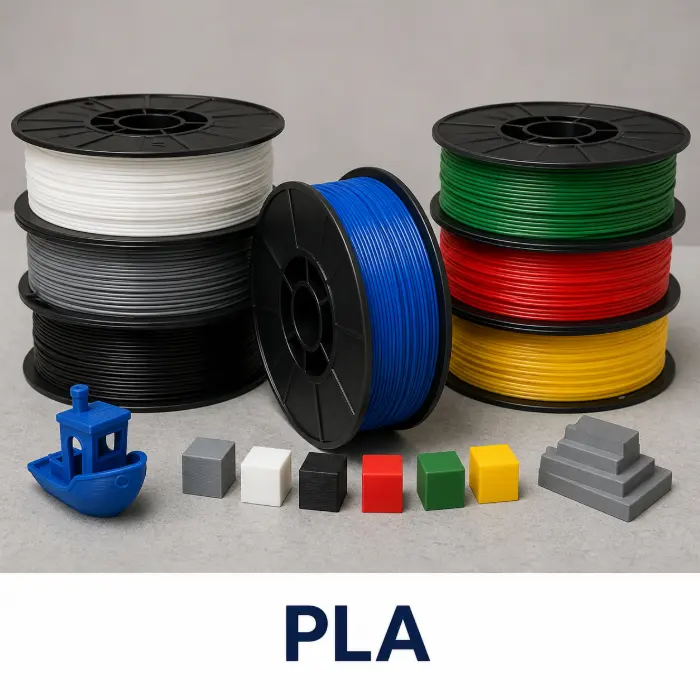
PLA
Rigid, economical material for visual prototypes and low-load development parts.
View material details
- Piezas habituales
- Concept models, display components, education models, and low-load fixtures.
- Build controls
- Select orientation, layer settings, supports, and cosmetic requirements for the intended model.
- Performance review
- Limited sustained-heat capability. Confirm load, temperature, and environmental exposure before functional use.
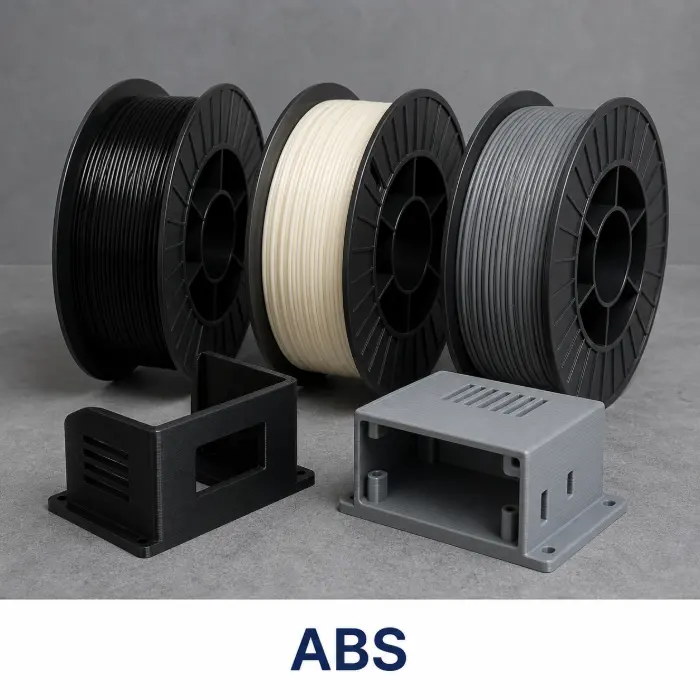
ABS
Tough thermoplastic for functional prototypes with useful impact and heat performance.
View material details
- Piezas habituales
- Carcasas de equipos, prototipos de automoción, plantillas y pruebas de ensamblaje a presión.
- Build controls
- Use suitable enclosure, bed adhesion, and cooling control to manage shrinkage and warping.
- Performance review
- Review the exact grade, layer direction, fits, impact requirements, and service temperature.
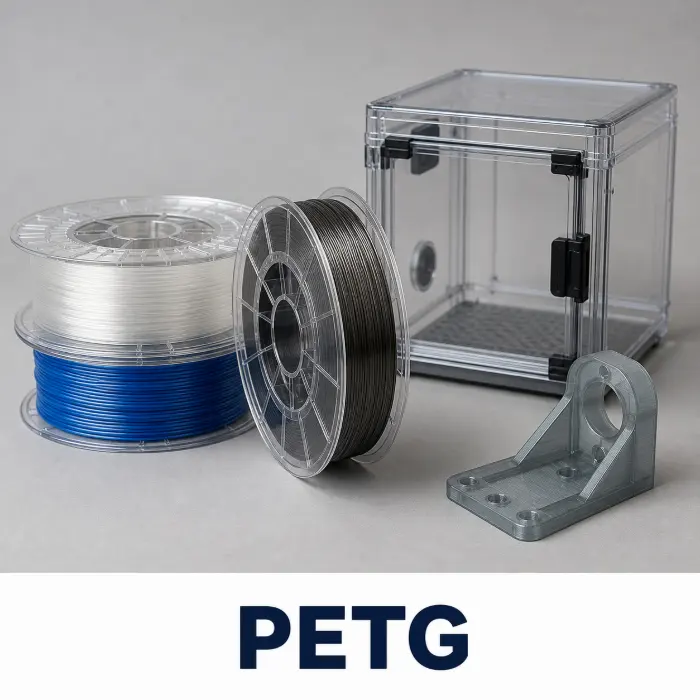
PETG
Good toughness and moisture resistance for general functional prototypes and housings.
View material details
- Piezas habituales
- Brackets, covers, functional housings, and mechanical development parts.
- Build controls
- Control filament moisture, cooling, feeding, and retraction to limit stringing and surface defects.
- Performance review
- Chemical resistance, UV exposure, temperature, and long-term loading remain grade- and application-specific.
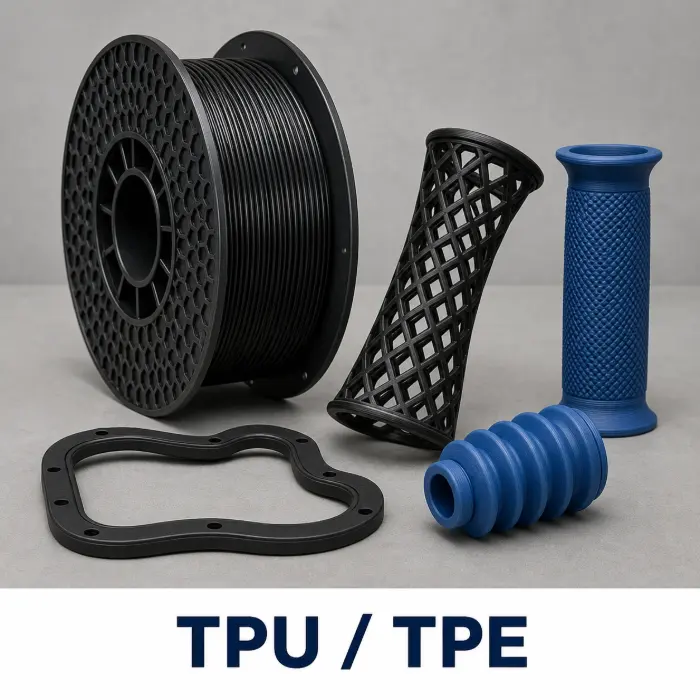
TPU / TPE
Flexible materials for compliant contact, cushioning, grip, and fit-check applications.
View material details
- Piezas habituales
- Grips, bellows, bumpers, flexible prototypes, and reviewed seal geometries.
- Build controls
- Match feed system, speed, drying, support, and wall design to the hardness and chosen grade.
- Performance review
- Confirm compression, recovery, abrasion, layer behavior, and leakage requirements where applicable.
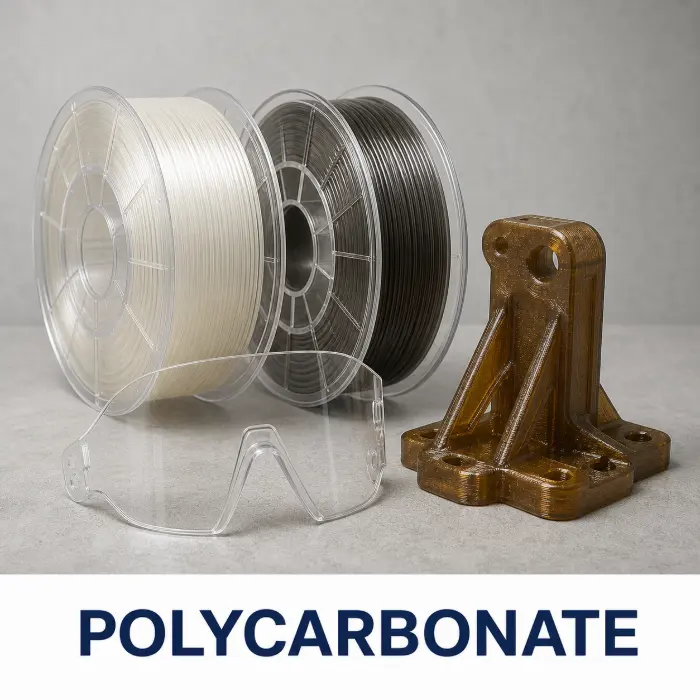
Policarbonato / PC
Impact-resistant thermoplastic for demanding functional and structural prototype work.
View material details
- Piezas habituales
- Guards, brackets, electronics housings, and loaded development components.
- Build controls
- Use dry material and appropriate nozzle, bed, and enclosed-chamber conditions for the selected grade.
- Performance review
- Review anisotropy, impact, temperature, stress, and required dimensional stability.
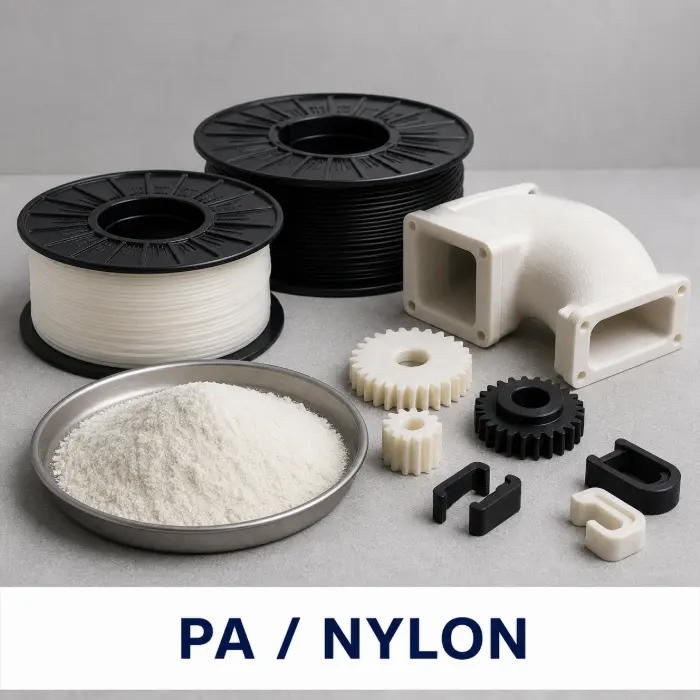
PA / Nylon
Tough, wear-resistant grades for complex mechanical prototypes and moving parts.
View material details
- Piezas habituales
- Engranajes, clips, conductos, guías, componentes deslizantes y carcasas funcionales.
- Build controls
- FDM filament and SLS powders require their own build and moisture controls. Define the condition for inspection.
- Performance review
- Confirm exact grade, process, moisture conditioning, load direction, and wear or fatigue requirements.
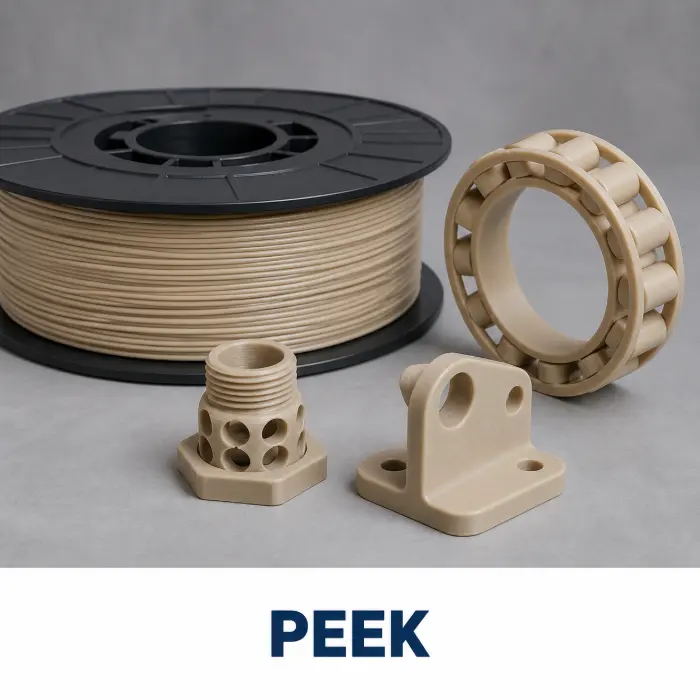
PEEK
High-performance polymer for reviewed thermal, chemical, and mechanically demanding applications.
View material details
- Piezas habituales
- Specialized fixtures, semiconductor components, and chemical-service development parts.
- Build controls
- Requires specialist equipment, controlled thermal conditions, material drying, and crystallinity review.
- Performance review
- Availability and feasibility are confirmed by engineering review; supplier properties are not automatic printed-part allowables.
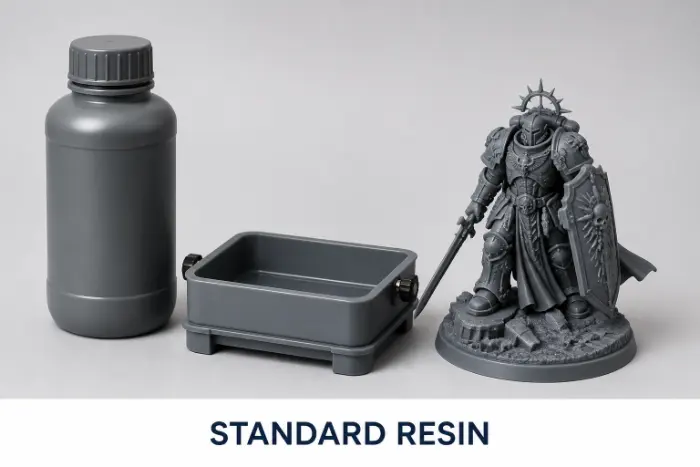
Resina estándar
Fine detail and smooth surfaces for visual evaluation and presentation models.
View material details
- Piezas habituales
- Detailed concepts, miniatures, display parts, and study models.
- Build controls
- Plan orientation, supports, washing, and the resin-specific post-cure.
- Performance review
- Generally selected for visual validation; sustained load, impact, heat, and outdoor use require separate review.
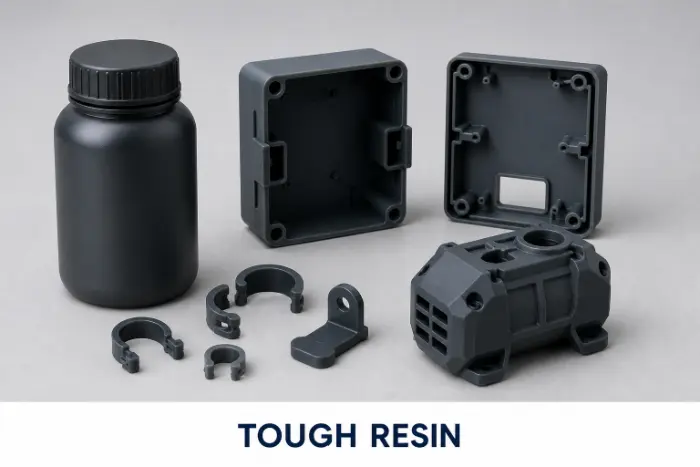
Resina resistente
Engineering photopolymers with improved toughness for handling and functional trials.
View material details
- Piezas habituales
- Clips, carcasas, comprobaciones de montaje y prototipos funcionales.
- Build controls
- Control support placement, washing, curing, and the specified inspection condition.
- Performance review
- Behavior remains grade-specific. Validate repeated loading, aging, sunlight, and the intended operating environment.
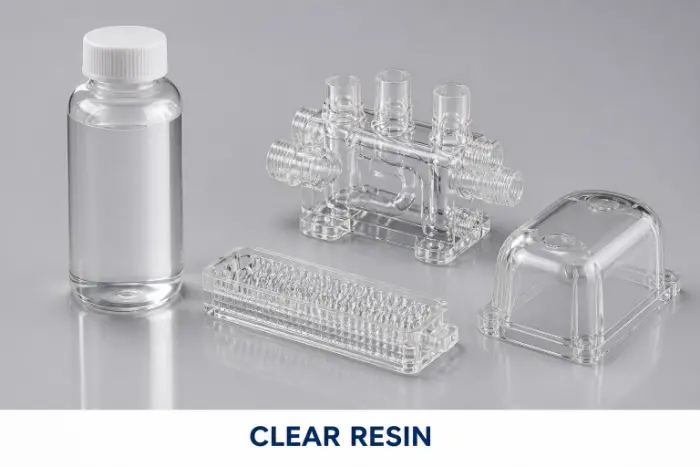
Resina transparente
Transparent or translucent prototypes with clarity developed through suitable finishing.
View material details
- Piezas habituales
- Fluid-visualization models, transparent covers, display parts, and reviewed light-transmission prototypes.
- Build controls
- Washing, curing, orientation, sanding, polishing, and coating determine the final surface and clarity.
- Performance review
- Define the visual or optical requirement; clear resin alone does not establish optical-grade performance.
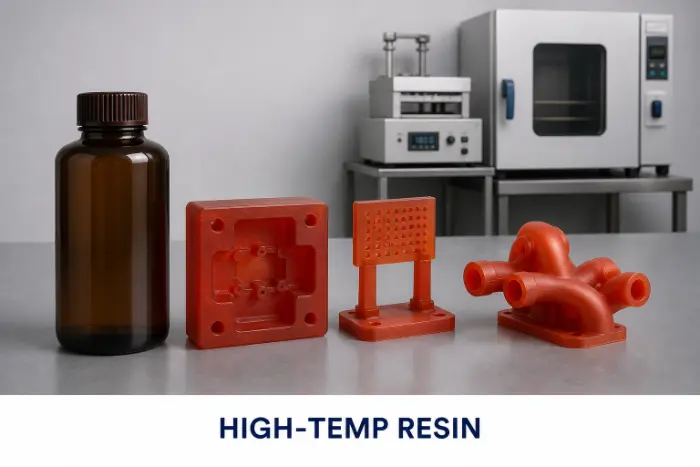
Resina resistente a altas temperaturas
Specialty resin for parts exposed to specified short-term thermal conditions.
View material details
- Piezas habituales
- Thermal test fixtures, reviewed short-run tooling, and hot-air test components.
- Build controls
- Follow the exact washing, cure, and thermal-conditioning schedule for the selected grade.
- Performance review
- Confirm temperature, exposure duration, load, and supplier test conditions; heat-deflection values are not continuous-use guarantees.
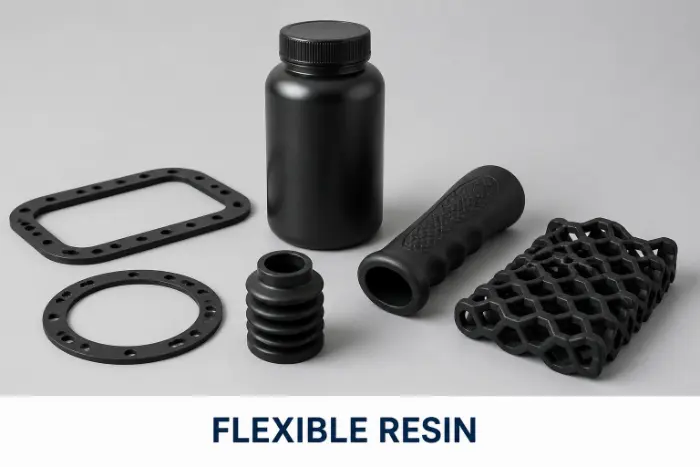
Resina flexible
Rubber-like photopolymer for detailed compliant parts and soft functional prototypes.
View material details
- Piezas habituales
- Grips, cushions, bellows, flexible fit-check parts, and reviewed seal prototypes.
- Build controls
- Select hardness, wall design, support placement, washing, and post-cure for the required shape.
- Performance review
- Check compression, recovery, repeated flexing, surface condition, and environmental exposure for the application.
For metal PBF, specify the required alloy and properties for a separate feedstock and process review. For every material, confirm the exact grade, orientation, post-processing, test conditions, and any application-specific documentation.
Design for Reliable Printing
Review the features that influence support, distortion, finishing access, strength, and fit before the build starts.
Espesor de la pared
Use process-appropriate sections and review unsupported broad surfaces, slender features, and local transitions.
Orientación de la construcción
Balance load direction, feature accuracy, support contact, visible surfaces, and build time.
Supports and Access
Plan removable supports where required, plus powder or resin escape routes and access for cleaning.
Orificios, roscas y acoplamientos
Identify critical bores, threads, datums, and sealing faces. Allow finishing stock or clearance where needed.
Dirección de carga
Account for anisotropy, layer bonding, infill, and build orientation rather than treating printed properties as uniform.
Acondicionamiento de materiales
Define drying, storage, post-cure, and the inspection condition for the selected polymer or resin.
Post-Processing for the Finished Part
Select finishing by material, function, appearance, cleanliness, and the dimensions that must be controlled after the print.
Eliminación del soporte
Remove breakaway, soluble, or metal supports using a method suited to the material and supported surfaces.
Acabado de la superficie
Review sanding, polishing, blasting, dyeing, or suitable coatings against appearance and dimensional requirements.
Resin Washing and Curing
Use resin-specific washing, drying, and curing conditions; the finished properties depend on the approved schedule.
Tratamiento térmico de metales
Apply stress relief, heat treatment, or HIP when specified and suitable for the selected alloy and production route.
Precision Feature Finishing
Finish critical bores, threads, locating surfaces, and sealing faces to the agreed drawing requirements.
Cleaning and Protection
Remove accessible process residue, inspect the agreed features, and protect finished parts during packing.
Where 3D Printing Adds Value
Rapid iteration, customized parts, complex geometry, and small batches can reduce development work before dedicated production tooling.

Medical and Dental Development
Anatomical and dental study models, device prototypes, and application-specific guides after material and process review.
Automoción
Piezas de diseño conceptual, utillajes de montaje, modelos de flujo de aire y prototipos de interiores a medida.
Electrónica
Housing concepts, brackets, and ergonomic development models.
Arquitectura
Scale models, façade studies, and presentation components.
Equipamiento industrial
Jigs, fixtures, guards, ducts, and reviewed low-volume functional parts.
Desarrollo de productos
Fast form, fit, and assembly evaluation before production tooling.
3D Printing Project Questions
Which file formats should I send?
STEP is preferred for engineering review. STL, 3MF, and OBJ files can be reviewed with clear units, scale, and suitable mesh quality. Add a dimensioned PDF for tolerances, datums, and features that need inspection.
Does a smaller layer height guarantee tighter tolerances?
No. Layer height affects build resolution and surface stepping, but dimensional results also depend on the machine, material, geometry, orientation, calibration, thermal behavior, and post-processing.
¿Cómo se pueden reducir las líneas visibles de las capas?
Choose a suitable process and orientation, then review layer settings and compatible finishing. Sanding, polishing, blasting, or coating may alter dimensions. Resin curing establishes properties but does not by itself remove visible stepping.
What causes warping?
Uneven thermal conditions, shrinkage, moisture, support or bed-adhesion problems, and unbalanced geometry can contribute. Controls are selected for the process rather than applying one method to all printing technologies.
¿Qué resistencia tienen las piezas impresas en 3D?
Strength depends on grade, process, orientation, infill where applicable, layer bonding, defects, and post-processing. Review the actual loading and test condition instead of treating bulk-material data as guaranteed printed performance.
When should another manufacturing process be considered?
Machining or molding may be more suitable when stock-material properties, tight fits, surface requirements, or repeat-volume economics are the priority. Compare the full production and finishing route.