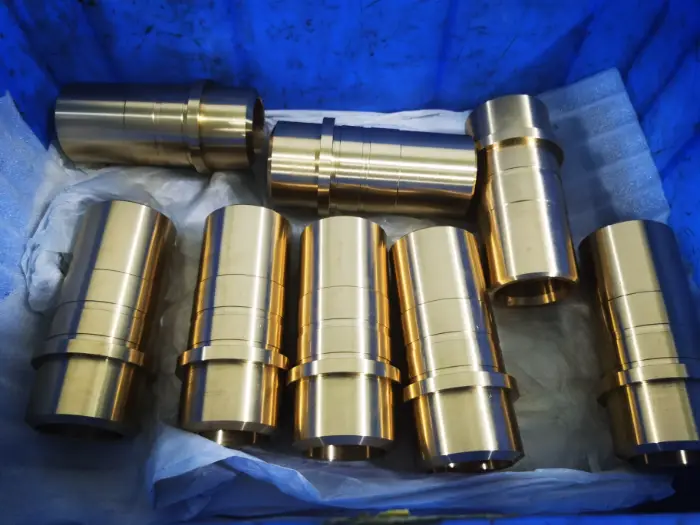
Bronze CNC Machining Services
Custom bronze parts made to drawing for bearings, bushings, gears, and precision mechanical assemblies. We match alloy, material condition, machining, and finish to the required wear, corrosion, load, and fit performance.
- Application-Based Alloy Selection
- プロトタイプから生産へ
- 仕上げ・検査
Bronze Properties Vary by Alloy Family
Bearing bronzes, aluminum bronzes, wrought spring alloys, and copper-beryllium grades provide different combinations of strength, wear, ductility, and conductivity.
- 密度
- 7.45–9.25g/cm³
- 引張強度
- 207–1,400MPa
- 降伏強度
- 95–1,200MPa
- 弾性係数
- Approx. 75–140GPa
- 電気伝導率
- Approx. 7–60% IACS
- 硬度
- Grade-SpecificSpecify test scale and condition
Broad references span selected bronze and copper-beryllium grades and conditions. They do not define one material or universal limits. Confirm the UNS grade, product form, casting route, temper, test method, and certified material data.
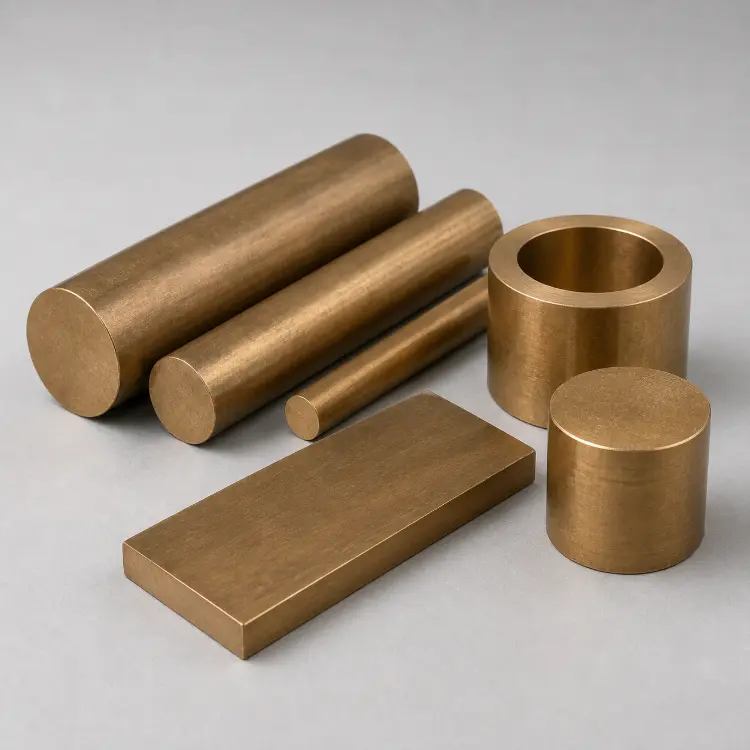
Choose the Bronze Alloy for the Part
Compare machining behavior, load, wear, lubrication, corrosion exposure, and the required material condition.
錫ブロンズ
A family of copper-tin alloys used for load-bearing, wear, and corrosion performance. Machining behavior and bearing suitability depend on the exact grade, casting route, and service conditions.
Grades, applications & machining notes
- Grade examples
- Cast grades: UNS C90300, C90500, and C90700.
- 代表的な部品
- Bushings, bearings, gears, valve guides, pump components, and piston rings in machinery and selected marine applications.
- Machining and bearing considerations
- Define running clearance, shaft finish and hardness, lubrication, load, and speed. Review casting quality and machining allowance; these grades should not be expected to compensate for severe misalignment or contaminated lubrication.
- 仕上げオプション
- Precision turning, boring, honing, grinding, or polishing as specified. Tin or nickel plating requires a defined functional purpose and allowance on critical surfaces.
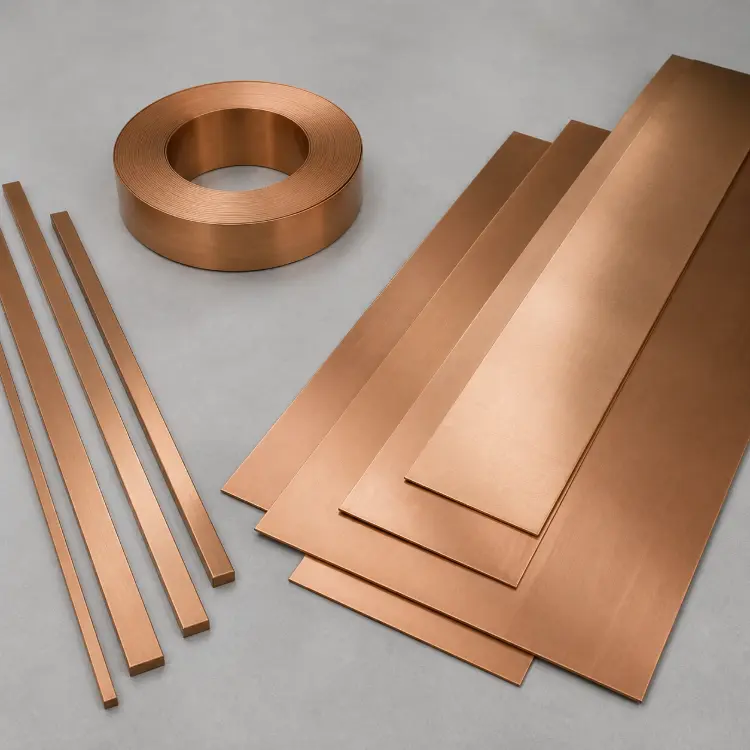
リン青銅
Wrought copper-tin-phosphorus alloys used for spring behavior, fatigue resistance, wear, and electrical contacts. Temper and product form strongly influence both machining and final performance.
Grades, applications & machining notes
- Grade examples
- Wrought grades: UNS C51000, C51900, and C52100.
- 代表的な部品
- Springs, electrical contacts, clips, thrust washers, small bushings, and selected precision mechanisms or gears.
- Machining and forming considerations
- Match cutting tools and support to the temper. For springs or formed contacts, define thickness, grain direction, forming route, and the required final mechanical properties.
- 仕上げオプション
- Deburring, polishing, brushing, and anti-tarnish protection. Tin, nickel, silver, or gold plating is selected for the electrical and service requirements.
- Material guide
- Explore phosphor bronze →
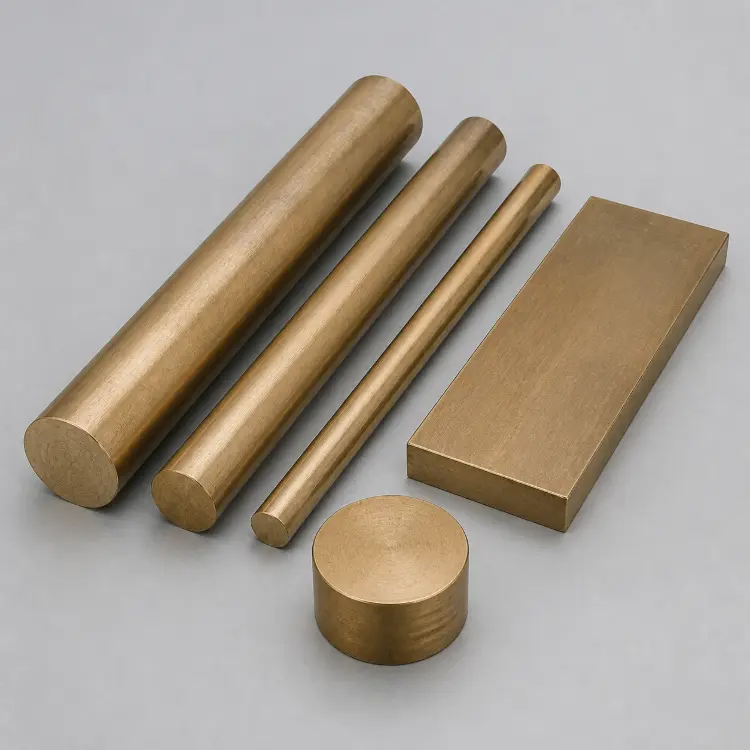
Aluminum & Nickel-Aluminum Bronze
High-strength copper-aluminum alloys for wear, demanding mechanical loads, and selected marine or pump duties. Grade and microstructure affect machinability, corrosion behavior, and impact performance.
Grades, applications & machining notes
- Grade examples
- Wrought: UNS C61400 and C63000. Cast: UNS C95400 and C95800, with C95800 commonly used as nickel-aluminum bronze.
- 代表的な部品
- Heavy-duty bushings, gears, valve seats, impellers, wear plates, and marine hardware.
- Machining and bearing considerations
- Use tooling suited to the grade, hardness, and abrasive behavior. Bearing applications need accurate alignment, suitable shaft finish, and reliable lubrication because conformability and dirt embedding are limited.
- 仕上げオプション
- Precision machining, grinding, polishing, or controlled abrasive blasting. Any plating process requires suitable pretreatment and defined adhesion and fit requirements.
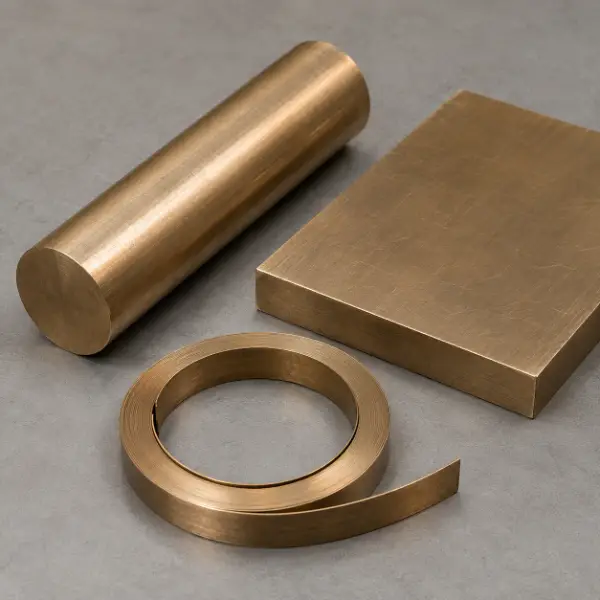
Beryllium Copper
Also marketed as beryllium bronze, these age-hardenable copper alloys balance strength, elasticity, fatigue resistance, and conductivity. High-strength and high-conductivity grades serve different requirements.
Grades, applications & machining notes
- Grade examples
- Wrought grades: UNS C17200, C17300, and C17510. These grades are not interchangeable solely because they contain beryllium.
- 代表的な部品
- Precision springs, contacts, diaphragms, bushings, and selected mold or tooling inserts. Specialized non-sparking applications require their own qualification.
- Machining and treatment considerations
- Define incoming temper, aging sequence, finishing allowance, and final inspection. Follow supplier guidance for controlled machining, dust-generating finishing, cleaning, and chip handling.
- 仕上げオプション
- Polishing, anti-tarnish treatment, or specified nickel, tin, silver, or gold plating. Confirm conductivity, contact performance, and dimensions in the final condition.
- Material guide
- Explore beryllium copper machining →
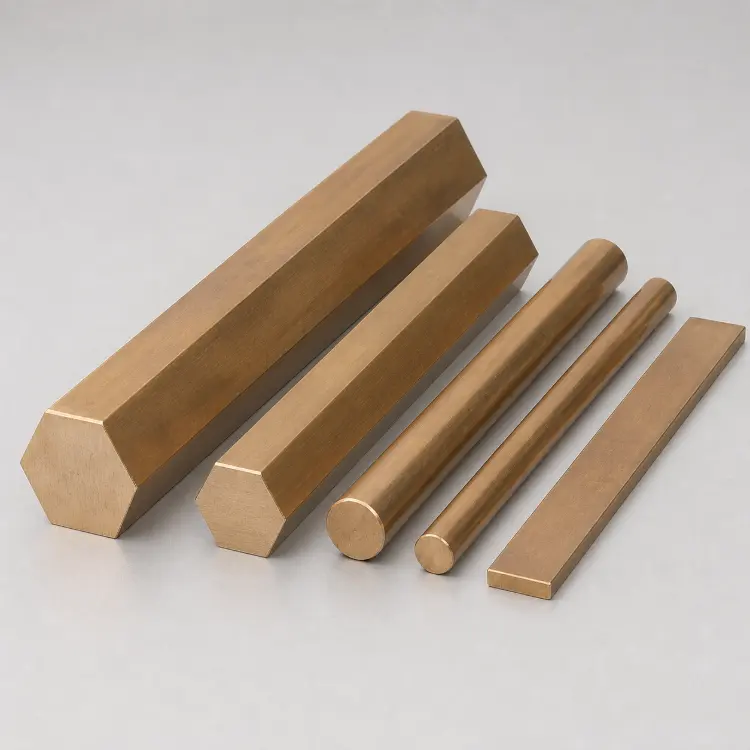
シリコン・ブロンズ
Copper-silicon alloys offering useful corrosion resistance, strength, forming, and joining characteristics. Supplied condition and product form determine the machining route.
Grades, applications & machining notes
- Grade examples
- Wrought grades: UNS C65100, C65500, and C65600.
- 代表的な部品
- Fasteners, valve stems, pump parts, fittings, brackets, and architectural hardware.
- Machining and stock considerations
- Confirm whether bar, plate, tube, forging, or casting is required. Match chip control, workholding, and cutting parameters to the exact grade and temper.
- 仕上げオプション
- Polishing, brushing, bead blasting, patination, or a clear protective coating. Decorative plating is applied with an agreed surface and dimensional specification.
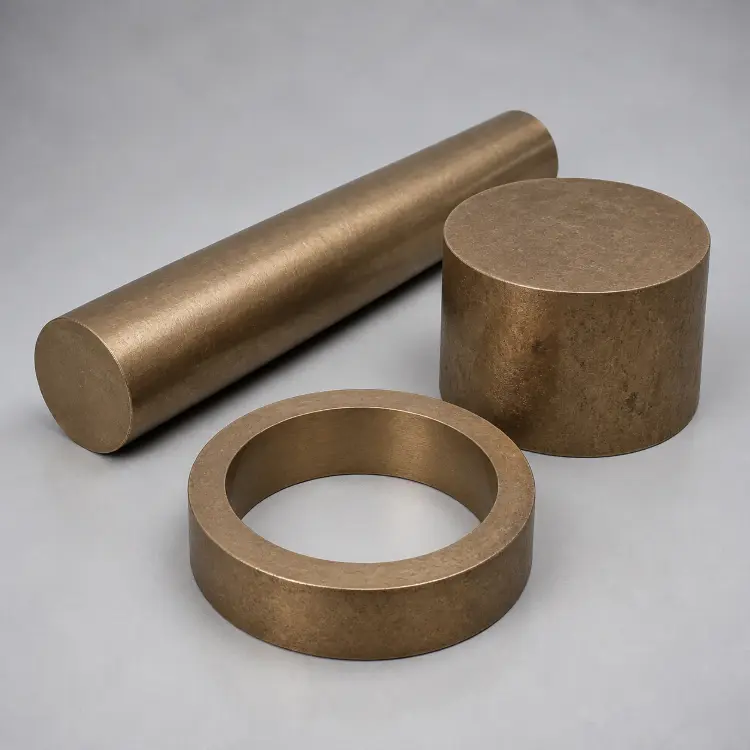
マンガン青銅
A commercial name for high-strength copper alloys used under heavy mechanical loads. These materials can require substantially different cutting strategies from softer bearing bronzes.
Grades, applications & machining notes
- Grade examples
- Cast commercial grades: UNS C86200, C86300, and C86400. In the UNS system, this group is classified as high-strength yellow brass.
- 代表的な部品
- Bridge bearings, rolling-mill nuts, bushings, gears, guides, and wear plates for construction and industrial machinery.
- Machining and bearing considerations
- Review casting condition, hardness, tool wear, and workholding. Define running clearance, alignment, lubrication, and final bearing geometry for the actual duty.
- 仕上げオプション
- Precision machining, grinding, and polishing. Oils, waxes, lacquers, or specified plating may protect suitable non-working surfaces.
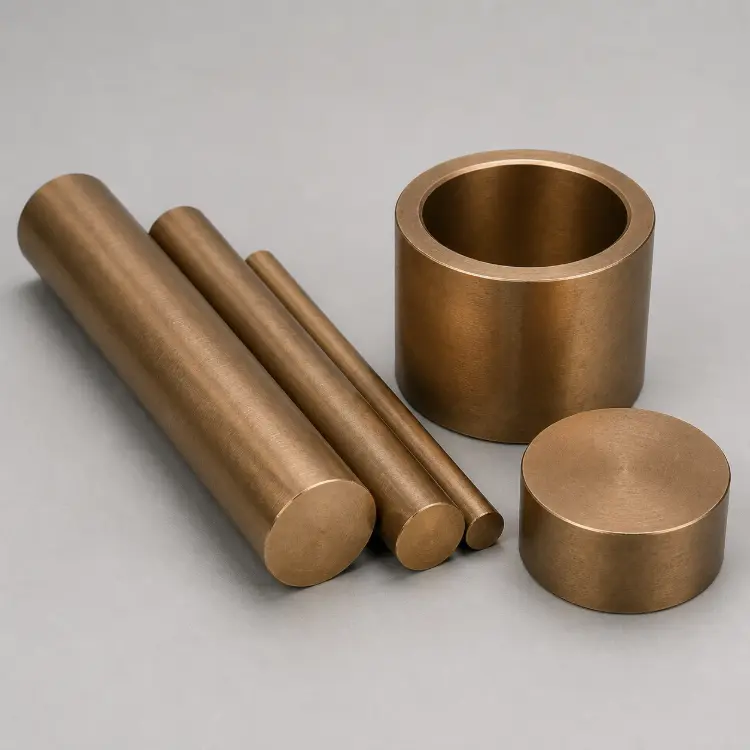
鉛入り錫青銅
Bearing alloys known for machinability, conformability, debris embedding, and resistance to seizure under suitable operating conditions. Lubrication, clearance, load, and speed remain part of the design.
Grades, applications & machining notes
- Grade examples
- Cast grades: UNS C93200, C93600, and C93700.
- 代表的な部品
- Sleeve bearings, bushings, thrust washers, and selected pump bearings, including reviewed boundary-lubricated applications.
- Machining and bearing considerations
- Use controlled boring, turning, and groove machining to achieve the specified fits and edges. These grades are not a universal substitute for oil-impregnated or other self-lubricating bearing systems.
- 仕上げオプション
- Precision turning, boring, honing, and lubricant-groove machining. Working faces need an agreed finished condition; coatings and storage protection must suit the bearing function.
- Material requirements
- These grades contain lead. State any lead-content, contact-material, or finished-product qualification requirements before material approval.
Commercial family names can overlap. Specify the exact UNS grade and material condition, together with product form, required records, and operating conditions for the finished part.
Drawing-Based Bronze Machining Capabilities
Review the alloy, casting or stock condition, wall thickness, workholding, and inspection plan before confirming the manufacturing route.
Machining Reference Parameters
| フライス加工範囲 | 最大 3000 × 1600 × 1000 mm*Subject to machine selection, stock availability, clamping, and tool access. |
|---|---|
| Turning capacity | Up to Ø200 × 1000 mm*Diameter, length, support, geometry, and rigidity require a combined review. |
| General dimensional reference | ±0.05 mm*Quotation reference. Drawing tolerances and measurement conditions are agreed for the part. |
| 主な高精度機能 | Down to ±0.01 mm*Confirmed after feature-specific engineering and inspection review. |
| 加工面粗さ | Ra 0.8–3.2 µm*Depends on alloy, material condition, surface geometry, tooling, and finishing. |
| Thin-wall reference | From 0.8 mm*Depends on wall height, unsupported span, stock condition, clamping, and final fit. |
Controls for Functional Bronze Parts
Match the Cutting Strategy
Choose tooling, cutting geometry, feeds, and speeds for the actual alloy, hardness, chip behavior, and stock condition.
Review Stock and Castings
Confirm material records, machining allowance, cast-surface condition, and any required soundness or treatment requirements.
Support Thin Sections
Use stable distributed support and controlled clamping to limit movement in bushings, sleeves, and split components.
機能用穴の確認
Define bore size, form, alignment, surface finish, and acceptance after release from the fixture or final assembly condition.
*Planning references confirmed against the complete drawing. Maximum size, thin walls, precision, and roughness are assessed separately and should not be assumed achievable together.
Weldo Bronze Machining Projects
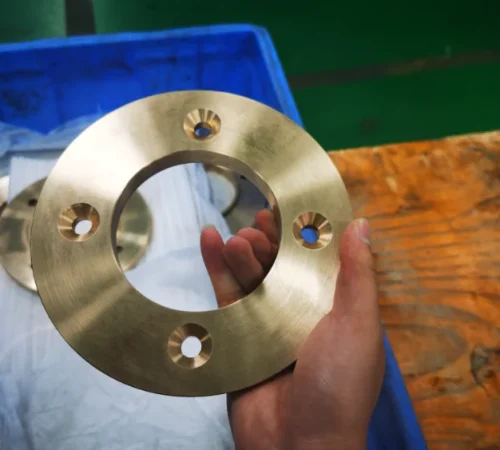
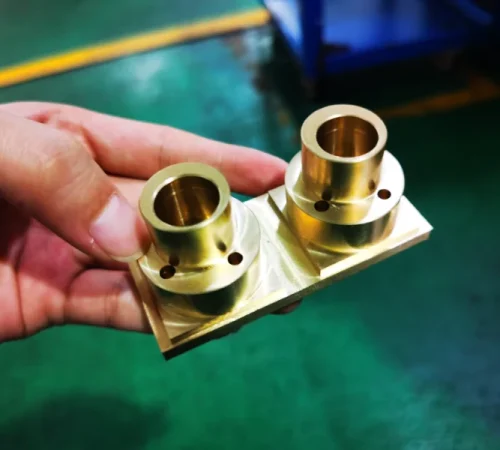
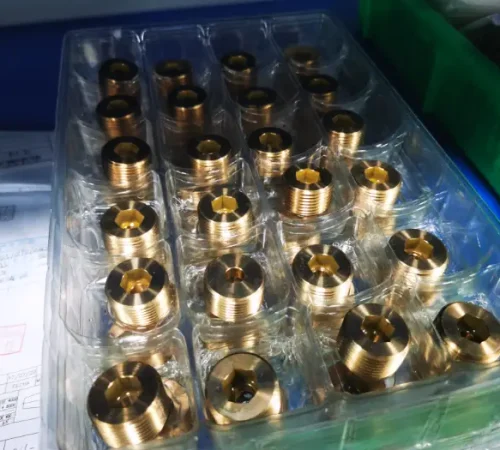
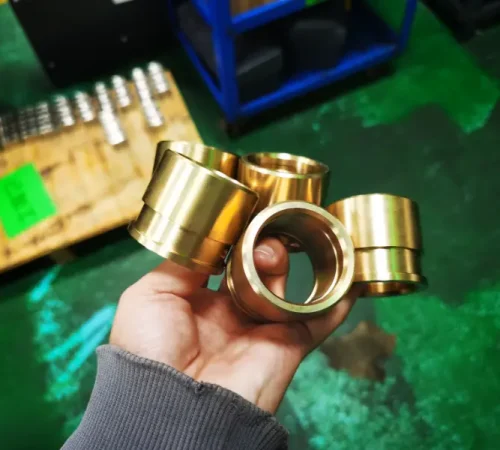
Examples of bronze machining projects completed by Weldo, including custom components for bushings, housings, fittings, and precision mechanical assemblies.
青銅部品の表面仕上げ
Select the finish for corrosion exposure, wear, friction, contact performance, and appearance. Define the finished condition of bearing surfaces and critical fits.
研磨・ブラッシング
Create a controlled satin or bright surface. Specify the visual reference, roughness, and any critical edge or bearing geometry.
ビーズブラスト
Produce a matte texture using suitable clean media and masking. Define any subsequent coating and protect functional surfaces.
化学的パティナ
Create specified brown, dark, or aged tones. Agree the color reference, preparation, and protective topcoat where required.
Anti-Tarnish Protection
A suitable inhibitor, such as a specified BTA-based treatment, lacquer, or wax, can help limit tarnish on compatible surfaces.
金属メッキ
Specify nickel, chrome, tin, silver, or gold systems for the required contact, wear, or appearance performance, including pretreatment and thickness.
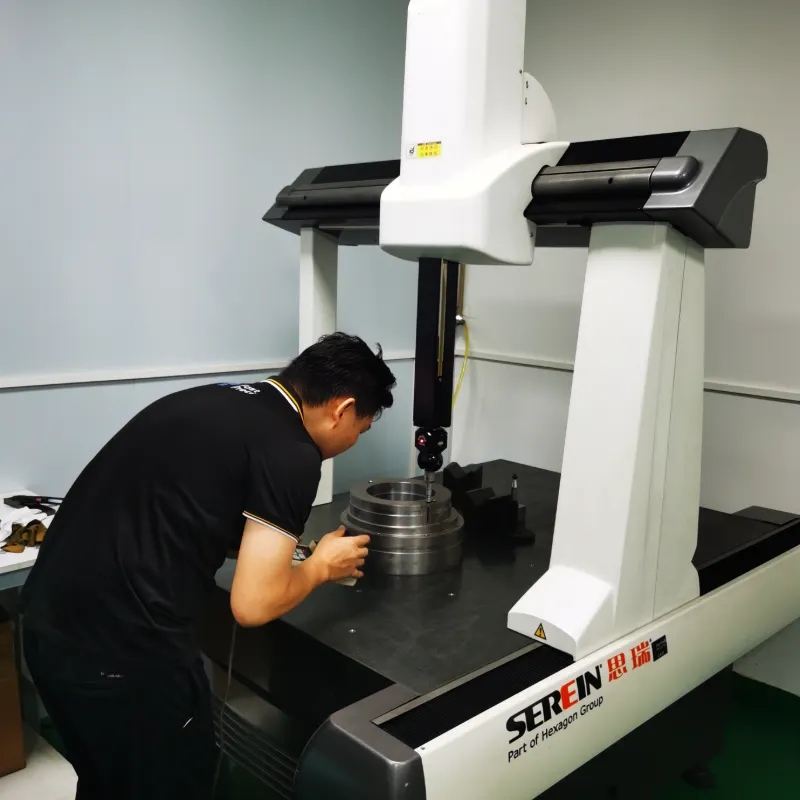
材料審査から最終検査まで
Identify critical interfaces before machining and verify the agreed drawing requirements in the finished condition.
Material Review
Confirm the grade, stock or casting route, condition, and required material records.
Datum Control
Plan workholding and machining sequences to maintain critical feature relationships.
In-Process Checks
Monitor bores, threads, wall thickness, and functional dimensions during production.
最終確認
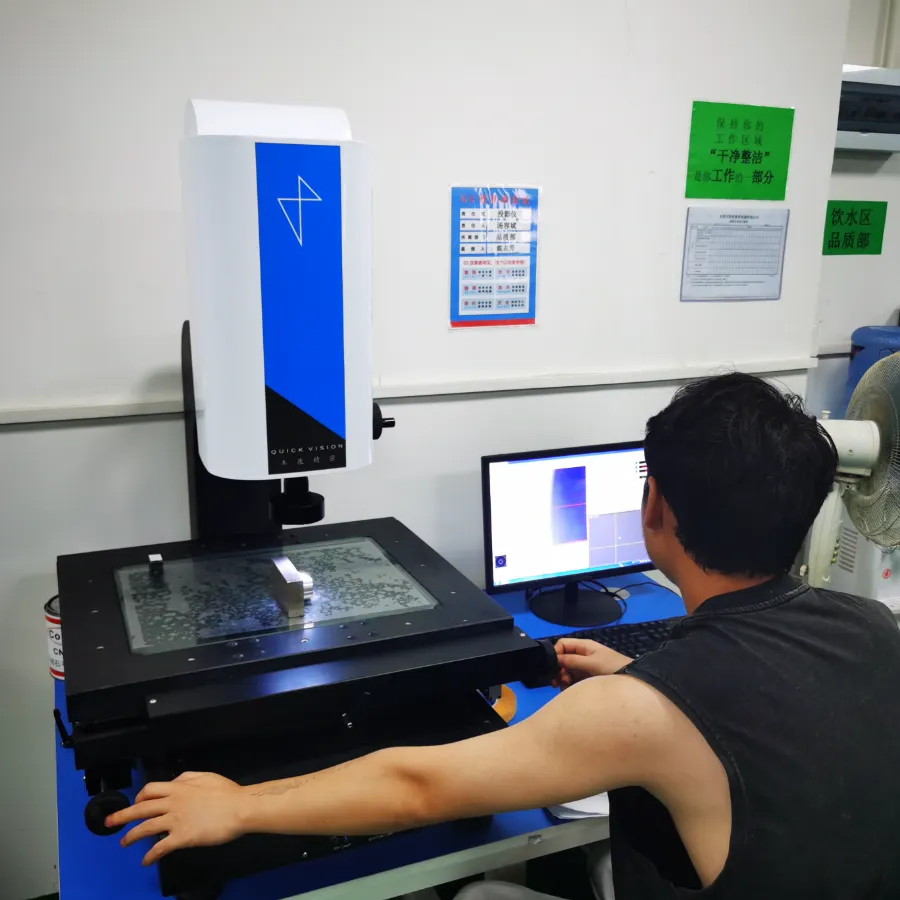
Use suitable dimensional, CMM, or optical inspection for the specified features and records.
Bronze Machining Questions
Is bronze easy to machine?
Machinability varies substantially by grade and condition. Leaded bearing bronzes generally machine well, while aluminum bronzes and high-strength copper alloys can require different tooling, engagement, and chip-control strategies. Specify the actual alloy before comparing production routes.
What are the main machining challenges?
Tool wear, adhesion, burrs, casting variation, and movement in thin sleeves can affect the result. Use tooling suited to the alloy, stable workholding, controlled cutting parameters, and a planned deburring and inspection sequence.
Can bronze bearings run without lubrication?
Do not assume that a solid machined bronze bearing can run dry. Suitability depends on the alloy, pressure and speed, clearance, shaft surface, temperature, and bearing design. Oil-impregnated, graphite-plugged, and other self-lubricating products are distinct engineered systems.
How can bronze machining costs be reduced?
Select a suitable available stock size and machinable grade, apply tight tolerances to functional features, and keep deep or narrow geometry accessible to tools. Clear datum, finish, and inspection requirements help avoid extra setups and rework.
Can bronze parts be plated or given a patina?
Yes, with a suitable process for the alloy and intended use. Specify surface preparation, coating thickness, masking, appearance, and finished dimensions. Bearing and contact surfaces require a defined functional condition after treatment.
Are cast and wrought grades interchangeable?
They can differ in composition, microstructure, mechanical properties, stock availability, and permitted defects. Specify the exact UNS grade, product standard, condition, and required records before approving a substitution.