
Acrylic CNC Machining Services
Custom acrylic and PMMA parts made to drawing for windows, light guides, covers, manifolds, and precision assemblies. Weldo reviews stock, geometry, cutting, finishing, and inspection around your dimensional and appearance requirements.
- Acrylic & PMMA Options
- プロトタイプから生産へ
- 仕上げ・検査
Mechanical and Optical Property References
Representative room-temperature values for selected clear, general-purpose PMMA grades. Formulation, thickness, test method, and material condition affect the result.
- 密度
- 1.18–1.19g/cm³
- 引張強度
- 60–77MPa
- 引張弾性率
- 3.0–3.3GPa
- Visible-Light Transmission
- 最大 92%Clear grades; thickness-dependent
- 屈折率
- Approx. 1.49Wavelength- and grade-dependent
- 熱偏向温度
- 90~98°CSelected grades at 1.8 MPa
Verify supplier-grade data for design. Heat deflection temperature is a test result, not a continuous-use temperature. Optical, impact-modified, colored, and medical formulations require their own data and material records.
Choose the Acrylic Material for the Part
Match stock form and formulation to clarity, impact, weather exposure, dimensional needs, and the finishing route.
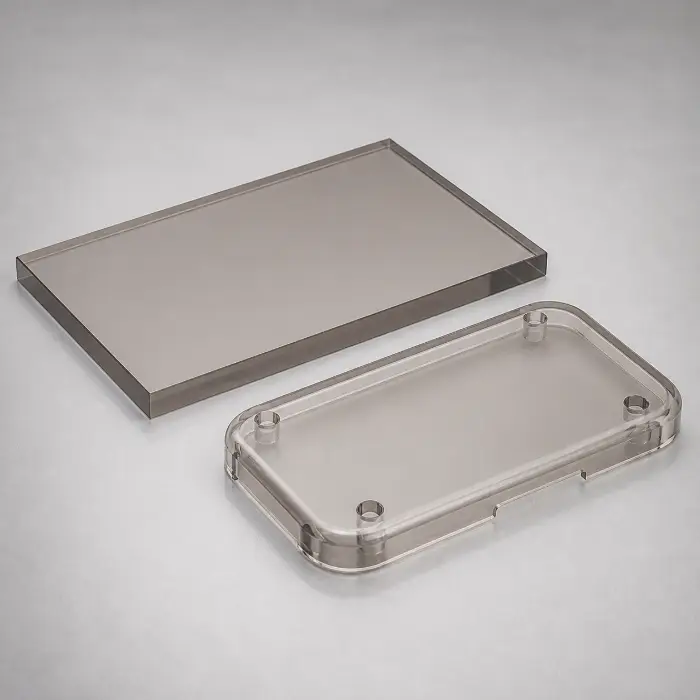
キャストアクリル(PMMA)
Often selected for detailed machining and polishing where stock stress, surface quality, and dimensional stability matter.
Applications & machining notes
- 代表的な部品
- Windows, light guides, covers, manifolds, and display components.
- Selection and processing
- Review supplier stock stress, thickness variation, finishing allowance, and any bonding or polishing sequence. Cast sheet is not automatically free of residual stress.
押出成形アクリル(PMMA)
Consistent sheet thickness and economical stock options for panels, profiles, and simpler machined parts.
Applications & machining notes
- 代表的な部品
- Faceplates, signs, covers, panels, and housings.
- Selection and processing
- Confirm supplied thickness and stress condition. Control cutting heat, support, and compatible coolant; review annealing for stress-sensitive finishing or bonding.
光学用PMMA
Selected formulations and stock quality support defined transmission, haze, uniformity, and optical-surface requirements.
Applications & machining notes
- 代表的な部品
- Instrument windows, light guides, illumination parts, and selected lenses.
- Selection and processing
- Identify optical faces, surface form, clarity, haze, wavelength, and inspection requirements. A polished appearance alone does not establish optical performance.
耐衝撃性アクリル樹脂
Modified formulations improve impact performance compared with conventional acrylic, with grade-specific stiffness and clarity.
Applications & machining notes
- 代表的な部品
- Protective covers, machine windows, shields, and housings.
- Selection and processing
- Specify the actual impact, clarity, temperature, and chemical requirements. Match tools and finishing to the chosen formulation.
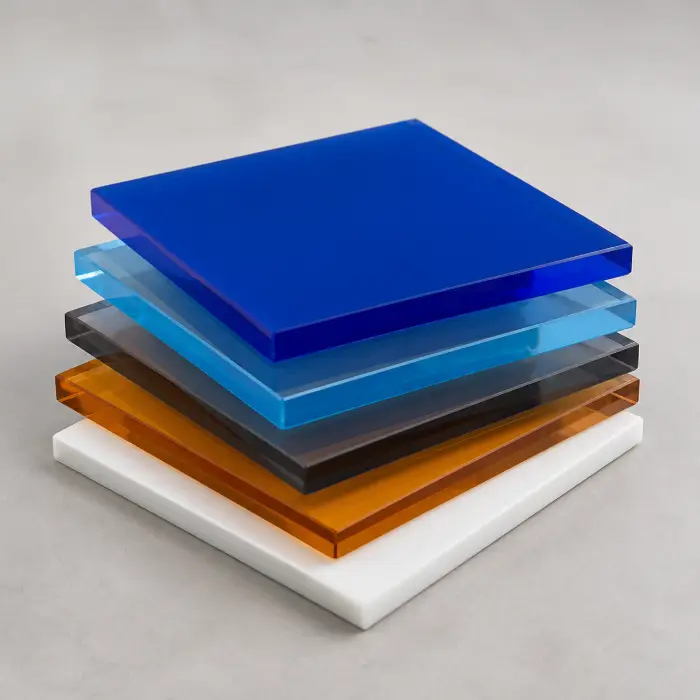
Colored & UV-Resistant PMMA
Tinted, opaque, and outdoor grades offer options for appearance, light transmission, and weathering requirements.
Applications & machining notes
- 代表的な部品
- Signs, indicators, lenses, panels, and decorative covers.
- Selection and processing
- Define color reference, light transmission, surface texture, and the intended outdoor exposure. Verify supplier-grade weathering data.
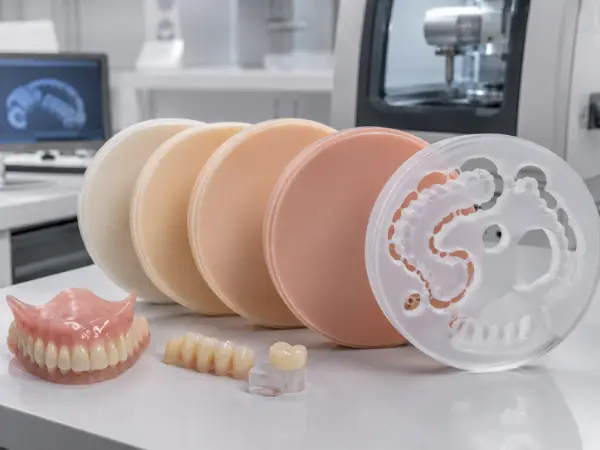
Medical & Dental PMMA
Documented grades for specified dental, medical, or laboratory components, with material condition and processing requirements defined.
Applications & machining notes
- 代表的な部品
- Dental discs, guides, covers, fixtures, and laboratory components.
- Selection and processing
- Specify the exact supplier grade, material records, cleanliness, and application requirements. Explore dental PMMA →
Drawing-Based Acrylic Machining Capabilities
Confirm grade, stock thickness, geometry, workholding, finishing, and inspection before accepting dimensional or optical requirements.
Machining Reference Parameters
| Work-envelope reference | Up to 3000 × 1200 × 850 mm*Subject to stock, equipment, support, clamping, and tool access. |
|---|---|
| Dimensional references | General ±0.1 mm / selected features ±0.05 mm*Confirm feature geometry, stock condition, inspection temperature, and final treatment. |
| Thin-wall reference | From 2.0 mm*Review wall height, unsupported span, handling, and optical or cosmetic requirements. |
| Internal-radius reference | From R0.5 mm*Subject to cutter access, depth, tool reach, edge quality, and part function. |
| 加工面粗さ | Ra 0.8–5 µm*Tool texture and roughness are distinct from optical clarity and surface-form acceptance. |
Controls for Acrylic Parts
Cutting Heat and Chips
Use sharp tools, suitable engagement, and reliable chip removal to limit rubbing, melting, and edge damage.
低ストレスのワーク保持
Support the part and control clamping to limit marks, deflection, and cracking around thin sections or holes.
Stress and Compatibility
Review stock condition and compatible coolants, cleaners, adhesives, and inks. Use supplier-specific annealing where appropriate.
Optical and Dimensional Acceptance
Define optical faces, datums, roughness, clarity, inspection method, and acceptance after polishing or coating.
*Planning references confirmed against the complete drawing. Maximum size, thin walls, small radii, tolerance, and roughness are assessed separately and should not be assumed achievable together.
Weldo Acrylic Machining Projects
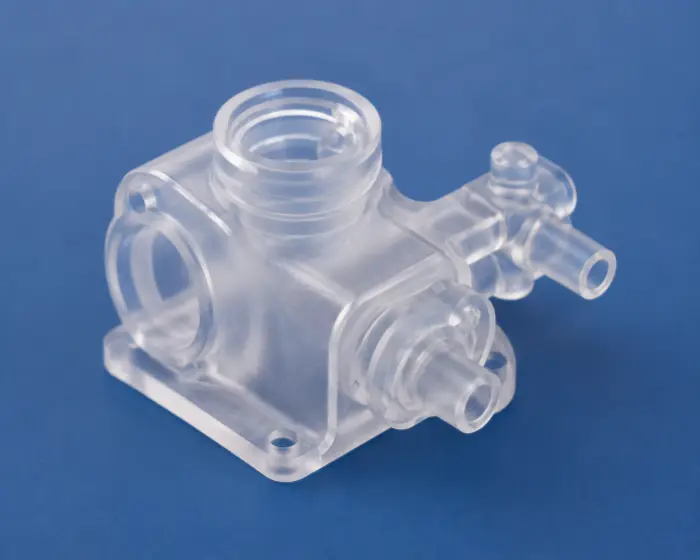
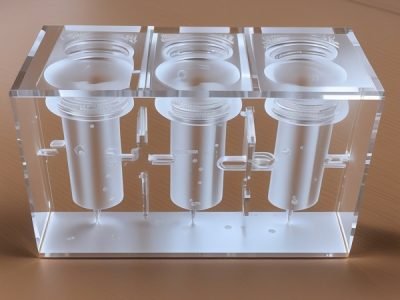
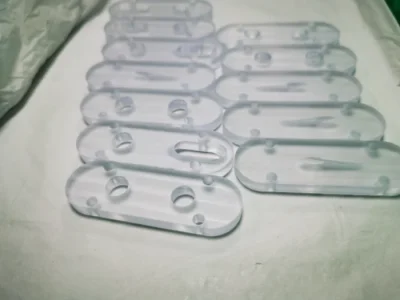
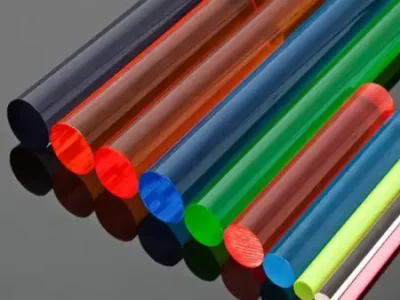
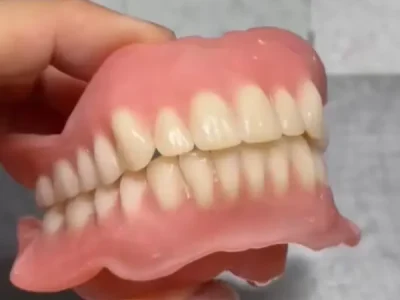
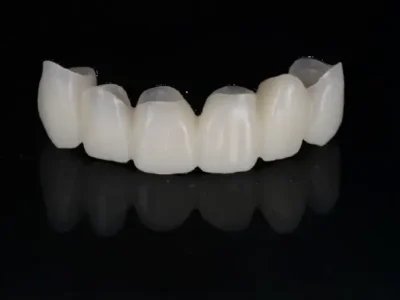
Examples of machined PMMA components, clear parts, discs, and material forms used in Weldo acrylic projects.
アクリルおよびPMMA部品の表面仕上げ
Select the process for transparency, gloss, texture, graphics, and scratch resistance, with optical and dimensional acceptance defined in advance.
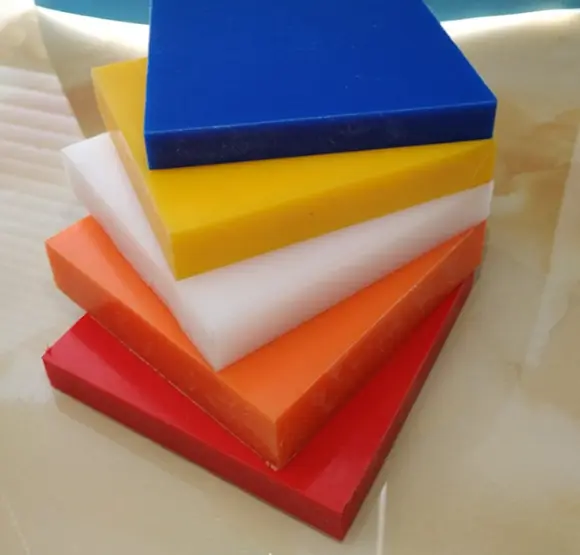
機械加工
A functional surface with controlled tool marks, deburring, and edge condition. Define any cosmetic or optical faces.
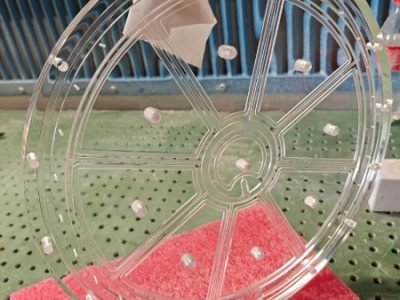
機械研磨
Reduce surface marks and improve gloss using a compatible process, with heat, edges, and dimensions controlled.
ダイヤモンド研磨
Selected edge or surface finishing for compatible geometry. Specify surface quality and optical acceptance separately.
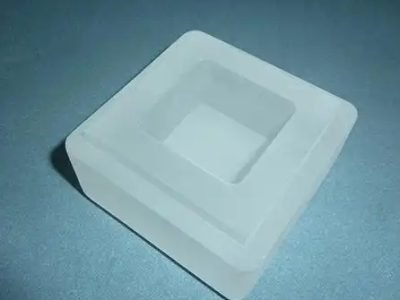
つや消し仕上げ
Create a specified matte texture or diffusion effect. Agree the visual reference, roughness, and protected areas.
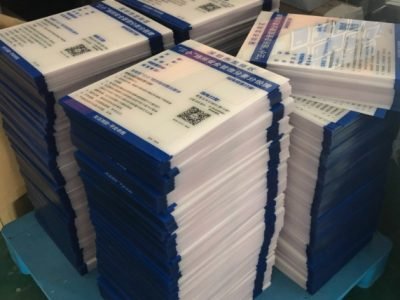
Printing & Marking
Apply specified text, scales, or graphics using compatible inks and preparation. Define adhesion, wear, and clarity requirements.
ハードコーティング
Selected coating systems can improve scratch resistance or provide other surface functions. Agree chemistry, thickness, and acceptance.
From Drawing Review to Protected Delivery
Identify optical faces, material condition, surface requirements, and the acceptance method before production.
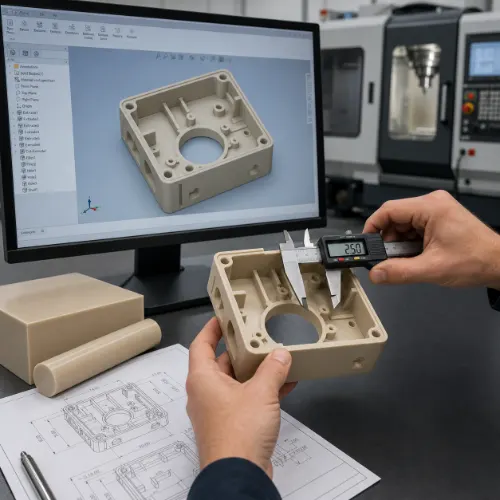
DFMレビュー
Confirm grade, geometry, tolerances, optical faces, and the finishing and inspection sequence.
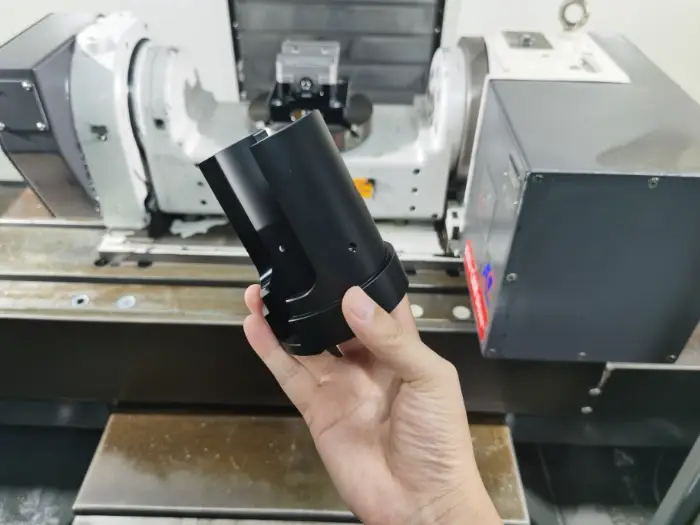
Process and Stress Control
Monitor tooling, clamping, chip removal, heat, and any specified conditioning or annealing.
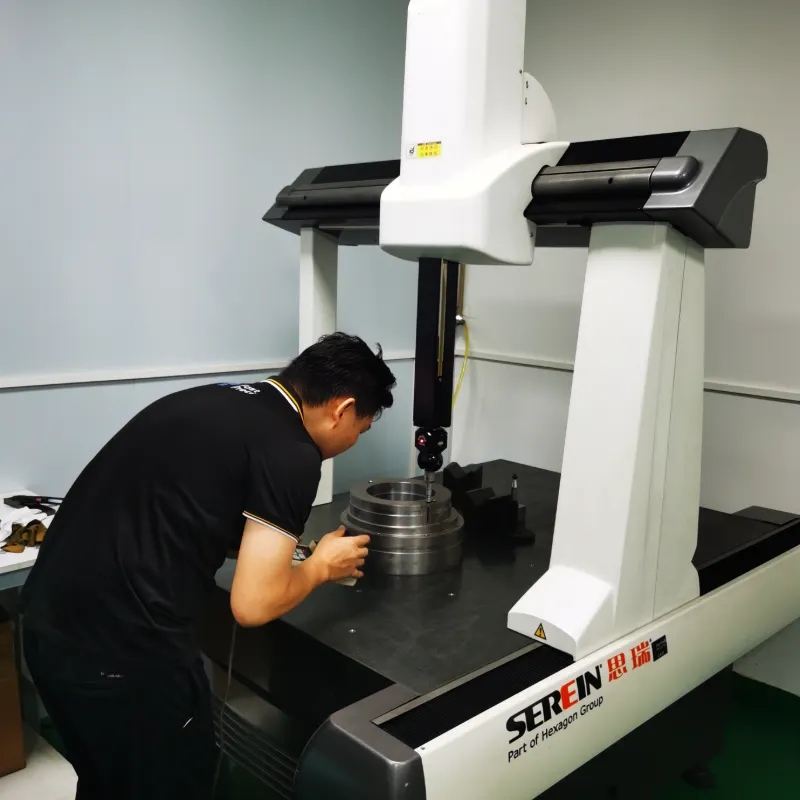
Finished-Part Inspection
Verify critical dimensions, surface condition, and the agreed optical features using suitable methods.

Protected Packing
Clean with compatible methods and protect finished surfaces and edges against handling scratches.
Acrylic Machining Questions
How are cracking and crazing reduced?
Review low-stress stock, sharp tools, controlled support, cutting heat, and chemical compatibility. Supplier-specific annealing may be appropriate when machining, polishing, bonding, or later exposure can reveal residual stress.
Which cutting tools suit acrylic?
Sharp, polished carbide tools with suitable flute geometry and chip space are common choices. Single-flute or O-flute tools can suit routing, while other tools may suit rigid milling. Match the tool to the actual operation and stock.
What machining speed should be used?
Select speed and feed from cutter diameter, flute count, engagement, machine rigidity, material, and the required finish. Use tool-supplier guidance and a validated cutting plan that produces clean chips without rubbing or melting.
How can machining costs be reduced?
Choose practical stock thicknesses, accessible features, adequate internal radii, and tolerances limited to functional needs. Define optical faces early so polishing and inspection are applied where required.
Can acrylic parts have machined threads?
Yes, with suitable thread geometry, wall thickness, edge distance, and assembly loads. Inserts may suit repeated assembly, but their installation method and fit must be compatible with PMMA and its cracking sensitivity.