
精密バー送り加工
スイスのCNC加工サービス
ウェルド社は、標準的な旋盤では 振れ、形状の位置合わせ、表面品質を維持することが困難な 小径で細長い部品を製造しています。 ガイドブッシングによる支持と、 旋削・フライス加工・穴あけ・裏面加工の連携により、 試作から量産に至るまで、たわみや セットアップごとのばらつきを低減します。.
スイス式機械加工を選ぶ理由
切断点で部品を支える
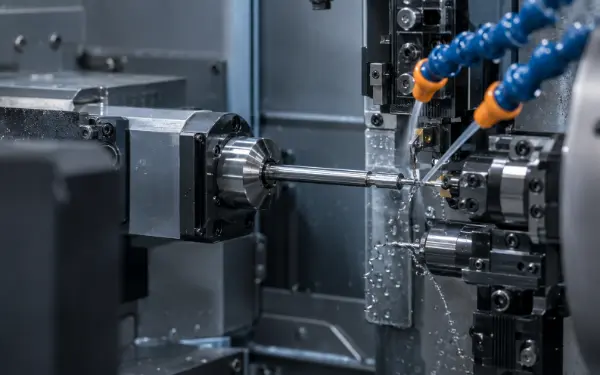
スライド式ヘッドストックがガイドブッシングを通して棒材を送り出し、工具が支持点のすぐ隣で切削を行う。支持されていない部分が短いため、細長い形状のワークにおけるたわみ、チャタリング、および径のずれが抑制される。.
制御された細長い形状
ガイドブッシングの横で切断することで、支持されていないバーの長さが短くなり、たわみ、テーパー、振動の抑制に役立ちます。.
旋削とフライス加工を同時に行う
直径、面取り、溝、貫通穴、およびねじは、すべて同じプログラム座標系に紐付けられたままとなります。.
フロントおよびリアの完成
サブスピンドルは切断前にワークを受け入れるため、手作業による再固定を行うことなく、裏面、穴、面取りの仕上げ加工を行うことができます。.
安定した生産
バーの供給を制御し、工具の順序を安定させることで、繰り返し受注においても一貫したサイクルタイムと検査結果が確保されます。.
1つのスイスサイクルに統合された操作
これらの数値はあくまで見積りの目安であり、普遍的な限界値ではありません。承認された図面、材料、棒材の状態、形状特性、および検査計画によって、最終的な製造能力が決定されます。.
パーツのファミリー
バーを基に製造された精密部品
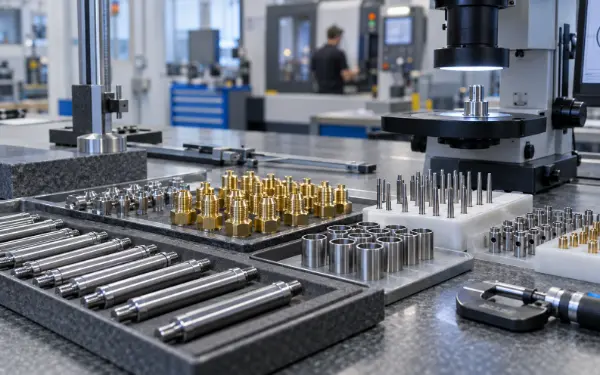
最適な候補は、回転対称形状と、精密な形状間の 関係性を兼ね備えています。以下の各部品ファミリーは、 加工ルートを決定づける機能要件をそれぞれ示しています。.
精密シャフト・ピン
ダボピン、バルブステム、プローブシャフト、およびアクチュエータピンは、 直径の均一性、真直度、振れ量、 および先端形状の管理を重視して製造されています。.
ブッシングおよびスリーブ
内径と外径の加工順序を調整することで、 過度なクランプ圧をかけずに、肉厚、同軸度、および端面の位置関係を 制御します。.
継手・コネクタ
ポート、シール溝、横穴、面取り、ねじ切りは、 切断前に完了させることができるため、基準面の変更や二次的な 取り扱い作業を削減できます。.
医療・機器用部品
小型のねじ付き金具、ガイド、および機器部品には、 トレーサビリティのある材料、バリの適切な管理、清浄な表面、 および明確に定義された検査記録が求められます。.
材料戦略
素材と仕上げの選択肢
小径の場合、切りくずの形状、加工硬化、熱伝導率、 および材料の安定性が、工具寿命や径の制御に直接影響を及ぼします。 仕上げ加工用の余裕は、加工開始前に算入されます。.
ステンレス鋼
継手、バルブ部品、医療用部品、締結部品、および 耐食性シャフトの製造に使用されます。この加工計画により、 加工硬化、長い切りくず、切削熱、および工具の摩耗を抑制します。.
炭素鋼および合金鋼
ピン、伝動軸、ギア軸、ブッシュ、および 高強度ファスナーに採用されています。熱処理による歪みやコーティングの 堆積は、加工代および検査計画に織り込まれています。.
アルミニウム合金
軽量な継手、電子コネクタ、センサー 部品、および計器部品に使用されます。鋭利な工具と清潔な取り扱いにより、 バリの発生や表面の傷を防ぎます。.
真鍮 そして 銅合金
端子、電気接点、流体用継手、およびバルブ 部品に使用されます。グレードの選定にあたっては、導電性、耐食性 、強度、被削性、および鉛含有量の要件を総合的に考慮します。.
POM/アセタール
POMは、シャフト、ブッシング、スペーサー、ローラー、および 精密機械部品の絶縁材として使用されます。機械加工により、切削熱、 変形、およびクランプ圧力を抑制します。.
覗き見
PEEKは、医療機器、半導体システム、および厳しい条件が求められる 産業用アセンブリに用いられています。製造工程では、材料の調整、切削熱、 残留応力、バリの発生が適切に管理されています。.
PTFE, ナイロン そして PMMA
Each plastic follows a separate process. PTFE requires deformation control, nylon requires moisture-aware inspection, and PMMA requires heat, scratch and residual-stress control.
DFM and Cost Control
Convert Critical Features into a Stable Process
DFM review connects each functional requirement to the bar condition, tool access, machining sequence and measurement method needed to hold it in production.
Length-to-Diameter Ratio
Bar straightness, roundness and guide-bushing clearance are treated as process inputs. An unsuitable bar can create taper or runout even when the machine motion is accurate.
Thin Walls
Cutting order, tool sharpness and sub-spindle grip force are balanced to prevent elastic collapse during machining and springback after release.
Small and Deep Holes
Hole depth is reviewed against drill diameter, coolant delivery and chip evacuation. Inspection access is defined before a deep-hole tolerance is accepted.
Cross-Hole Intersections
Breakthrough location and edge requirements determine tool direction and deburring method. Internal burr acceptance must be measurable rather than described only as “burr-free.”
Threads and Runout
Thread standard, class, engagement length, relief and gauge method are linked to the datum diameter controlling assembly runout.
Tolerance Allocation
Tight tolerances are reserved for fits, sealing diameters and locating relationships. Nonfunctional dimensions use an economical general tolerance.
主要コストドライバー
生産管理
Quality from First Article to Final Shipment
Quality control begins with feature-specific measurement planning. First-article results establish offsets and inspection frequency; in-process trends identify tool wear before a critical dimension leaves tolerance.
検査範囲
- Material grade and bar condition
- OD, ID and shoulder locations
- Roundness and coaxiality
- Hole diameter and position
- Thread gauge inspection
- 表面粗さ
- Cross-hole burrs
- Coating and heat-treatment results
Available Documentation
State document requirements during quotation so traceability is built into the production plan.
アプリケーションサポート
Swiss Machining for Critical Industries
Part geometry, material condition, surface requirements and inspection depth are aligned to the actual service environment.
Instrument shafts, holders, guides, threaded components and precision hardware.
Valve components, sensor housings, pins, connectors, bushings and drive parts.
Conductive pins, terminals, contacts, miniature housings and connectors.
Nozzles, valve stems, fittings, adapters, sealing grooves and internal passages.
Locating pins, guide shafts, actuator components, spacers and bushings.
Adjustment components, lightweight sleeves, shafts and precision fasteners.
ウェルドを選ぶ理由
One Factory, One Controlled Route
Weldo coordinates drawing review, material preparation, machining, deburring, finishing, inspection and shipment through one workflow.
- Prototype and repeat production
- Engineering and tolerance review
- Swiss turning and live-tool operations
- Material and finishing coordination
- First-article and in-process inspection
- Production traceability
- Quality-document support
- International order coordination
Buyer Questions
Swiss CNC Machining FAQs
A Swiss machine is a sliding-headstock lathe designed for bar-fed parts. In guide-bushing mode, the bar moves through a bushing while tools work close to the support point, limiting deflection in slender parts. Modern machines also add driven tools and sub-spindles for milled, drilled, threaded and rear-side features.
An automatic feeder supplies bar stock to the main-spindle collet. The sliding headstock moves the bar through the guide bushing while gang-mounted tools cut near the support point. Driven tools add off-axis features, and the sub-spindle receives the part before cutoff to complete rear operations.
Choose it when a part combines a small diameter, slender geometry, multiple features and repeat quantities. Close support controls deflection, while automatic feeding and integrated operations reduce handling. For the right component, that produces stable feature relationships with fewer setups.
The name comes from Switzerland's watchmaking industry, where sliding-headstock automatic lathes were developed for small precision components. Today, “Swiss” describes the machine architecture rather than the country where the machine or part is manufactured.
A conventional lathe holds the workpiece mainly in a chuck or collet and moves tools along the exposed stock. A Swiss lathe moves the bar through a guide bushing and supports it near the cut. Swiss architecture suits slender, small-diameter parts; conventional lathes remain more economical for short, rigid and larger-diameter components.
Yes. Swiss machining is practical for prototypes that need guide-bushing support, driven-tool features or a route intended for later production. A simple one-off part may cost less on a conventional lathe, but using the Swiss route early validates the tooling, datums and cycle planned for repeat orders.
There is no single tolerance for every Swiss-machined part. Diameter, unsupported length, bar quality, material, feature geometry, thermal stability and inspection method affect the result. Weldo confirms critical tolerances after drawing review and verifies them through first-article inspection.
Cross-hole burr control starts with tool direction, edge-break geometry and stable tool condition. Accessible edges are chamfered or mechanically deburred; internal intersections receive an application-specific process. Inspection confirms that loose burrs cannot obstruct flow, interfere with assembly or damage a mating component.