カスタムパワートレイン部品の製造
特注エンジンブロックおよびCNCによるエンジンブロックの加工
ウェルド社は、承認済みの 鋳造品やビレットブランクを用いて、図面に基づいた特注エンジンブロックを製造しています。当社は、試作および量産において、DFMレビュー、多軸CNC 加工、および文書化された検査を組み合わせて実施しています。.
製品の定義
カスタムエンジンブロックとは何ですか?
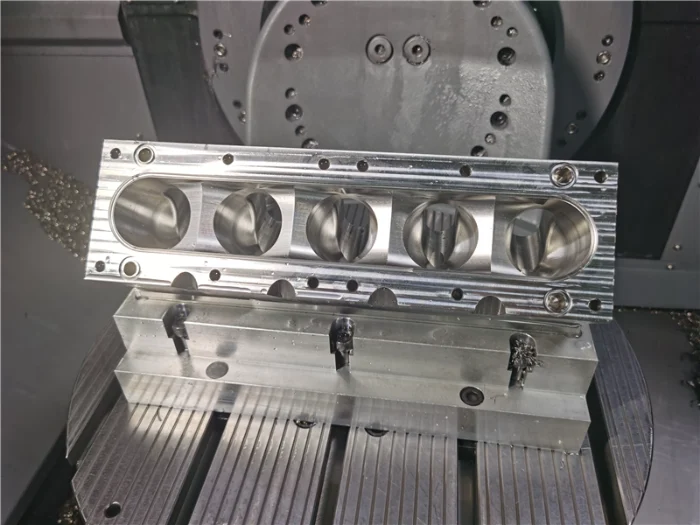
エンジンブロックは、シリンダー、クランクシャフト、メインベアリングを支えるとともに、 潤滑や温度制御に必要なオイル通路や冷却水通路を備えています。 特注ブロックは、標準的なカタログ仕様に基づくものではなく、 顧客が指定した形状に基づいて製造されます。.
カスタム加工が適している場合
新しいパワートレイン、シリンダー間隔の変更、 非標準の取り付け、旧型部品の代替、軽量ビレットコンセプト、 あるいは鋳造金型製作前の設計検証など、用途に合わせて最適なルートをお選びください。.
図面に基づく製造
ウェルド社の機械は、承認された製造データに基づいて製造されます。材料、内径 構造、基準面、公差、清浄度、および検査範囲 については、生産開始前に合意が得られています。.
エンジンの構成
当社が対応するカスタムエンジンブロックの設計
構造設計によって、基準面の設定、アクセス、ワークの固定、および 穴加工の制御要件が決まります。すべてのプロジェクトは、そのプロジェクト固有の 図面と素材の状態に基づいて検討されます。.
直列エンジンブロック
直列シリンダー配置では、シリンダーボア間隔、メインベアリングの 位置合わせ、およびロングデータム管理が一貫して行われる必要があります。直列4気筒および お客様指定の2JZエンジンブロックプロジェクトに適しています。.
V型エンジンブロック
両方のデッキ角度は、クランクシャフトの中心線に対して確実に管理されなければなりません。 適用例としては、カスタムV6、LS3エンジンブロック、およびLS7エンジンブロック のプログラムなどが挙げられます。.
狭角VRブロック
VR6エンジンブロックは、シリンダー間隔が狭い上に、 工具のアクセスが制限されています。ボア、デッキ、および 冷却構造の周辺では、基準面の設定が極めて重要です。.
GT-R パフォーマンス・プロジェクト
お客様からご提供いただいた日産GT-RおよびVR38DETTをベースとした設計については、 ボア形状、デッキ制御、潤滑機能、および ビレット加工の実現可能性について検討が可能です。.
ディーゼルエンジンブロック
ヘビーデューティー用ディーゼルエンジンブロックは、産業用、 移動式機器、発電機用途向けに、ベアリング支持性、材料の 安定性、および耐圧性に優れたデッキ形状を重視しています。.
ビレット&レガシー・ブロック
ビレット加工は、鋳造用金型の作成が現実的ではなく、かつ完全な 製造データが入手可能な場合、試作品、モータースポーツ、および生産終了した 仕様の製造に対応します。.
VR6、2JZ、LS3、LS7、GT-R および関連する名称は、顧客のプロジェクト 事例およびエンジン構成のみを表すものです。ウェルド社は、 OEM公認の交換部品サプライヤーとして紹介されているわけではありません。.
一般的なプロジェクトの参照例
当社が評価可能な車両およびエンジンプラットフォーム
ウェルド社は、特注品、試作品、および 高性能エンジンブロックプロジェクトにおける図面に基づく加工に対応しています。以下に挙げるプラットフォーム名は一般的な 技術上の参照例であり、すべての部品は お客様が承認した仕様に基づいて製造されます。.
フォルクスワーゲン
VR6および関連するコンパクトな多気筒レイアウトでは、ボア間隔、 デッキへのアクセス、および冷却経路の設計において、基準面の計画に細心の注意を払う必要がある。.
BMW
直列4気筒および直列6気筒の開発プロジェクトにおいて、 シリンダーヘッドの表面再加工、ベアリングの位置合わせ、 取り付け方法の見直し、あるいは試作ブロックの 形状設計などが行われている。.
日産
GT-R、VR38、およびRBシリーズの基準アーキテクチャ。顧客が定義する 性能、ビレット、および交換用部品の開発プログラム向け。.
ホンダとホンダ・フィット
Kシリーズ、Lシリーズ、およびホンダ・フィットの改造プロジェクトで、 標準仕様とは異なる取り付け、ボア、デッキ、またはアクセサリーのインターフェースが求められるもの。.
トヨタ&レクサス
2JZ、UZ、GRおよび関連する直列エンジンやV型エンジンのレイアウトを、 性能向上、旧型エンジンの置き換え、試作加工向けに提供しています。.
マツダ
従来のピストンエンジン用ブロックや、特殊なロータリーエンジン用 ハウジングは、それぞれ個別の形状および加工の検討が必要となる。.
素材、性能、仕上げ
カスタムエンジンブロックに使用する材質を選択してください
一般的なグレード、加工上の留意点、表面処理、および実用上のトレードオフを比較してください。出力およびトルクの値は、プロジェクトの参考値であり、材料の保証や完成ブロックの定格値ではありません。.
鋳造用アルミニウム合金
効率的な熱伝達と複雑な鋳造冷却水流路を必要とする、重量に配慮したブロックにとって実用的な選択肢です。.
メリット
軽量で、熱伝導性に優れ、鋳造が安定した後の機械加工が容易である。.
制限事項
鉄に比べて、ボア部の耐摩耗性と剛性が低い。気孔率、デッキの変位、およびライナーの保持力については、慎重な管理が必要である。.
表面処理の選択肢
- 防食用の変換皮膜
- 摩耗しやすい露出部分への選択的ハードアルマイト処理
- 鉄製ライナーまたは特殊な内面コーティングを施した後、ホーニングを行う
代表的なアプリケーション
現代の乗用車、ハイブリッド車、小型トラック、およびアルミニウム製のLS3/LS7型またはVR38型の高性能エンジンレイアウト。.
アルミビレット
鋳造による金型製作が現実的でない場合や、試作、モータースポーツ、少量生産のプロジェクトにおいて、形状設計の自由度を高める必要がある場合に用いられます。.
メリット
鋳造による気孔がなく、設計の自由度が高く、穴の間隔、デッキの高さ、内部形状の修正も容易です。.
制限事項
材料の使用量が多く、加工時間もかかる。7075材については、耐食性、熱サイクル、および穴の構造について個別に検討する必要がある。.
表面処理の選択肢
- 特定の外部部材に対するハードアルマイト処理
- 指定された摩耗箇所または腐食箇所への無電解ニッケルめっき
- 特殊ライナーまたはシリンダー内径用コーティングシステム
代表的なアプリケーション
プロトタイプエンジンやレース用エンジン。カスタム仕様のLS、2JZ、VR6、およびGT-R/VR38をベースとしたアーキテクチャを含む。.
ねずみ鋳鉄
耐久性に優れたガソリンエンジンおよびディーゼルエンジンにおいて、シリンダーボアの安定性、振動の低減、および長寿命を実現する実績のある選択肢です。.
メリット
耐摩耗性、減衰性、寸法安定性に優れ、量産に適した経済的な鋳造品です。.
制限事項
アルミニウム、CGI、またはダクタイル鋳鉄に比べて、質量が大きく、耐食性が低く、引張延性が低い。.
表面処理の選択肢
- 指定された内径表面仕上げのためのプラトーホーニング
- 防錆油を用いたリン酸塩処理
- 外装面へのEコートまたは高温塗装
代表的なアプリケーション
商用ディーゼルエンジン、従来のハイパフォーマンスエンジン、および2JZ型や初期型VR6型のブロックレイアウト。.
黒鉛鋳鉄
シリンダー内圧が高くなる用途向けに選定されており、ねずみ鋳鉄製ブロックの厚さを大幅に増やすことなく、より高い強度と剛性が求められます。.
メリット
ねずみ鋳鉄よりも高い強度、剛性、耐疲労性を有しつつ、有用な減衰性能と熱性能も維持している。.
制限事項
鋳造工程の管理がより厳しくなり、切削抵抗が増大し、工具の摩耗が早まることで、製造コストが増加する。.
表面処理の選択肢
- CBNまたはダイヤモンドを用いたプラトーホーニング
- リン酸塩処理または黒色酸化処理に加え、追加の保護処理を施したもの
- Eコートまたは高温外部塗装
代表的なアプリケーション
高出力のディーゼルピックアップトラック、大型商用車、およびコンパクトで高積載能力を持つパワートレイン。.
ダクタイル鋳鉄
ブロックの重量よりも、靭性、疲労強度、および機械的衝撃に対する耐性がより重要となる場合のための、特殊な選択肢です。.
メリット
高荷重がかかるベアリング部やバルクヘッド部において、高い靭性、耐疲労性、および構造強度を発揮します。.
制限事項
アルミニウムに比べて質量が大きく、熱伝導率も低い。そのため、重量を重視する乗用車プロジェクトではあまり適していない。.
表面処理の選択肢
- 指定された摩耗部位に対する局所高周波焼入れ
- 腐食の影響を受けやすい特定の表面向けの無電解ニッケルめっき
- 外部部分には、リン酸塩処理、Eコート、または工業用塗料が施されています
代表的なアプリケーション
大型ディーゼルエンジン、産業用動力ユニット、および特殊な高負荷レーシングエンジン。.
エンジニアリング・ノート 排気量、出力、トルクは、材料固有の定格値というよりは、設計上の入力パラメータです。最終的な性能は、ブロックの形状、ボアの構造、シリンダーの最大圧力、エンジン回転数、熱負荷、疲労耐久性、および検査要件に基づいて検証する必要があります。.
加工前
材料およびブランクの検証
ブランクは、加工前に図面および材料関連文書と照合されます。目視検査は標準的な手順であり、浸透探傷試験、磁粉探傷試験、超音波探傷試験、または透過放射線検査は、材料、ブランクの形状、および欠陥の発生リスクに応じて選定されます。大型のブランクや歪みに敏感なブランクについては、規定の応力除去処理または時効処理が施されます。. お客様からの書面による承認がない限り、材料の代替は行いません。.
製造工程
特注エンジンブロック向けのCNC加工プロセス
このルートは、安定した基準点、管理された穴の形状、 滑らかな通路、および測定可能な図面要件に基づいて構築されています。.
図面およびDFMレビュー
ブランク、基準面、穴加工体系、流路、公差、および 検査計画を確認する。.
ブランクおよび原点の設定
材料と加工余裕を確認し、安定した 基準面を設定します。.
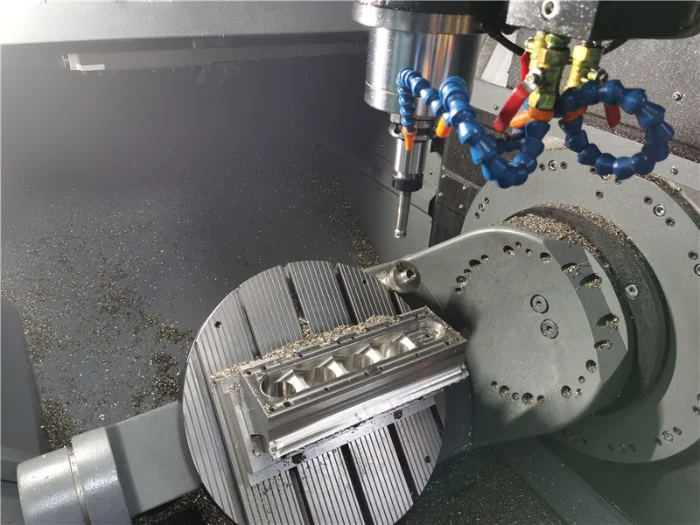
多軸CNCフライス加工
機械加工面、クランクケース面、取付突起、ポケット、および 多面接触面。.
穴あけ・ねじ切り
切削くずの排出を制御しながら、油溝、冷却溝、ダボ穴、ねじ穴などの 形状を加工します。.
精密加工・ラインボーリング
承認された 基準系に対する制御シリンダーおよびメインベアリングの幾何学的形状。.
シリンダー内径ホーニング
リングシステムのボア形状および図面に指定された表面粗さを 仕上げる。.
CNC旋盤加工のサポート
ライナー、スリーブ、ブッシュ、プラグ、およびその他の回転 用付属部品を製造する。.
オプションのワイヤ放電加工
Cut selected conductive through-slots, inserts or profiles that milling cannot reach efficiently.
Deburring & Cleaning
Remove breakout burrs and residual chips from intersecting and blind passages.
最終検査
Verify critical geometry, surface condition, passage integrity and requested records.
Wire EDM is limited to suitable conductive through-features. It does not replace milling, deep-hole drilling, boring or honing for the primary block geometry.
Reference Capacity
Engine Block Machining Capabilities
These are planning references rather than universal engine-block tolerances. Final capability is confirmed after reviewing the drawing, material, feature size, workholding and inspection method.
Usable block size depends on fixtures and access.
Typical noncritical machined features.
Confirmed after material and geometry review.
Finer surfaces require a dedicated finishing route.
Class, depth and sealing form follow the drawing.
Route depends on blank type and validation scope.
Bore requirements remain drawing-specific. Cylinder quality may require diameter, roundness, cylindricity, crosshatch angle and Rk-family surface parameters—not Ra alone.
品質保証
Inspection for Custom Engine Blocks
Inspection is planned around the features that control assembly, sealing, lubrication and long-term stability.
材料の検証
Check certificates, traceability, blank dimensions and the specified nondestructive-test records.
寸法管理
Verify decks, bore positions, bearing geometry and datum relationships during and after machining.
Bore Surface Control
Assess diameter, form and specified texture using equipment matched to the drawing requirement.
Passage & Leakage Checks
Inspect continuity, burrs and contamination. Pressure or leakage testing can be coordinated when specified.
ウェルドを選ぶ理由
A Practical Route From Drawing to Inspected Part
Weldo focuses on manufacturing feasibility, stable process planning and clear inspection requirements. Specialized honing, coating, CT inspection or pressure testing can be coordinated through an approved route when the project requires them.
Explore prototype CNC machining →Engineering FAQ
Custom Engine Block Questions
Short answers for sourcing, manufacturing and repair-related decisions.
Can Weldo machine an engine block from my drawing? +
Yes. Weldo supports drawing-based machining of customer-supplied castings, billet stock and approved blanks. Feasibility is confirmed from the material, dimensions, datums, tolerances and inspection requirements.
What information is required for a quotation? +
Provide the 2D drawing or 3D model, blank condition, material, quantity, critical tolerances and finishing requirements. Identify the cylinder bores, main-bearing bores, deck surfaces and critical passages.
How do I know if my engine block is bad? +
Warning signs include repeated overheating, coolant or oil leakage, mixed oil and coolant, white exhaust smoke, low compression and abnormal noise. Similar symptoms can come from the head or gasket, so testing is required before confirming block damage.
Can an engine block be repaired? +
Some blocks can be restored by boring, honing, deck resurfacing or an approved repair liner. Severe bulkhead cracks, main-bearing damage, extensive distortion or major structural breakage usually make replacement safer.
How long will an engine block last? +
There is no fixed lifespan. A properly manufactured and maintained block can last for the service life of the engine. Overheating, poor lubrication, corrosion, detonation, contamination and incorrect assembly shorten its life.
How expensive is it to fix an engine block? +
Cost depends on damage, engine design and required operations. Honing or resurfacing costs less than installing liners, repairing cracks, rebuilding the rotating assembly or replacing the engine. Inspection is required before a reliable quotation.
What is the strongest material for an engine block? +
There is no single best material. CGI and ductile iron provide high strength and stiffness; gray iron offers wear resistance and damping; reinforced aluminum provides a better strength-to-weight ratio. Selection depends on pressure, temperature, weight, bore design and cost.
Engineering Review & Quote
Start Your Custom Engine Block Project
Send your drawing or model with the blank condition, material, quantity, bore requirements, tolerances and inspection specifications. We will review manufacturability and prepare an appropriate machining route.