
Weldo Machining · Custom Parts
Custom Connecting Rods
Precision-machined to your drawings, material requirements and assembly specifications. Get a manufacturing review, a clear quotation and a project-specific delivery plan.
お見積りのご依頼 →01 / Rod Designs
Custom Connecting Rods for Your Application
Choose the geometry your assembly needs. Cross-section, end design and loading must be considered together—not by beam name alone.
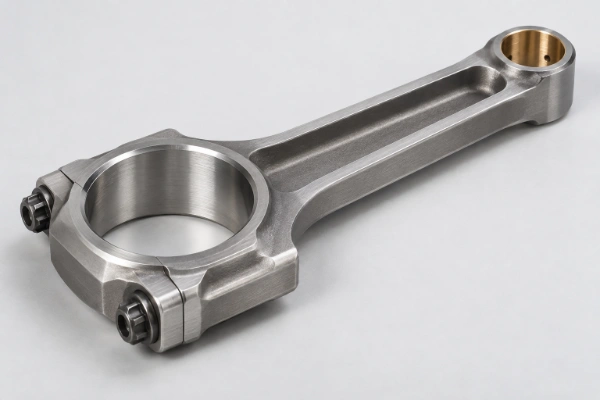
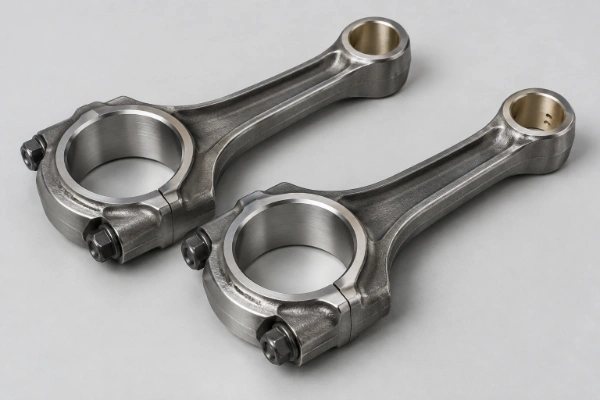
Steel Connecting Rods
Drawing-defined rods with machined big-end housings, small-end bores and matched caps for engine, pump and compressor designs.
- I-beam and H-beam sections: follow the approved drawing; the beam label alone does not establish load capacity.
- Functional geometry: fillets, cap joints, bolt seats and lubrication features are reviewed around the assembly requirements.
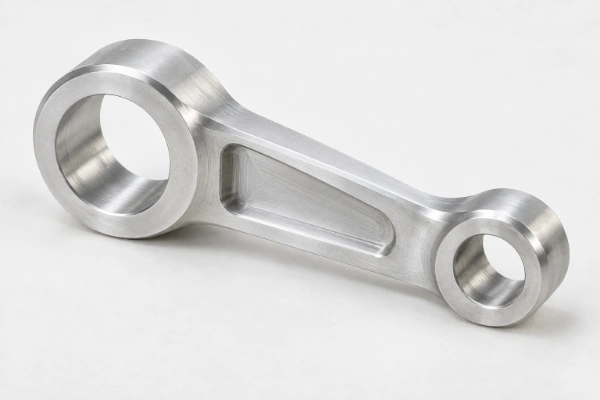
Custom-Profile Industrial Links
One-piece links with specified offsets, pockets and bore geometry for automation, instruments and industrial mechanisms.
- Material and geometry: machine from the specified metal or engineering plastic to match the load and mating parts.
- Application limits: light-load aluminum or POM links are not drop-in replacements for engine connecting rods.
One-piece or split-end construction: specified independently of the beam profile. Split big ends are manufactured and inspected with their matched caps.
02 / Material Selection
Materials Matched to the Working Load
Specify the grade and supplied condition. Material substitutions require approval before production.
アルミニウム合金
6061 · 7075Lightweight options for machinery linkages, prototypes and drawing-defined connecting rods. Grade and temper are selected around load, temperature and fatigue requirements.
- Performance
- 6061 suits many light-duty links; 7075 in an appropriate temper provides higher strength for demanding designs. Neither is a same-size substitute for steel.
- 仕上げ
- Deburring and selective anodizing, with dimensional allowances and masking defined for fits and threads. Review coating effects on fatigue-critical surfaces.
- アプリケーション
- Automation links, lightweight mechanisms and validated custom rod designs.
チタン合金
Ti-6Al-4VHigh specific strength for weight-sensitive connecting rods. Material condition, contact design and fatigue requirements are defined before machining.
- Performance
- Low density relative to steel, with careful control of cutting heat, tool wear and surface integrity.
- 仕上げ
- Precision deburring and drawing-approved anti-galling treatments where sliding or threaded contacts require protection.
- アプリケーション
- Weight-critical mechanisms and engineering-validated performance assemblies.
Alloy Steels
4140 · 4340Strength and toughness for highly loaded rods and industrial mechanisms. Billet or forged blanks are selected with the specified heat-treatment route.
- Performance
- Heat treatment and final machining are coordinated to control hardness, distortion and fatigue-critical geometry.
- 仕上げ
- Grinding or honing where specified; controlled shot peening and corrosion protection only on approved areas.
- アプリケーション
- Engine designs, pumps, compressors and heavy-duty transmission linkages.
POM
POM-C · POM-HLow-friction engineering plastic for light-load links and functional prototypes. POM is not a replacement for metal engine connecting rods.
- Performance
- Good machinability and low moisture uptake. Creep, bearing pressure and operating temperature govern selection.
- 仕上げ
- Deburring, cleaning and dimensional stabilization as required; no metal-style heat hardening.
- アプリケーション
- Instruments, automation mechanisms and non-combustion motion prototypes.
Need a different material?
Share your specified alloy or polymer, operating temperature and load conditions. We will review stock availability and process compatibility.
03 / Machining Capabilities
Clear Specifications. Measurable Results.
General tolerances define the baseline. Functional bores, center distance and axis relationships receive individual drawing requirements.
| Control Item | Specification Basis | Scope & Conditions |
|---|---|---|
| Machining processes | 3-, 4- and 5-axis CNC machining | Route selected for geometry, access and production quantity. |
| General dimensional tolerances | ISO 2768-1, agreed class such as m | For dimensions without individual tolerances; not a substitute for functional limits. |
| Bore sizes & fits | Drawing limits or ISO 286 tolerance classes | Big-end housing, bush fits and pin bores are specified separately. |
| Geometrical tolerances | ISO 1101 drawing requirements | Specify form tolerances and datum references where required for axis relationships. |
| Center distance & end widths | Individually toleranced | Controlled from the drawing’s functional datum scheme. |
| Machined surface finish | Ra 0.8–3.2 μm, typical machined surfaces | Not a bearing-bore acceptance limit. Functional surfaces follow the drawing. |
| Part envelope | Confirmed at drawing review | Overall length, end sizes, tool access and fixturing determine feasibility. |
| Final inspection state | Finished and specified assembly condition | Matched cap and specified preload; bush bores checked in the agreed installed state. |
Assembly state matters: inspect a split big-end housing bore with its matched cap and specified bolt preload. Housing-bore size and bearing running clearance are separate requirements.
04 / Manufacturing Route
From Blank to Finished Connecting Rod
Weldo provides CNC加工 and coordinates specified finishing and inspection around the final assembly requirements.
Blank & Process Review
Select billet or a sourced forged blank to match the drawing, quantity and material condition. Confirm stock allowances, grain-flow requirements and responsibilities before production.
Rough & Semi-Finish Machining
Machine the beam, ends, holes and threads using stable support and controlled datum transfers. Preserve specified fillets and load-bearing sections.
Heat Treatment & Finishing
Sequence required heat treatment, final boring, grinding or honing to manage distortion. Confirm specialist operations and selective surface treatments in the quotation.
Final Verification & Delivery
Inspect in the specified assembly state, clean oil passages and threads, preserve matched sets and provide the agreed inspection and traceability records.
05 / Quality Control
Inspect the Features That Govern Fit
Verification follows the approved drawing, inspection plan and material condition—not appearance alone.
Material & Traceability
Retain specified material and heat-treatment records. Verify hardness and apply drawing-required crack detection using methods suitable for the material.
Bores, Bend & Twist
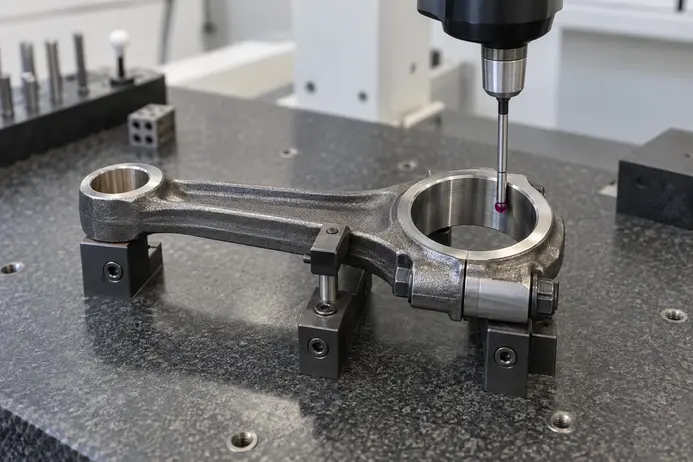
Check bore size, form, center distance and axis relationships using suitable gauges, fixtures or CMM methods. Inspect installed bushings and preloaded caps in the specified state.
Total & End-Weight Matching
Use one defined weighing setup and attachment condition. Adjust only approved balance areas; rod matching does not replace complete rotating-assembly balancing.
06 / Delivery & Cost
A Clear Plan for Your Production Schedule
Weldo operates its own machining factory and offers one-stop coordination of machining, specified treatments and inspection.
Typical Dispatch
For eligible stock-material projects after drawing approval and order confirmation. Batch schedules are agreed separately.
Custom forgings, heat treatment, specialist finishing and validation add time. The quotation defines the start conditions and shipment date.
Control Cost Without Compromising Fit
Prioritize functional tolerances.
Apply tight controls to bores, center distance and critical surfaces—not every external feature.
Match the blank to the quantity.
Compare billet and forged-blank routes using machining time, tooling and lead time together.
Approve a first article.
Confirm fit and inspection results before repeating the process across a production batch.
プロジェクトを始めましょう
Turn Your Connecting Rod Drawing into a Manufacturing Plan.
Send your drawing or sample details, material, application, quantity and target delivery date. We will confirm feasibility, scope and quotation.
The quotation identifies whether caps, bolts, bushings and bearing shells are included.
07 / Common Questions
Custom Connecting Rod FAQs
Practical answers on reuse, assembly and manufacturing validation.
Can you reuse or recondition connecting rods?
Reuse depends on the original manufacturer’s limits, service history and inspection results. Check cracks, heat damage, bend, twist, bores and bolts. Only approved designs should be reconditioned; cracked, severely overheated or out-of-limit rods should be replaced. Dimensional conformity alone does not establish remaining fatigue life.
Can connecting rod caps be interchanged?
Do not interchange matched rods and caps, even when their nominal dimensions are identical. Pair identification, orientation and specified bolt preload affect big-end size and roundness. Fracture-split rods must retain their original mating cap; damaged or mismatched parts require assessment before assembly.
What should be checked before installing connecting rods?
Confirm crankpin and bearing sizes, running clearance, side clearance, orientation and clearance to the crankshaft fillet. Use the specified bolt lubricant and tightening method, not a generic torque value. Agree these assembly conditions before manufacturing a custom replacement.
Can custom connecting rods be made from an existing sample?
A sample can support reverse engineering, but worn or distorted dimensions must not become production targets. Confirm center distance, bores, widths, material and heat treatment against mating parts or design data. High-cycle applications also require defined loads and validation, not simply a copy of the shape.
What determines a connecting rod’s horsepower and RPM rating?
Material grade or an H-beam or I-beam profile alone does not establish a rating. Reciprocating mass, stroke, combustion pressure, cross-section, bolt preload and intended life must be assessed together and validated. A dimensional inspection report is not an engine durability certification.