
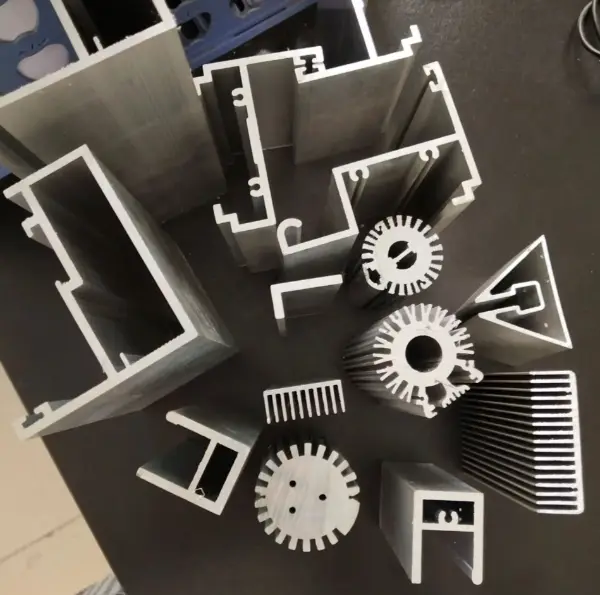
Custom Aluminum Extrusion Services
Turn a profile drawing into finished aluminum components with coordinated die development, alloy and temper selection, cutting, surface finishing, and inspection.
- Solid & Hollow Profiles
- Alloy & Temper Review
- Machining & Finishing
From Heated Billet to Finished Profile
Extrusion forms a continuous cross-section through a shaped die. Cooling, straightening, temper development, and downstream work follow the chosen alloy and production route.
Billet Preparation
Cut and heat the selected alloy billet for controlled flow through the die.
Die Extrusion
Form the approved solid, semi-hollow, or hollow cross-section.
Controlled Cooling
Match cooling or quenching to the alloy, section, and required temper.
Straightening
Stretch and straighten suitable profiles to control bow, twist, and distortion.
Temper Development
Apply alloy-appropriate conditioning; age heat-treatable grades when specified.
Secondary Operations
Cut, machine, finish, and inspect the profile to the approved drawing.
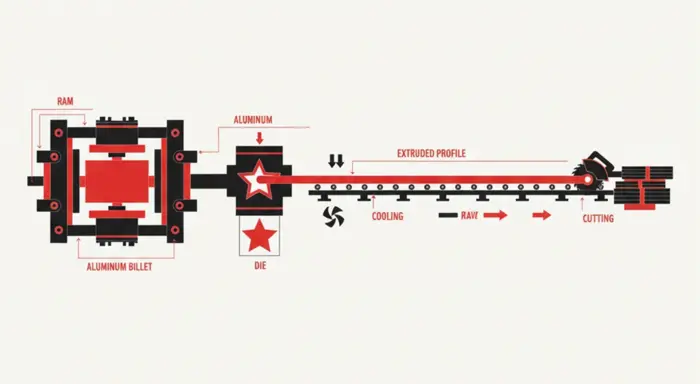
Direct Extrusion
The ram pushes the billet through a stationary die. This widely used route supports many custom solid and hollow profile geometries.
Indirect Extrusion
A die advances into the billet with reduced billet-to-container sliding friction. Suitability depends on the profile and available press setup.
Aluminum Extrusion Alloys
Choose alloy and temper together. Balance strength, profile complexity, surface appearance, conductivity, fabrication, and the service environment.
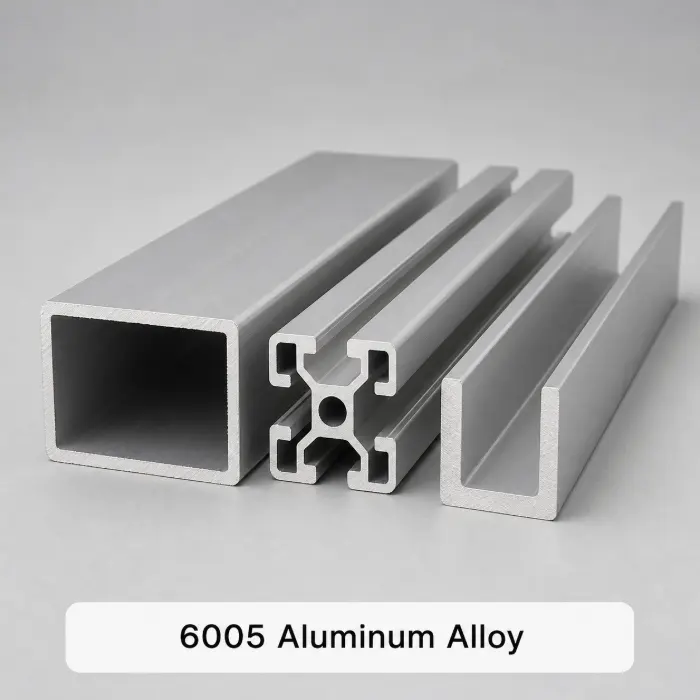
6005 Aluminum
A medium-strength structural alloy with useful corrosion resistance and extrusion performance for industrial profiles.
View alloy details
- Typical applications
- Machine frames, ladders, platforms, structural rails, supports, and modular systems.
- Temper and fabrication
- Confirm the exact 6005 specification and temper; 6005A is a separate designation and should not be substituted without agreement.
- Finish considerations
- Anodizing, powder coating, conversion coating, or other specified finishes, subject to appearance and fit requirements.
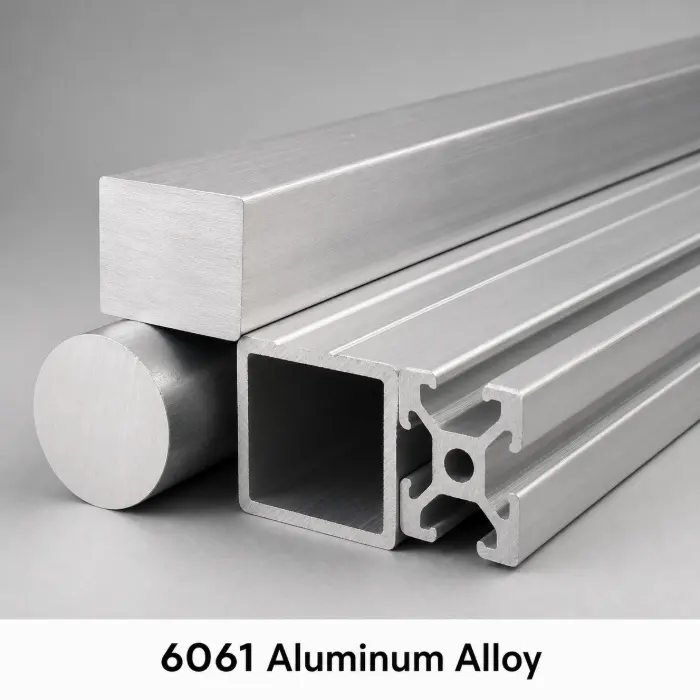
6061 Aluminum
A versatile heat-treatable alloy balancing structural strength, corrosion resistance, and secondary machinability.
View alloy details
- Typical applications
- Machine frames, equipment rails, mounting profiles, structural housings, and CNC-finished components.
- Temper and fabrication
- Commonly selected where strength and post-extrusion machining matter. Confirm temper, welded-joint requirements, and section feasibility.
- Finish considerations
- Anodizing, hard anodizing, conversion coating, painting, and powder coating, with allowances for functional fits.
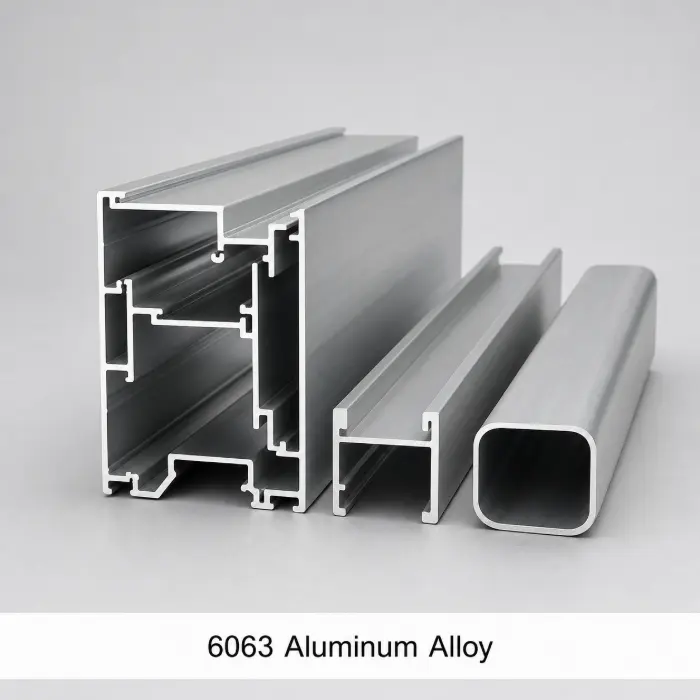
6063 Aluminum
An extrusion-focused alloy with good surface quality and decorative anodizing potential for detailed profiles.
View alloy details
- Typical applications
- Window and door profiles, trim, LED channels, heat sinks, display frames, and decorative enclosures.
- Temper and fabrication
- Selected for extrudability, appearance, and useful profile complexity rather than maximum structural strength.
- Finish considerations
- Decorative anodizing, electrophoretic coating, powder coating, PVDF coating, polishing, or brushing after review.
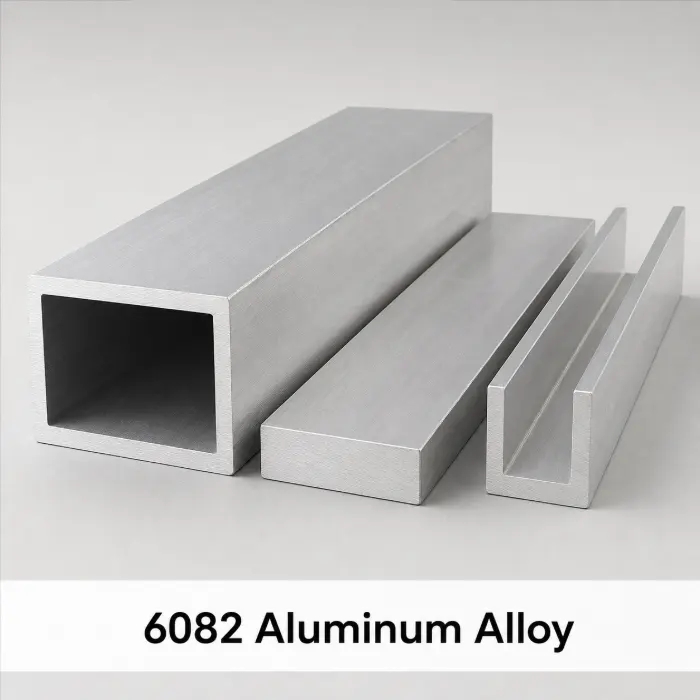
6082 Aluminum
A higher-strength 6xxx structural alloy with useful corrosion resistance, weldability, and machinability.
View alloy details
- Typical applications
- Load-bearing frames, transport structures, heavy supports, rails, and machined profiles.
- Temper and fabrication
- Extrusion complexity is generally more restrictive than 6063. Review wall balance, temper, machining, and welded joints.
- Finish considerations
- Protective anodizing, conversion coating, powder or PVDF coating; decorative appearance requires qualification.
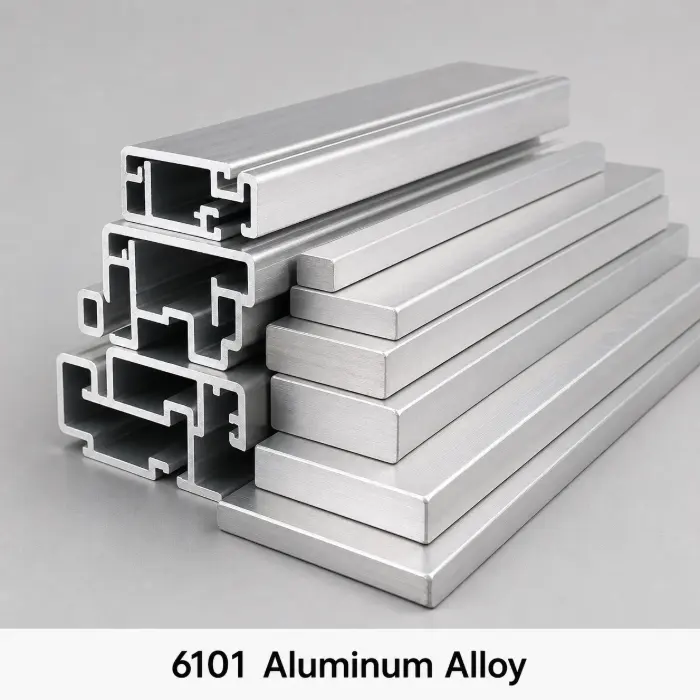
6101 Aluminum
A heat-treatable electrical alloy offering high conductivity with moderate structural strength.
View alloy details
- Typical applications
- Busbars, conductor rails, switchgear components, electrical connectors, and power-distribution profiles.
- Temper and fabrication
- Specify the conductivity and strength requirements together; the temper affects electrical, mechanical, and forming behavior.
- Finish considerations
- Mill finish or specified tin, nickel, or silver plating. Define conductive contact surfaces and mask them from insulating finishes.
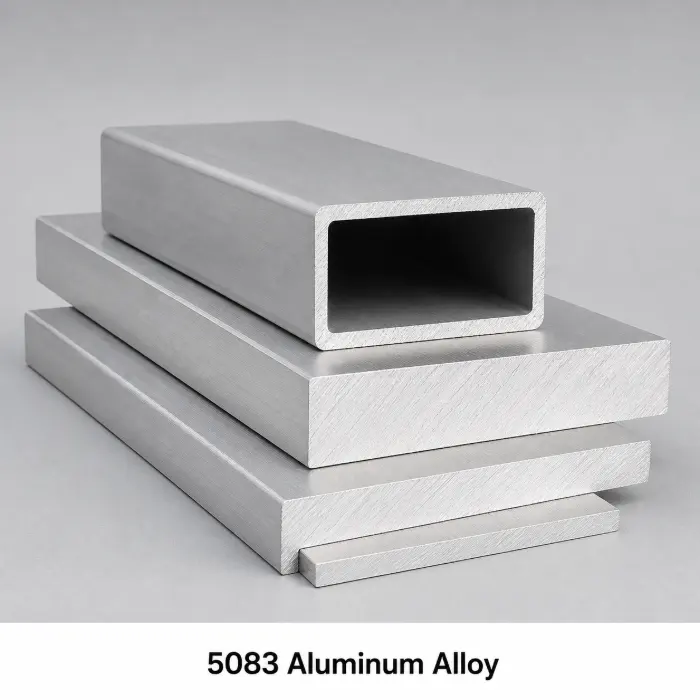
5083 Aluminum
A non-heat-treatable 5xxx alloy valued for marine corrosion resistance, weldability, and low-temperature toughness.
View alloy details
- Typical applications
- Marine rails, welded supports, deck structures, corrosion-resistant frames, and reviewed chemical or cryogenic applications.
- Temper and fabrication
- Section geometry and supplied condition require separate review. Do not specify T4, T5, or T6 as a general strengthening route for 5083.
- Finish considerations
- Mill finish, mechanical preparation, conversion coating, or protective coatings; qualify anodizing appearance and service suitability.
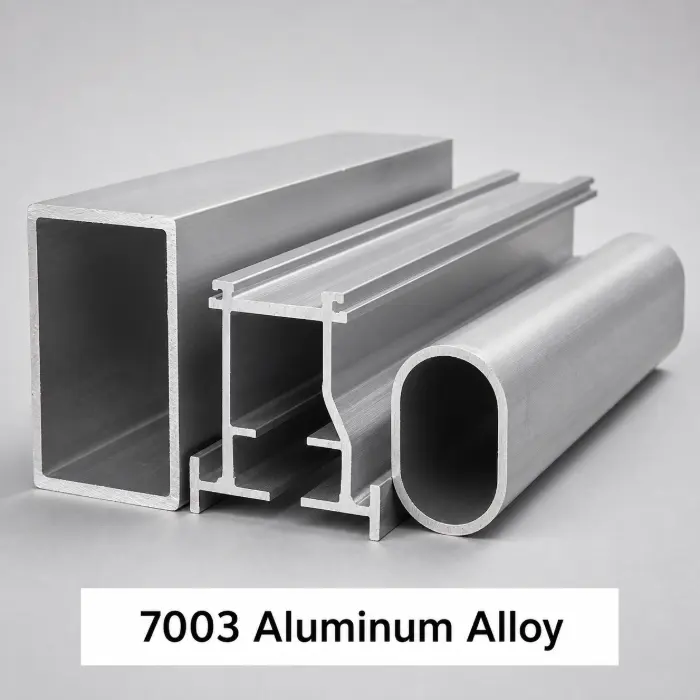
7003 Aluminum
A high-strength Al-Zn-Mg extrusion alloy for selected transport and lightweight structural applications.
View alloy details
- Typical applications
- Vehicle reinforcement profiles, structural rails, bicycle components, and reviewed welded assemblies.
- Temper and fabrication
- Confirm temper, welded-joint performance, corrosion exposure, and fatigue or crash requirements through the design and validation plan.
- Finish considerations
- Protective anodizing, conversion coating, or specified coatings; stressed regions and joints need corrosion-aware review.
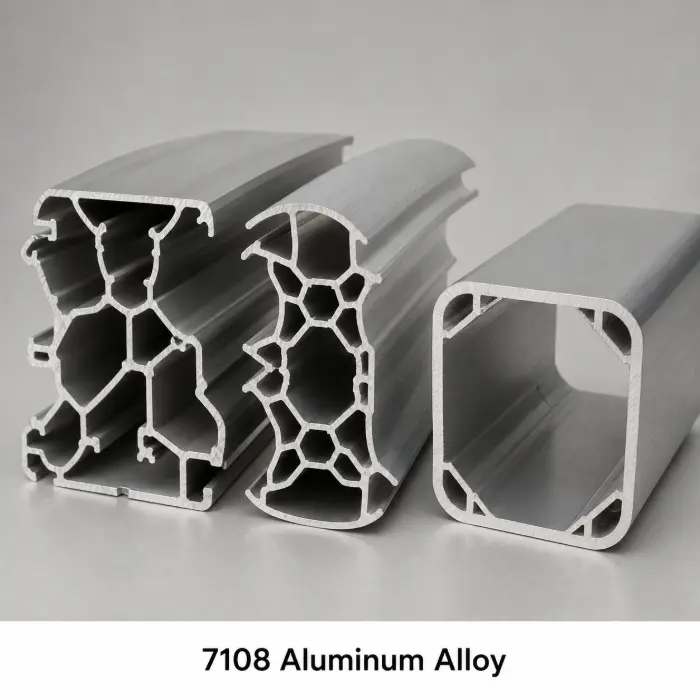
7108 Aluminum
A high-strength structural extrusion alloy with more restrictive profile geometry and forming requirements than common 6xxx grades.
View alloy details
- Typical applications
- Load-bearing frames, supports, transport profiles, and weight-sensitive structural components.
- Temper and fabrication
- Review section feasibility, temper, forming, and welding. Critical welded or highly stressed regions require project-specific validation.
- Finish considerations
- Protective anodizing or specified coatings, with corrosion requirements and appearance agreed for the selected condition.
Availability, supplied condition, mechanical properties, weld requirements, and surface appearance are confirmed for the exact alloy and profile. T4, T5, and T6 are not applicable to every alloy family.
Aluminum Extrusion Capabilities
Review the full cross-section, alloy, temper, required cut length, tolerances, and downstream operations together.
Drawing-Based References
| Profile classes | Solid, semi-hollow, and hollow sections, subject to die and press review. |
|---|---|
| Profile-width reference | Up to 1100 mm*Confirm section shape, circumscribing circle, alloy, press, die, and handling requirements. |
| Minimum-wall reference | From about 0.8 mm*Depends on alloy, section size, unsupported features, geometry, and required tolerances. |
| Dimensions and geometry | Drawing-defined dimensions, straightness, twist, and flatness using the agreed extrusion standard. |
| Tolerance basis | ANSI H35.2, EN 755-9, or another agreed standard within its applicable scope. Confirm the required edition and any tighter critical features. |
| Temper options | T4, T5, T6, and other conditions where applicable to the selected alloy and manufacturing route. |
| Delivered length | Project-specific cut lengths, reviewed against extrusion runout, straightening, aging, handling, and shipping. |
Coordinated Downstream Work
Precision Cutting
Specify delivered length, end condition, cut tolerance, deburring, and protection of functional faces.
CNC Machining
Review drilling, milling, tapping, pockets, mounting details, and critical interfaces against extrusion datums.
Fabrication and Finishing
Coordinate specified welding, assembly, and surface treatment with alloy condition, distortion, masking, and final fits.
Inspection and Records
Check section dimensions, delivered length, geometry, machined features, and finish requirements with agreed documentation.
*Quotation references, not universal limits. Maximum width and minimum wall are reviewed separately and should not be assumed achievable together. Capability depends on the full profile, die, press, alloy, and production route.
Design Profiles for Stable Extrusion
Early section review helps reduce die revisions, distortion, unnecessary mass, and repeated secondary machining.
Balanced Walls
Keep adjacent wall sections reasonably consistent to support uniform flow, cooling, and dimensional stability.
Generous Radii
Use suitable internal and external radii to improve metal flow and reduce severe local demands on the die.
Balanced Geometry
Use symmetrical or balanced sections where practical to manage bow, twist, and uneven cooling.
Supported Thin Features
Review long fins, deep narrow channels, and die tongues against flow, strength, cooling, and handling limits.
Machining Allowance
Leave stock where critical faces, bores, slots, or interfaces need post-extrusion machining.
Finish Allowance
Define coating buildup, visible surfaces, masking, rack contacts, and the final condition of functional fits.
Surface Finishes for Aluminum Profiles
Select the finish by appearance, corrosion exposure, wear, conductivity, and the required final dimensions.
Mill Finish & Preparation
Retain the as-extruded condition or specify deburring, brushing, polishing, or blasting for reviewed surfaces.
Anodizing
Protective, decorative, or hard anodizing as suitable for the alloy, appearance target, wear, and final dimensions.
MAO / Ceramic Coating
Micro-arc oxidation for selected applications requiring an oxide-based ceramic layer; review roughness, thickness, and fit.
Electrophoretic Coating
A reviewed decorative or protective organic coating system, with pretreatment, film thickness, and masking defined.
Powder Coating
Colored coating for suitable architectural and industrial profiles, with functional areas masked and cure compatibility confirmed.
PVDF Coating
Specified exterior coating systems for weathering and color-retention requirements, subject to pretreatment and coating specification.
Where Custom Profiles Add Value
Integrate channels, mounting details, and reinforcement into a purpose-designed section to reduce repeated machining and assembly work.
Automation
Machine frames, guards, linear modules, and assembly structures.
Transportation
Lightweight rails, frames, supports, and reviewed body structures.
Electronics & Thermal
Heat sinks, LED channels, housings, and equipment enclosures.
Architecture
Window, door, façade, trim, and profile systems.
Renewable Energy
Solar mounting, battery enclosures, and energy-system frames.
Furniture & Fixtures
Modular frames, tracks, display systems, and decorative profiles.
Custom Extrusion Questions
Should I choose 6061 or 6063?
6061 is often selected for structural requirements and secondary machining. 6063 is often preferred for extrudability, detailed profiles, and visible anodized appearance. The final choice also depends on temper, geometry, load, and finish.
Does a custom profile need a new die?
A new cross-section normally needs a dedicated die. Cost depends on section size, solid or hollow construction, die complexity, expected production, and correction requirements. Existing tooling can be reviewed where applicable.
When does custom extrusion become economical?
It is attractive when a repeated cross-section removes substantial machining, joining, or assembly work. Compare die cost, material yield, run quantity, finishing, and the complete delivered-part route.
How are thin walls and distortion controlled?
Review wall balance, radii, supported features, die design, alloy, cooling, stretching, and handling. Define acceptable straightness, twist, and flatness on the drawing instead of relying on a single general size tolerance.
What determines practical profile length?
Press runout, cooling, straightening, temper development, handling, shipping, and final cutting determine the usable length. State the delivered cut length and end requirements in the quotation package.
Can the extrusion be machined and finished afterward?
Yes, subject to review of datums, machining allowance, alloy condition, workholding, and finish sequence. Identify critical machined features, coating allowances, and surfaces requiring masking.