When you choose materials for defense equipment parts, assess the deployment location, mechanical loads, and protection requirements together. Because climates vary widely across the United States, the Middle East, and Europe, use geography as an initial screening guide and select the final material and surface finish based on the actual operating environment and project specifications.
What Conditions Should Be Confirmed Before Selecting a Material?
Before evaluating materials, confirm the part’s operating environment and functional requirements:
- Environment: Operating temperature, humidity, salt spray, dust, condensation, and thermal cycling.
- Media: Seawater, cleaning agents, fuel, lubricants, or other chemicals.
- Loads: Impact, vibration, fatigue, sliding friction, and abrasive wear.
- Function: Weight, strength, corrosion resistance, electrical conductivity or insulation, thermal conductivity, and maintenance requirements.
- Acceptance: Material condition, surface finish, critical dimensions, inspection items, and required documentation.
Corrosion behavior depends on more than the material grade. Temperature, chloride concentration, deposits, liquid accumulation, and crevices also matter. For example, stainless steel can still experience pitting or crevice corrosion in chloride-containing environments.
How Do the Climates in the United States, the Middle East, and Europe Affect Material Selection?
| Region and typical environment | Material-selection priorities | Surface-finish priorities |
|---|---|---|
| United States: humid, saline coastal areas; hot, dusty Southwest; cold northern areas with possible de-icing salt exposure | Evaluate corrosion resistance for coastal areas; heat resistance, wear resistance, and sealing for desert environments; and low-temperature toughness for northern areas | Specify coating coverage and low-temperature suitability; protect sliding surfaces and sealing areas in dusty environments |
| Middle East: high temperatures, dust, and large day-to-night temperature swings inland; high temperatures, humidity, and salt along the Gulf coast | Evaluate thermal stability, wear, and dust sealing inland; assess humidity and salt exposure together along the coast | Focus on wear resistance and dust protection inland; strengthen corrosion protection along the coast and specify coverage on cut edges, holes, and joints |
| Europe: cold, damp northern areas; rainy western areas; hot southern areas, some of them coastal | Evaluate low temperature, moisture, salt, and thermal cycling according to the specific location | Consider freeze-thaw and corrosion protection in the north; assess salt-spray and weather resistance in the south; minimize water-trapping crevices |
The United States spans humid coastal areas, deserts, and cold regions. Europe includes northern, temperate, and Mediterranean climates, while the Middle East also has significant differences between inland and coastal areas.
Which Materials Are Suitable for CNC-Machined Defense Equipment Parts?
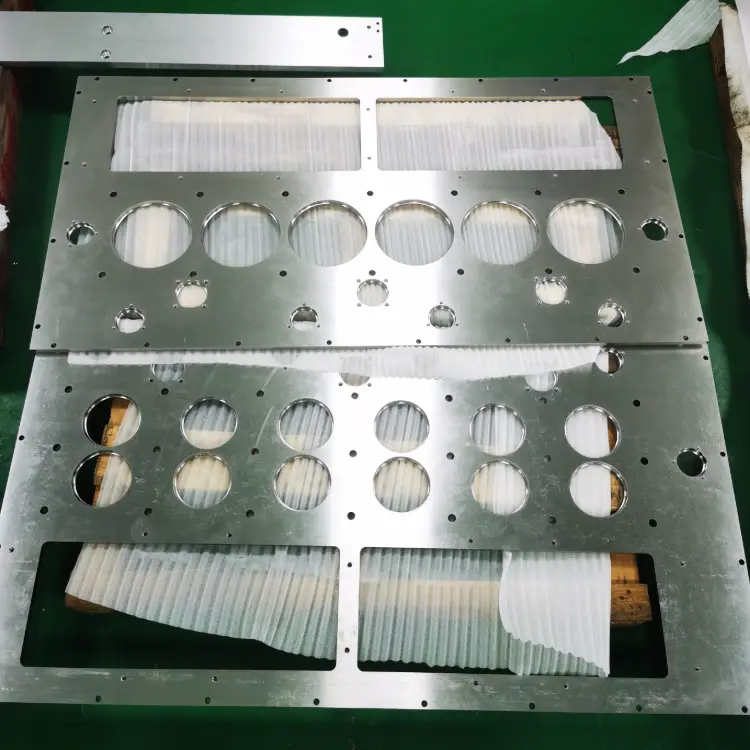
| Material category | Common parts and primary applications |
|---|---|
| 6061 | Housings, brackets, panels, and mounting plates requiring a balanced combination of properties |
| 7075 | Load-bearing structural parts that require high specific strength and low weight |
| Stainless steel | Corrosion-resistant fittings, housings, and fastening structures |
| 17-4PH | Shafts, valve components, and connectors requiring high strength and hardness |
| Carbon and alloy steels | Bases, pins, sleeves, and transmission components subject to high loads, impact, or wear |
| Titanium alloy | Lightweight connectors and structural components requiring high specific strength and corrosion resistance |
| Copper alloys | Electrically or thermally conductive parts and sliding-contact components |
| Engineering plastics | Insulating supports, guides, sleeves, and lightly loaded sliding parts |
Aluminum Alloys: Select by Strength, Environment, and Temper
6061 is suitable for parts requiring a balanced combination of machinability, corrosion resistance, and structural performance. 7075 is suitable for structures where strength and low weight are priorities. For humid, salt-spray, or long-term outdoor service, also evaluate the material temper, protection method, and joint design. Aluminum-alloy properties vary with grade, temper, and product form.
Stainless Steel and 17-4PH: Specify the Media and Heat-Treatment Condition
The 304 and 316 series are used for fittings, housings, and fastening structures. In chloride-containing environments, 316 is generally more suitable than 304, but temperature, chloride concentration, deposits, and crevices also affect actual corrosion performance. Seawater or high-temperature, high-salt service requires evaluation against the specific operating conditions.
17-4PH is suitable for shafts, valve components, and connectors requiring high strength and hardness. The drawing should specify the final aging condition because it affects mechanical properties and machining requirements.
Carbon and Alloy Steels: Coordinate Heat Treatment and Corrosion Protection
Carbon steel can be used for bases, connection plates, and brackets when effective protection is provided. Alloy steels such as 4140 are used for pins, sleeves, and transmission components subject to high loads, impact, or wear. For outdoor, coastal, or moisture-exposed service, evaluate the heat-treatment condition and corrosion-protection system together.
Titanium Alloys: Structural Parts with High Strength-to-Weight and Corrosion-Resistance Requirements
Ti-6Al-4V (Grade 5) can be used for connectors, supports, and structural parts that are weight-constrained and require high specific strength and corrosion resistance. Titanium alloy material and machining costs are higher, so it is best selected when the design has a clear weight or corrosion-resistance requirement. Property data should correspond to the specific material condition and product form.
Copper Alloys: Conductive, Thermal, and Sliding-Contact Parts
Copper alloys can be used for electrical terminals, conductive contacts, bushings, and sliding parts. For conductive connectors, verify conductivity and contact requirements. For load-bearing or wear-resistant bushings, evaluate strength, wear resistance, and fit. In damp or corrosive environments, confirm that the surface finish is compatible with the service media.
Engineering Plastics: Insulating, Low-Friction, and Media-Resistant Parts
Engineering plastics can be used for insulating supports, guides, sleeves, and lightly loaded sliding parts. Select by specific grade and check operating temperature, chemical compatibility, creep, and dimensional stability. For outdoor use, also verify resistance to ultraviolet exposure and thermal cycling.
How Should Surface Finishes Be Selected for the Material and Environment?
| Substrate and requirement | Possible finish options | Key controls |
|---|---|---|
| Aluminum alloy requiring wear resistance or a decorative finish | Anodizing; consider hard anodizing for high-wear applications | Specify coating thickness, sealing, and fit dimensions; the coating affects final dimensions |
| Aluminum alloy requiring corrosion protection while retaining electrical contact | Chemical conversion coating | Specify the applicable standard, class, and contact areas; MIL-DTL-5541 covers chemical conversion coatings on aluminum and aluminum alloys. Follow the drawing and contract for specific requirements. |
| Stainless steel requiring a clean surface and passivation | Passivation | Specify surface cleanliness and acceptance requirements; passivation is not a thick wear-resistant coating |
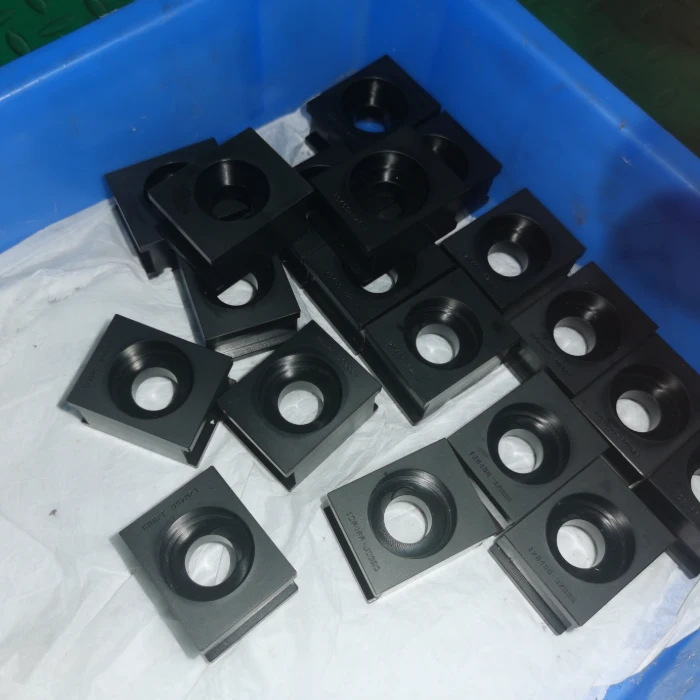
| Carbon or alloy steel requiring rust protection | Black oxide, plating, or a paint system | Black oxide is generally used with oil or a sealer; evaluate a complete protection system for outdoor and coastal service |
| Steel requiring wear resistance or dimensional restoration | Heat treatment, plating, or an engineered coating | Confirm substrate hardness, coating thickness, subsequent finish machining, and hydrogen-relief requirements for high-strength steel |
| Copper alloy requiring conductivity or tarnish protection | Plating or protective treatment selected for the contact function | Specify conductivity, solderability, thickness, and masking requirements |
| Engineering plastic requiring a cosmetic finish or surface texture | Blasting, painting, or a validated process | Confirm material compatibility, coating adhesion, and service temperature |
Pay particular attention to the following:
- In coastal or salt-spray environments, include cut edges, holes, threads, and joints in the corrosion-protection plan.
- For aluminum parts requiring grounding, identify electrical-contact areas separately. Anodizing forms an electrically insulating oxide film; chemical conversion coatings can be used for specified corrosion-protection and electrical applications.
- Anodic coating thickness affects dimensions. Specify final dimensions and masking requirements for mating surfaces, holes, and threads. AAC anodizing FAQ
- When electroplating high-strength steel, confirm applicable hydrogen-relief requirements during the process review.
How Should the Machining Sequence Account for the Material and Coating?
For precision parts, determine the material condition and surface finish before planning the machining datum and stock allowance. Thin-walled, deep-pocketed, or asymmetric parts may require staged rough machining, stress relief, and finish machining. For heat-treated parts, recheck critical dimensions after heat treatment and finish-machine as needed.
Specify the final dimensions and treatment areas for bearing seats, threads, sealing surfaces, and electrical contacts. For parts requiring anodizing, plating, or painting, define coating thickness and masking areas to protect assembly clearances and grounding functions.
How Can Material Cost and Lead Time Be Controlled?
Material grade, supply condition, stock form, heat treatment, surface finish, and inspection requirements all affect cost and lead time.
- Select material according to actual loads instead of using the highest-strength grade for every feature.
- Evaluate plate, bar, or extrusion sizes close to the finished dimensions to reduce material removal.
- Confirm material condition, heat treatment, and surface finish early to minimize mid-process changes.
- Define critical dimensions, coating acceptance, and required reports to reduce acceptance disputes at delivery.
What Information Should Be Included in an RFQ?
Provide information that defines the part, its deployment environment, and acceptance criteria:
- A 2D drawing or 3D model with datums, critical dimensions, and tolerances.
- Material grade, condition, product form, and applicable standard.
- Deployment location and environment, such as coastal, desert, indoor, or high-humidity service.
- Operating temperature, loads, contact media, and expected service life.
- Surface-finish standard, thickness, masking areas, and acceptance requirements.
- Quantity, inspection items, and material certificates or inspection reports required.
“Outdoor use” alone does not define the protection system. Specify the actual exposure to salt, humidity, dust, and thermal cycling. A material certificate confirms material information; an inspection report verifies the part against the drawing. They are not interchangeable.
How Does Weldo Support CNC Machining for Defense Equipment Parts?
Weldo can evaluate the machining route, critical dimensions, and surface finishes based on the drawing, material requirements, and deployment environment. Services include multi-axis CNC machining, precision grinding, wire EDM, secondary finishing, and dimensional inspection. Material certificates, inspection reports, and acceptance documents are confirmed against the project drawing and purchasing specifications.
To request a part evaluation, submit the drawing, quantity, deployment environment, and acceptance requirements through Weldo’s defense industry machining page.
Frequently Asked Questions
Do U.S. or European projects have uniform material and surface-finish requirements?
There is no single selection scheme for every project. Requirements depend on the deployment location, equipment application, purchasing contract, and customer specifications. If the contract specifies a MIL, EN, ISO, or customer standard, follow the applicable revision and acceptance clauses.
Can 316 stainless steel completely prevent corrosion in coastal environments?
The grade alone cannot guarantee this. 316 is generally more suitable than 304 for higher-chloride environments, but temperature, salt concentration, liquid accumulation, and crevices still affect pitting and crevice-corrosion risk. Drainage, surface condition, and maintenance should also be considered.
How can assembly dimensions be maintained after anodizing?
Specify the anodizing type, coating thickness, mating surfaces, and masking areas on the drawing. Allow for the coating during machining and inspect critical fit dimensions after finishing.
Conclusion: Match the Material and Surface Finish to the Deployment Environment
For U.S. projects, distinguish humid coastal conditions, hot and dusty conditions in the Southwest, and cold, salt-exposed conditions in the north.
For Middle East projects, distinguish inland desert service from the Gulf coast.
For European projects, consider cold and humid conditions in the north, wet conditions in the west, and coastal salt exposure in the south.
High-strength aluminum parts require a review of both temper and protection. Chloride exposure requires evaluation of stainless-steel grade and crevice-corrosion risk. Sand-worn areas need specified wear protection, while electrical-contact areas require a defined coating and masking plan. Put the deployment environment, material condition, surface finish, and acceptance criteria on the drawing or purchasing specification to align material selection, machining, and inspection.