
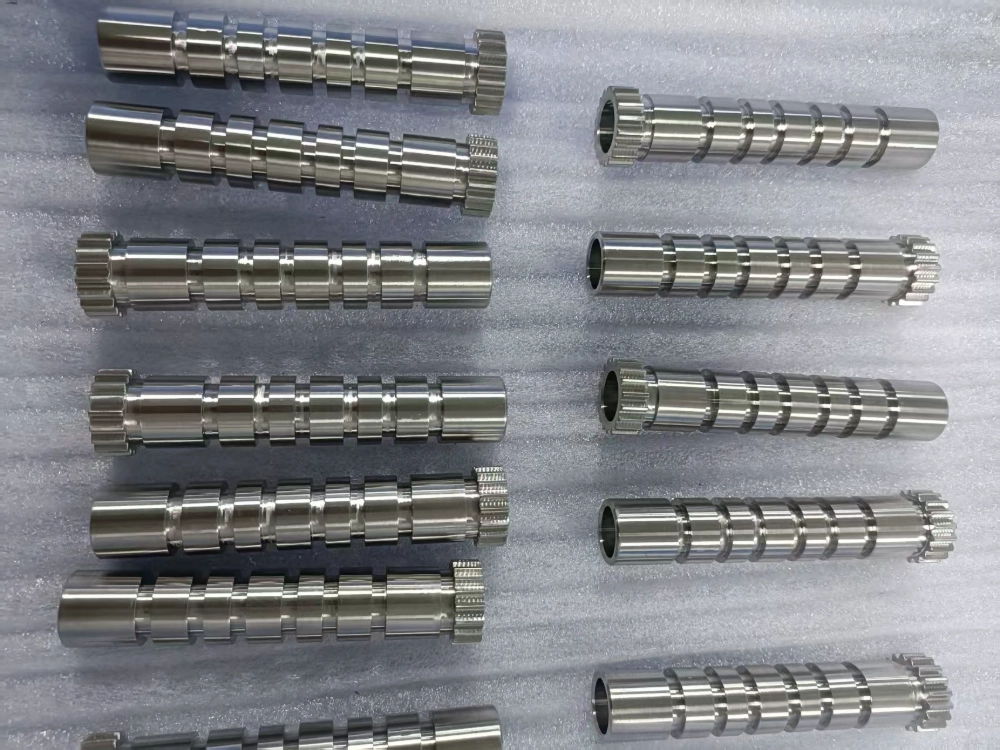
Steel CNC Machining Services
Custom steel parts made to drawing for shafts, gears, tooling, and load-bearing components. We review the grade, material condition, machining route, heat treatment, and finish to suit the part’s function and final dimensions.
- Carbon, Alloy & Tool Steel
- 시제품부터 양산까지
- 열처리 및 표면 처리
Steel Properties Depend on Grade and Condition
Carbon content, alloying, product form, and heat treatment affect strength, toughness, hardness, and machining behavior. These broad references cover selected grades and conditions.
- 밀도
- 7.75–7.90g/cm³
- 인장 강도
- 370–2,000MPa
- 항복 강도
- 200–1,800MPa
- 연신율
- 5–35%
- 열전도율
- 20–60W/(m·K)
- Selected Hardened Tool Steels
- 60–65HRC, grade- and treatment-dependent
Ranges describe different materials and conditions, not one steel specification. Confirm the required properties and hardness test method from the governing material standard and supplier records.
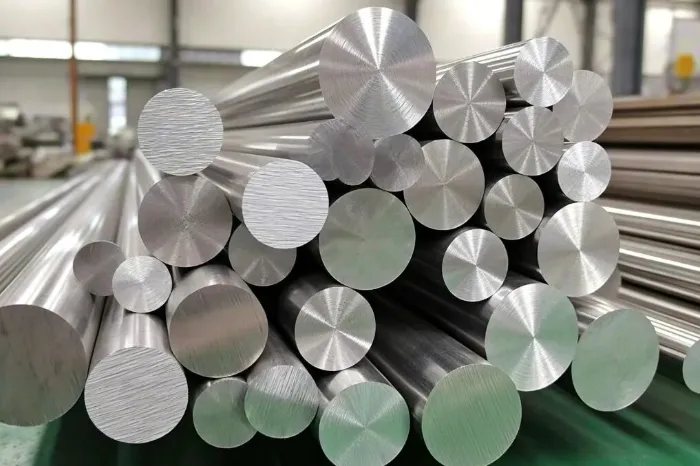
Choose the Steel for the Part
Compare machining behavior, strength, hardenability, wear, and corrosion exposure before selecting the material.
탄소강
Economical structural and engineering grades for general machine parts. Carbon content and supplied condition influence cutting behavior, strength, and heat-treatment response.
- ASTM A36
- AISI 1018
- AISI 1045
- C45
- AISI 1215
1018 is widely used for general components. Free-machining 1215 improves chip control for repetitive turning. Medium-carbon 1045 and C45 are options where higher strength or local hardening is required.
Applications, treatment & finishing
- 일반적인 부품
- Brackets, bases, shafts, pins, spacers, flanges, and general machine components.
- Heat-treatment considerations
- 1018 may be carburized. Suitable medium-carbon grades can be quenched and tempered or induction-hardened. A36 is a structural specification and should not be treated as a controlled hardening grade.
- 표면 보호
- Black oxide with an appropriate sealer, zinc or nickel plating, phosphating, and protective paint, selected for the application and final fits.
- 가공 참고 사항
- Plan chip control, burr removal, clamping, and the condition of welded or cold-drawn stock. Free-machining grades may have limitations for welding or demanding service conditions.
합금강
Options for higher hardenability, strength, toughness, and demanding mechanical loads. Final performance depends on composition, section size, and treatment.
- SAE 4140
- 42CrMo4
- SAE 4340
- 34CrNiMo6
- SAE 8620
Machinability changes with hardness and supplied condition. Annealed stock supports material removal before treatment; prehardened stock requires tooling and workholding matched to its actual hardness.
Applications, treatment & finishing
- 일반적인 부품
- Gears, drive shafts, couplings, hubs, spindles, and heavily loaded fasteners.
- Heat-treatment considerations
- 4140 and 4340 are commonly quenched and tempered. 8620 is commonly carburized for a hard case and tougher core. Define final hardness, case depth where relevant, and machining allowance.
- Surface and wear treatments
- Grade-appropriate nitriding or induction hardening, black oxide, zinc or nickel plating, and phosphating. Confirm compatibility with the required core condition.
- Material specification
- SAE and EN designations listed here are separate material choices. Similar grades are not automatically interchangeable; confirm chemistry, product standard, condition, and certification before substitution.
공구강
Grade-specific solutions for wear resistance, hardness, impact loading, or hot-work service. Selection balances toughness, hardness, and dimensional stability.
- AISI A2
- AISI D2
- AISI H13
- AISI O1
- 1.2363
- 1.2379
- 1.2344
- 1.2510
Tool steels are often rough-machined in the annealed condition. After hardening and tempering, critical geometry may require grinding, hard machining, or EDM with appropriate surface-integrity controls.
Applications, treatment & finishing
- 일반적인 부품
- Punches, dies, mold inserts, cutting tools, gauges, fixtures, and wear components.
- Heat-treatment considerations
- Use a grade-specific hardening and tempering route. Plan stress relief where appropriate, account for distortion, and retain finishing allowance on critical features.
- 마감 옵션
- Precision grinding and polishing, or compatible nitriding, PVD coatings, and black oxide. Coating temperature must suit the material’s heat-treatment condition.
- Inspection notes
- Specify final hardness, datums, form tolerances, surface condition, and whether acceptance follows heat treatment and finishing.
스테인리스강
Corrosion-resistant grades with different machining, strength, and cleaning characteristics. The environment and required material condition guide selection.
- 303
- 304
- 316 / 316L
- 17-4 PH
303 prioritizes machinability, with corrosion and welding tradeoffs. 304 and 316L require effective control of work hardening and heat. 17-4 PH provides higher strength in a specified aging condition.
Applications, treatment & finishing
- 일반적인 부품
- Valves, fittings, housings, food-equipment components, and medical or laboratory parts made to the required specification.
- Heat-treatment considerations
- Austenitic 303, 304, and 316L are not hardened by conventional quenching and tempering. 17-4 PH is strengthened by precipitation hardening; define the required final condition.
- 마감 옵션
- Grade-appropriate passivation, electropolishing, bead blasting, brushing, and polishing. Surface texture and corrosion acceptance should be defined separately.
- Material guide
- Explore stainless steel machining →
Specify the governing material standard, exact grade, product form, supplied condition, final hardness, and required certification. Grade examples do not establish automatic equivalence between standards.
Drawing-Based Steel Machining Capabilities
Confirm the route from the part’s dimensions, material condition, critical features, and final inspection requirements.
Machining Reference Parameters
| Part-envelope reference | 최대 3000 × 1600 × 1000 mm*Subject to machine selection, workholding, stock, and tool access. |
|---|---|
| Turning references | Ø1–200 mm / length up to 1000 mm*Independent range references; diameter, unsupported length, rigidity, and support must be reviewed together. |
| Thin-wall reference | From 0.5 mm*Depends on wall height, span, material condition, clamping, and finishing. |
| Dimensional references | General ±0.05 mm / selected features down to ±0.005 mm*Quotation references only. Drawing tolerances, process, temperature, and measurement conditions require agreement. |
| 표면 거칠기 | Ra 0.2–3.2 µm*Process-dependent. Finer values may require grinding or other finishing beyond milling or turning. |
| Hardened workpiece reference | Up to 60 HRC*Grade- and feature-specific review determines hard machining, grinding, or EDM suitability. |
Engineering Controls for Steel Parts
Grade and Material Condition
Review alloy, stock form, hardness, residual stress, and any welds before setting the machining route.
Stable Cutting and Workholding
Match tool grade, engagement, speed, coolant, and chip evacuation to hardness and feature access.
열처리 수당
Plan roughing, stress relief where appropriate, hardening, and final sizing to manage material movement.
Finished-Part Acceptance
Define datums, fits, hardness, surface condition, and inspection after treatment or coating where required.
*Planning references confirmed against the drawing. Maximum size, minimum diameter, thin walls, hardness, tight tolerance, and roughness are reviewed separately and should not be assumed achievable together.
강철 부품의 표면 처리
Choose a complete finish system for corrosion exposure, wear, appearance, coating thickness, and assembly fit.
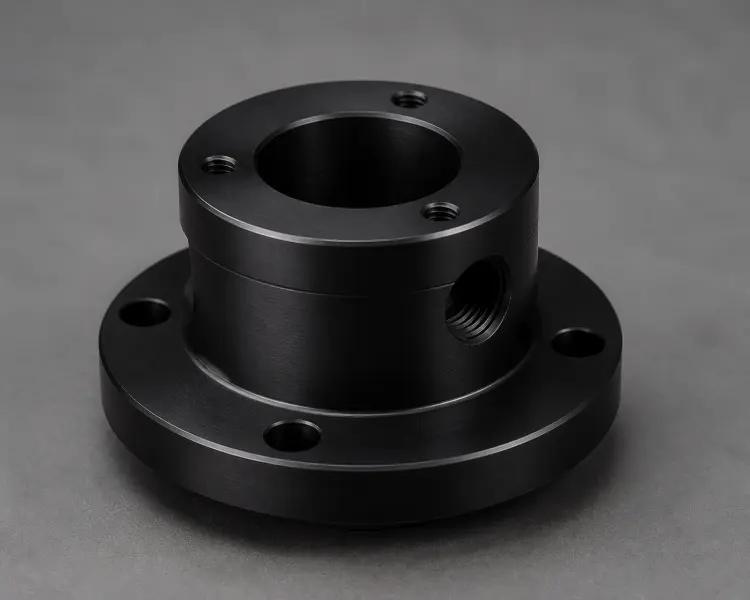
흑색 산화
A thin black conversion finish, commonly sealed with oil or wax for limited corrosion protection. Specify the required after-treatment and storage conditions.

아연 도금
Sacrificial corrosion protection with specified thickness, passivate, and masking. Define any required embrittlement-relief process for high-strength parts.
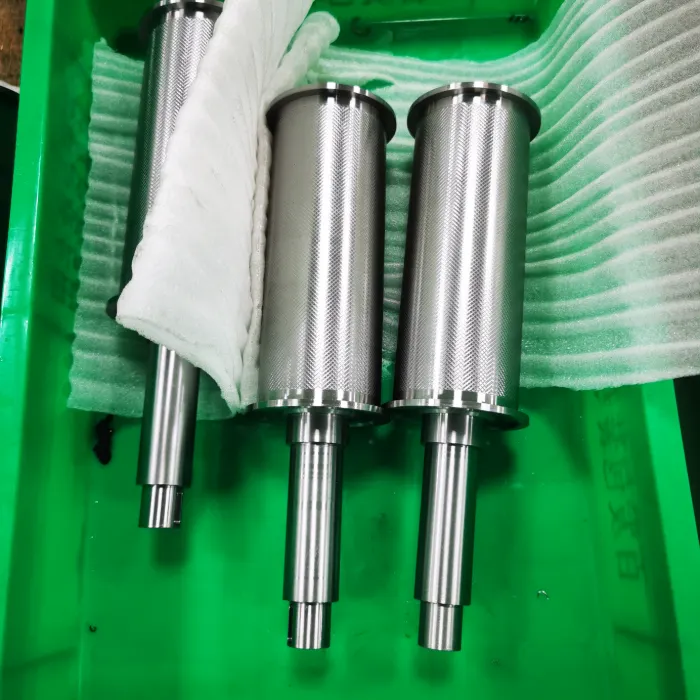
니켈 도금
A barrier coating for appearance, wear, or corrosion performance. Specify electrolytic or electroless nickel, thickness, and the final fit requirements.
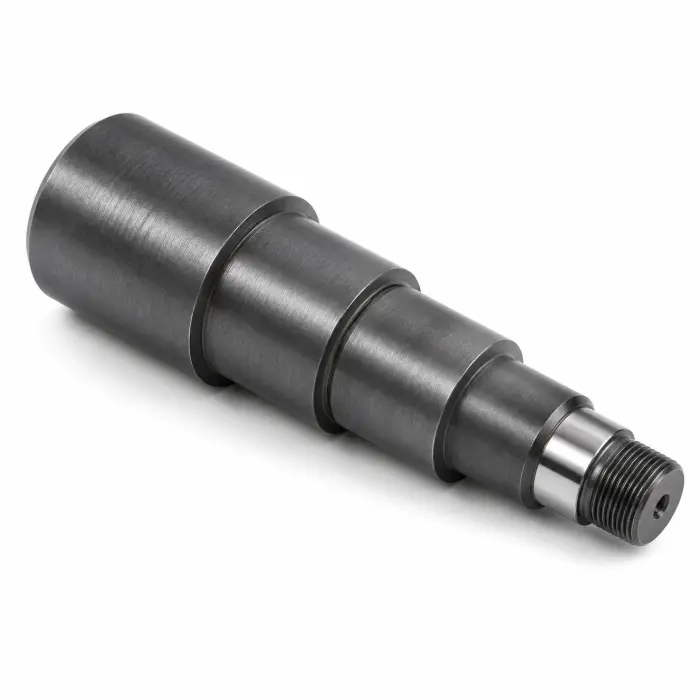
인산염 처리
A conversion coating used for oil retention or paint preparation. Corrosion performance depends on the complete oil, sealer, or paint system.
Explore more surface finishing options →
Allow for coating buildup on bores, threads, and fits. Hardening, carburizing, nitriding, plating, and conversion coatings serve different purposes; define the process sequence and finished acceptance condition.
Machining and Inspection Resources
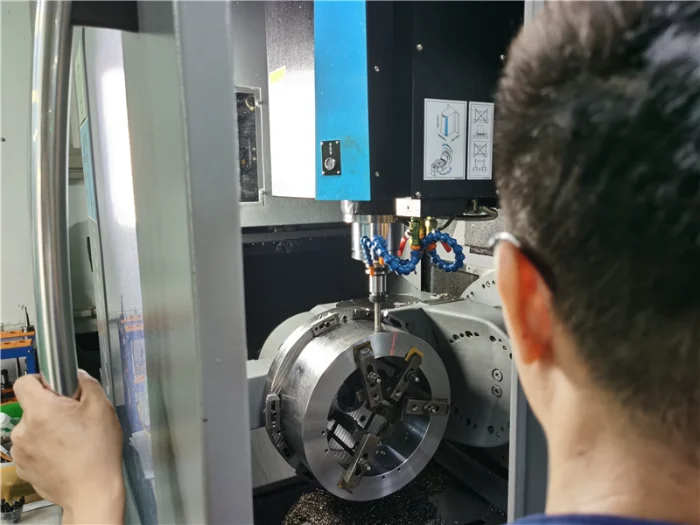
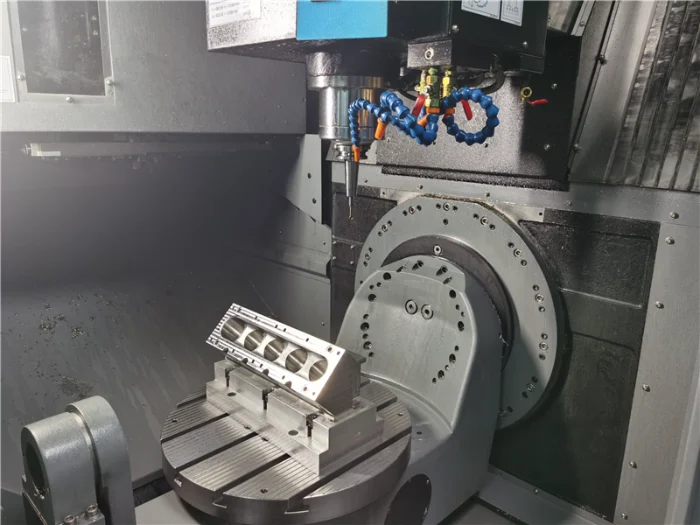
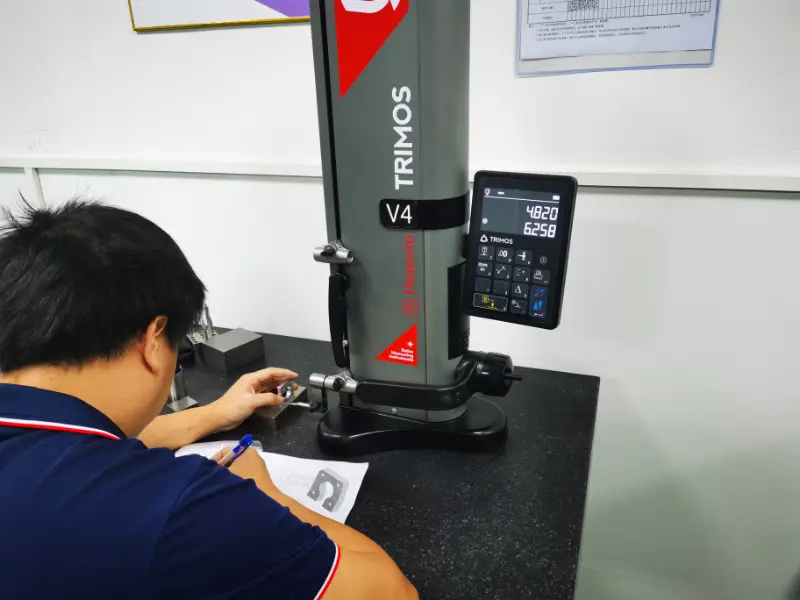
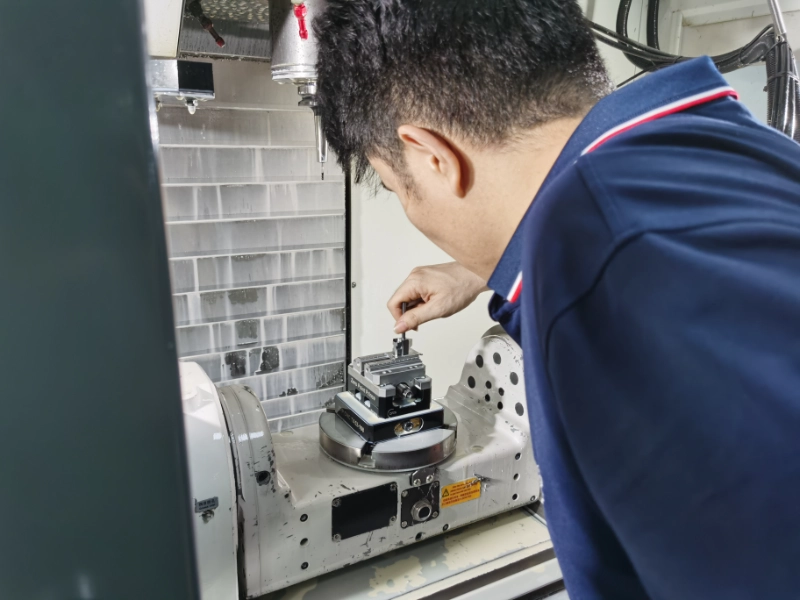
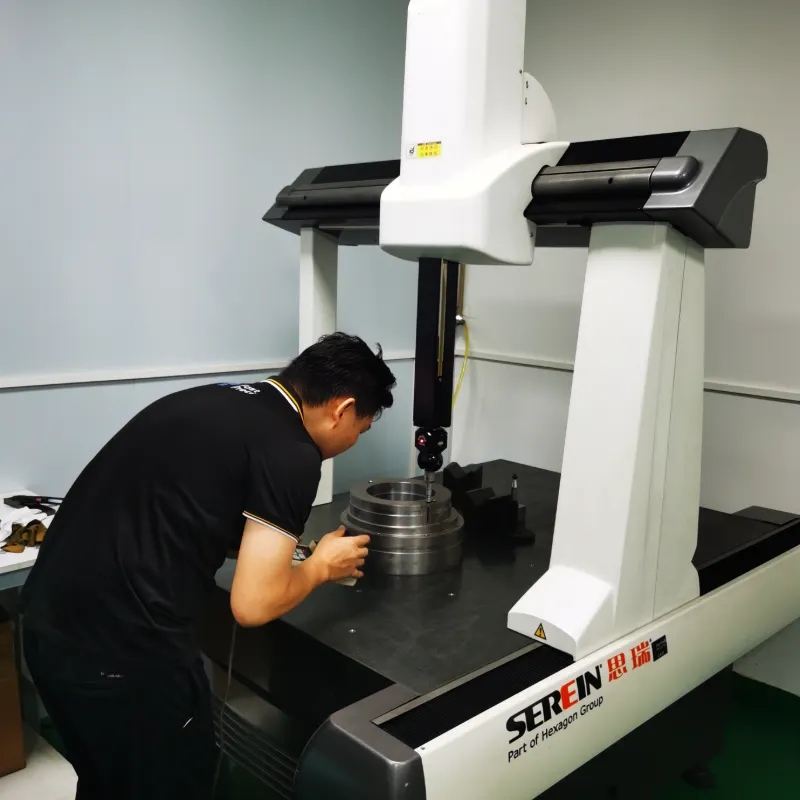
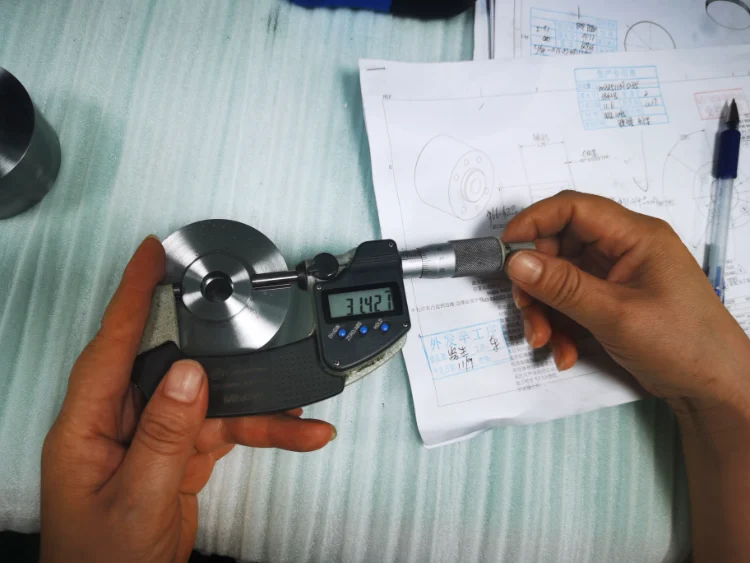
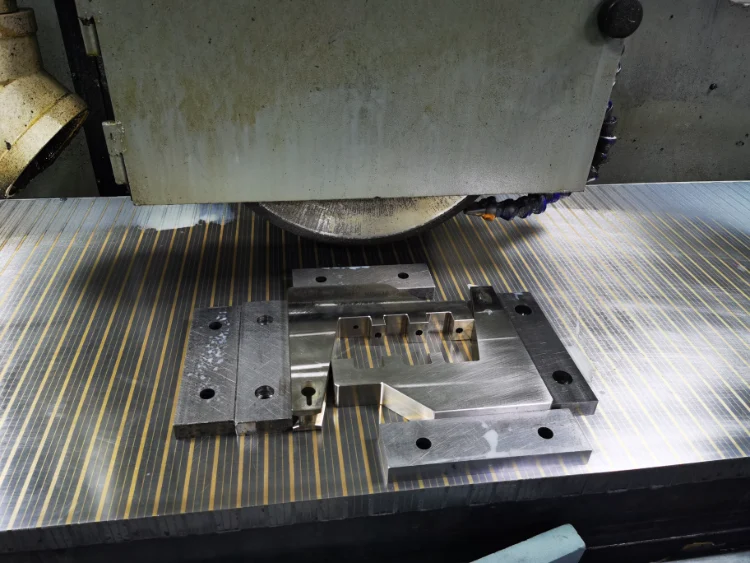
Machining, grinding, EDM, and dimensional inspection support the agreed production route and acceptance requirements for steel parts.
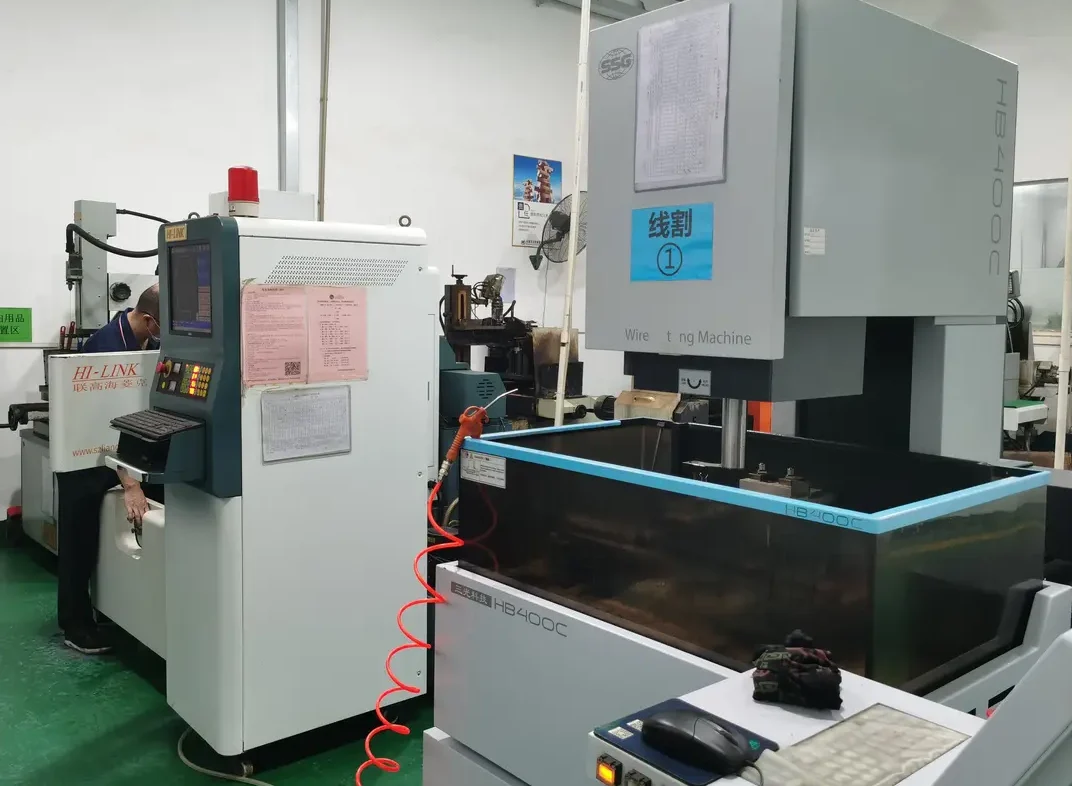
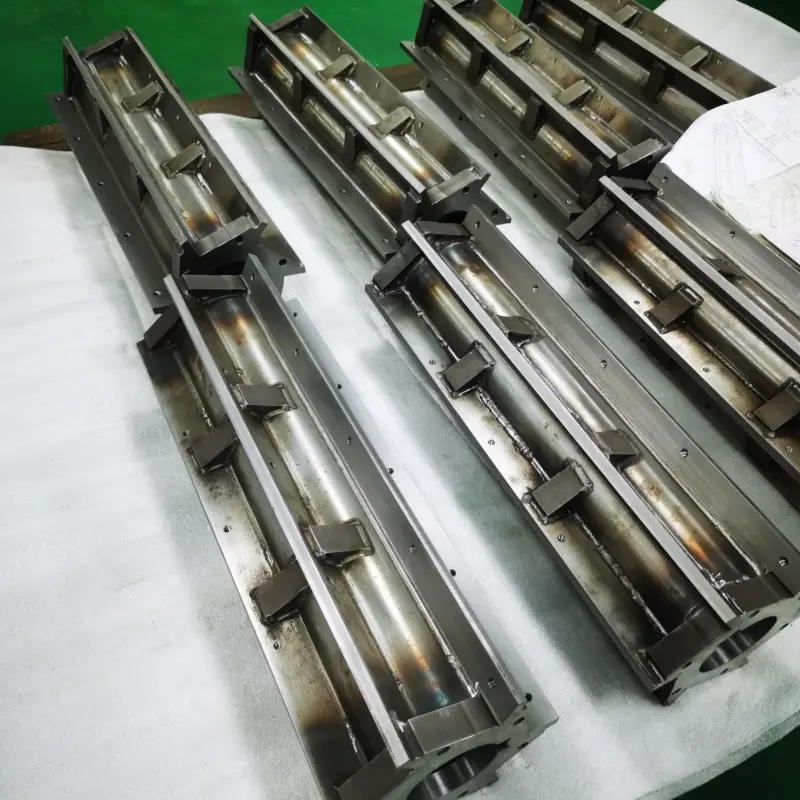
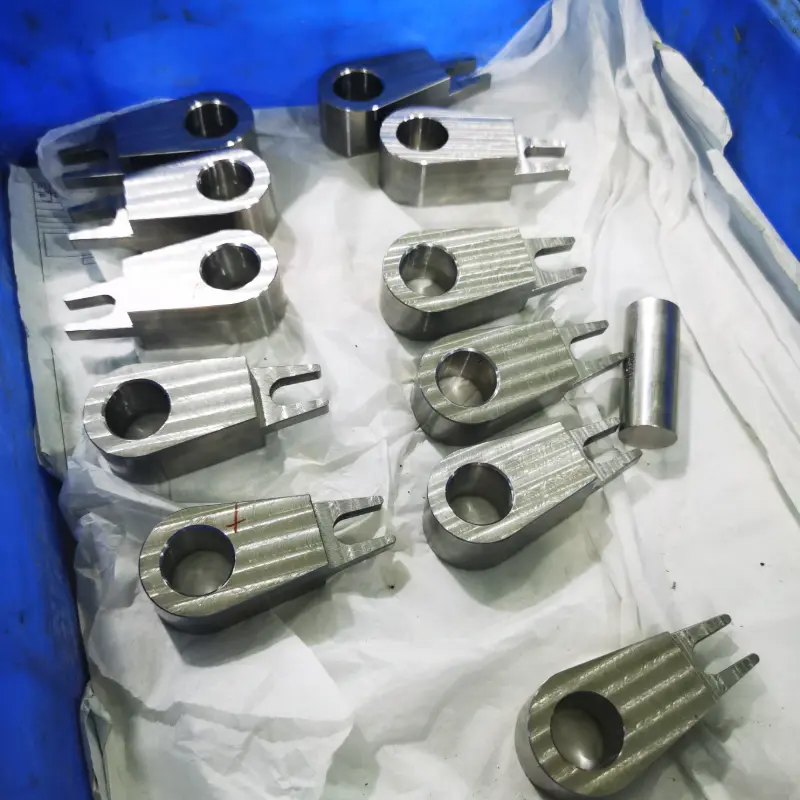
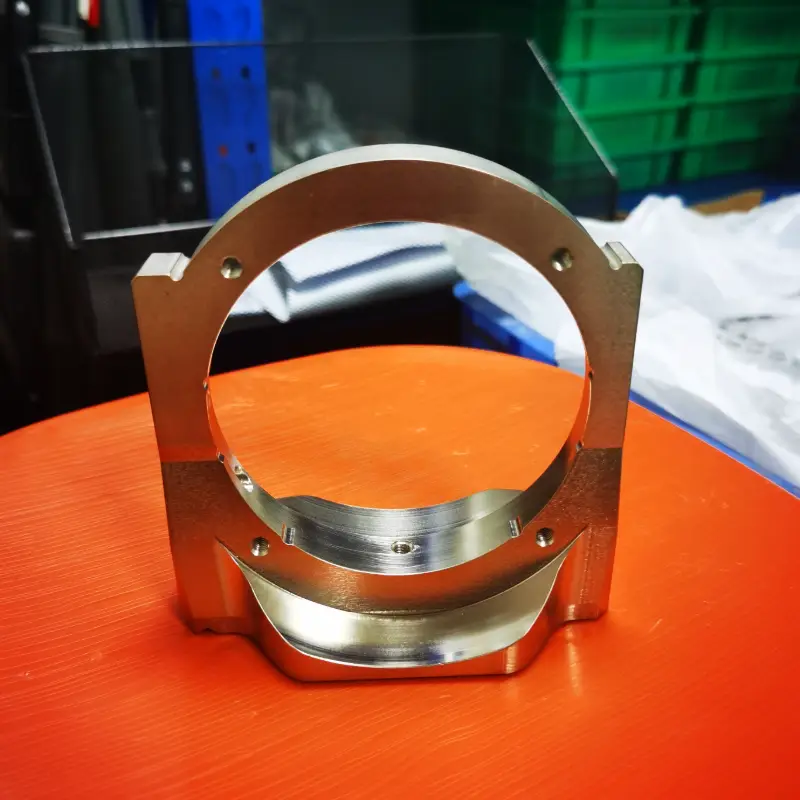
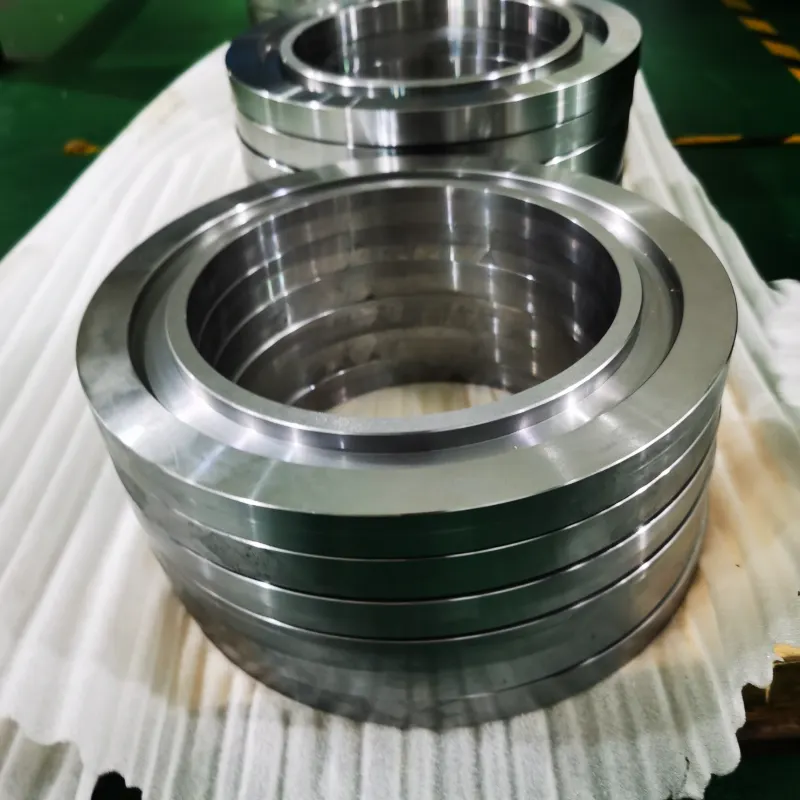
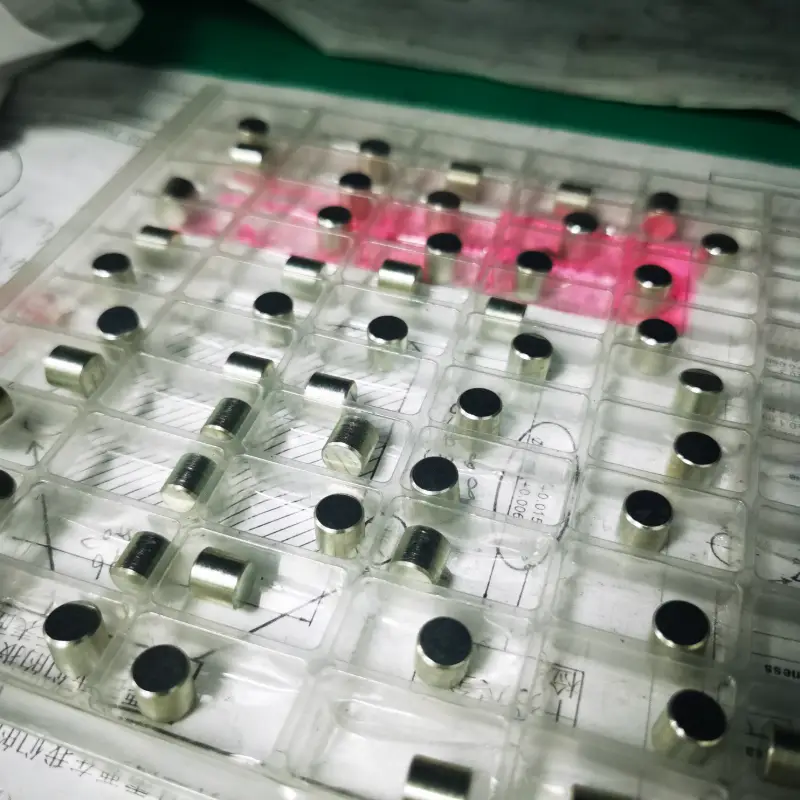
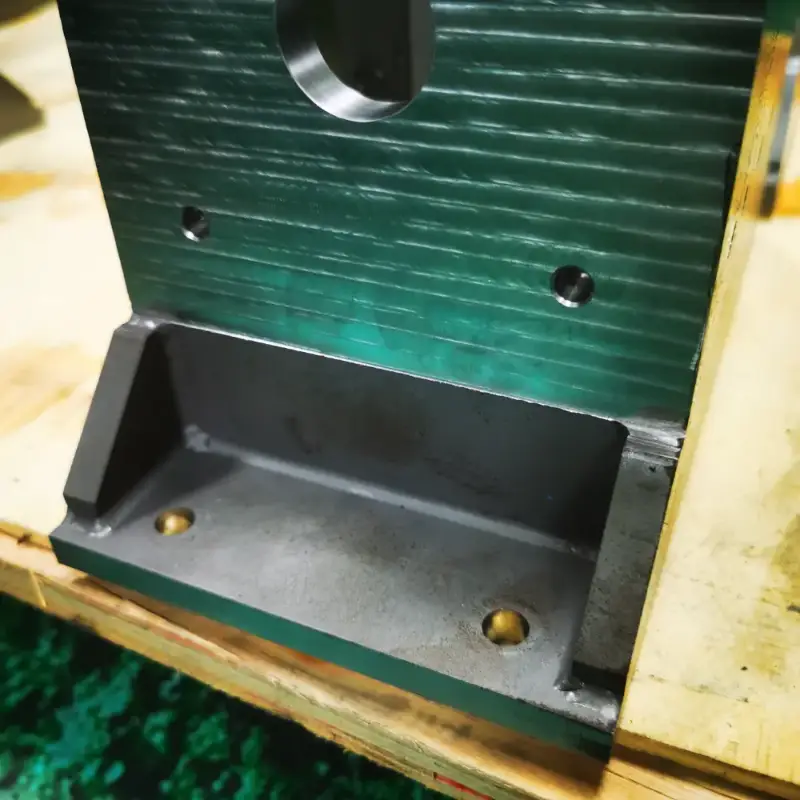
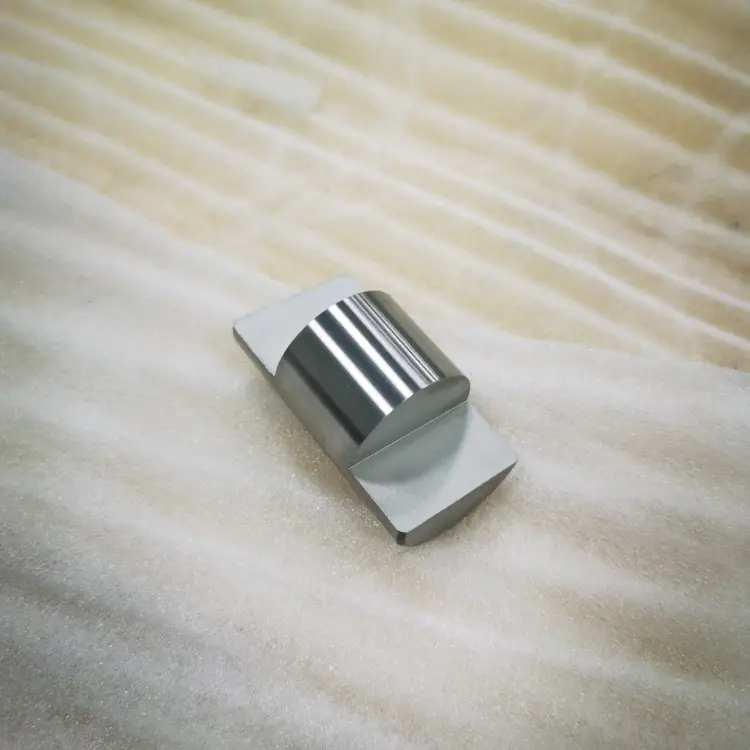
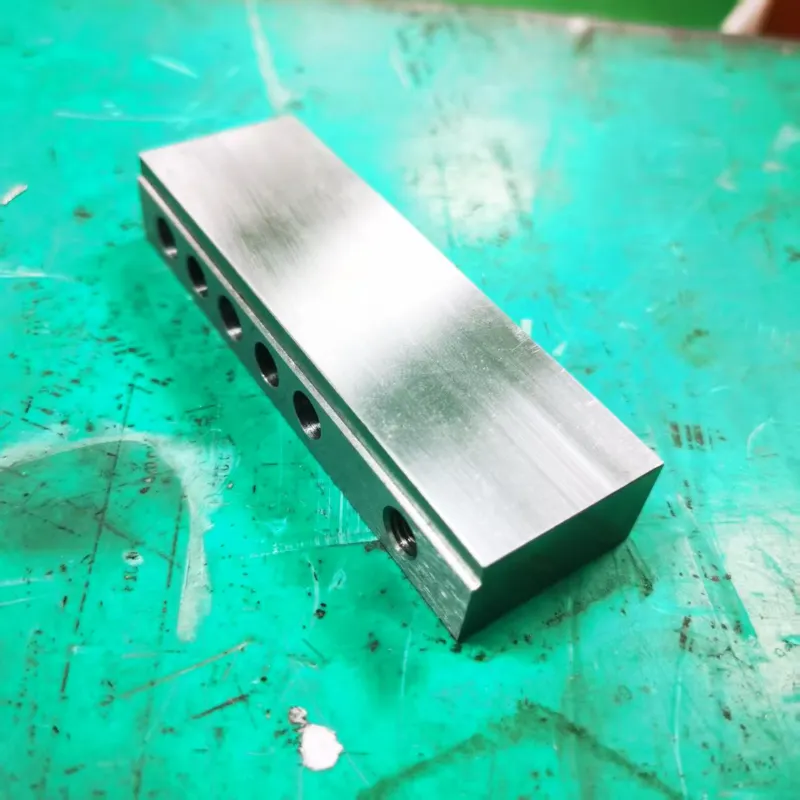
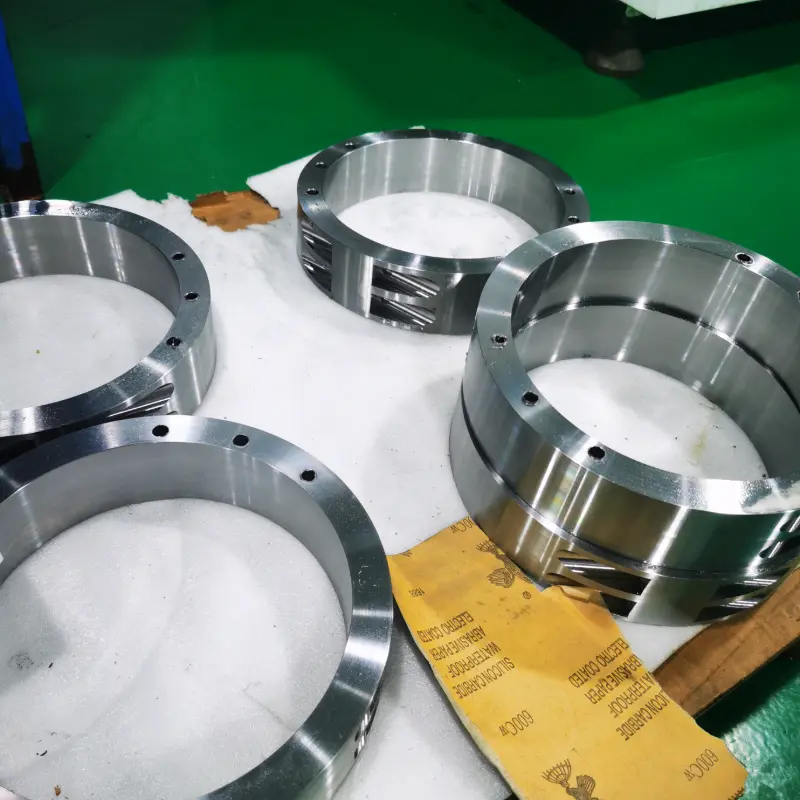
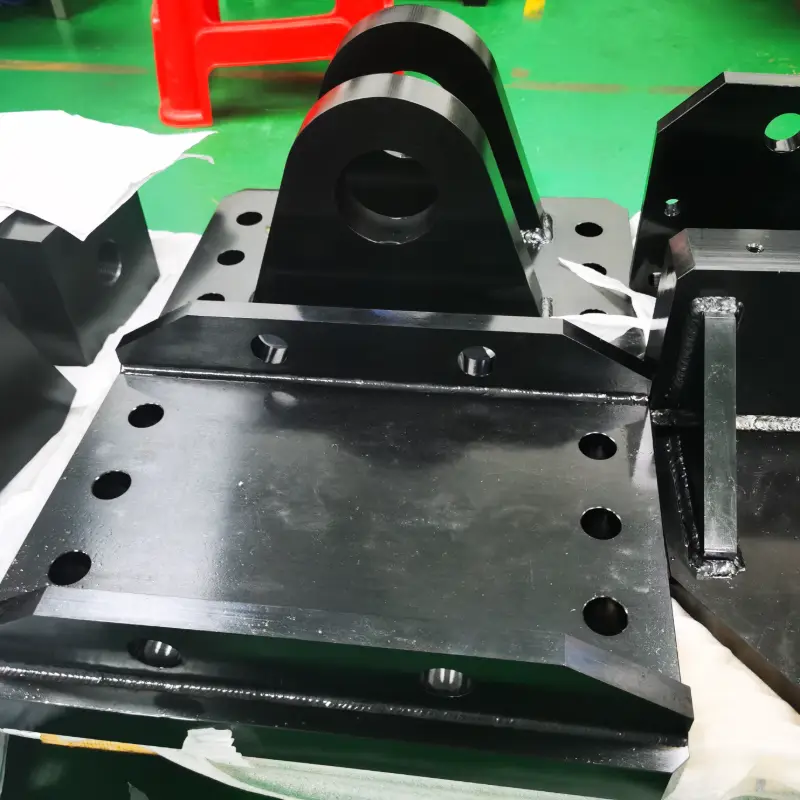
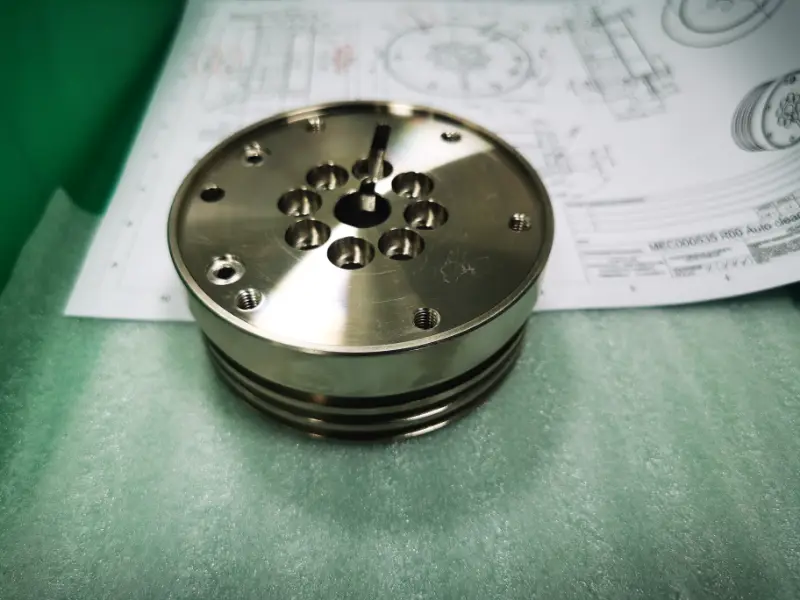
Weldo Steel Machining Projects
Examples of steel machining projects completed by Weldo, including welded components, shafts, plates, and other custom parts with different material and finishing requirements.

Steel Machining Questions
Should steel be heat-treated before or after machining?
The sequence depends on the grade, supplied condition, final hardness, and tolerance. A common route is rough machining, stress relief where appropriate, hardening and tempering, then final grinding or machining. Prehardened stock can be machined directly when the required properties and process allow.
How is heat-treatment distortion managed?
Review stock condition, balanced removal, section changes, fixturing, and the treatment route. Leave suitable finishing allowance on critical features and inspect after treatment. These measures reduce risk, but heat treatment does not guarantee unchanged dimensions.
What is the difference between 1018 and 1045?
1018 is a low-carbon steel commonly used for general components and weldments. 1045 has more carbon and can achieve greater hardness and strength through suitable heat treatment. Actual properties, machining behavior, and weldability depend on product form and material condition.
경화강은 CNC 가공이 가능한가요?
Yes, where hardness, geometry, rigidity, and tooling permit. Suitable carbide, ceramic, or CBN tools may be used for selected operations. Grinding or EDM can be more appropriate for very hard material, small details, or demanding form and surface requirements.
What matters most when milling or turning steel?
Confirm the grade and hardness, maintain stable clamping, and match cutting tools and parameters to the operation. Manage heat, tool wear, burrs, and chips. Include any later heat-treatment movement or coating allowance before finishing critical dimensions.
Which finish gives the best corrosion protection?
There is no universal choice. Zinc provides sacrificial protection; nickel is a barrier coating; black oxide and phosphate commonly rely on an oil, sealer, or paint system. Select the specified process and thickness for exposure, wear, appearance, and final fits.