Weighing 6061 vs 7075-t6 Aluminum starts with one question: what does your part need? If it needs welding, corrosion resistance, easy machining, and controlled cost — which covers the vast majority of machined and structural applications — choose 6061. Choose 7075-T6 only when a load-verified design genuinely requires an extreme strength-to-weight ratio and the design can work around its welding, corrosion, and cost weaknesses.
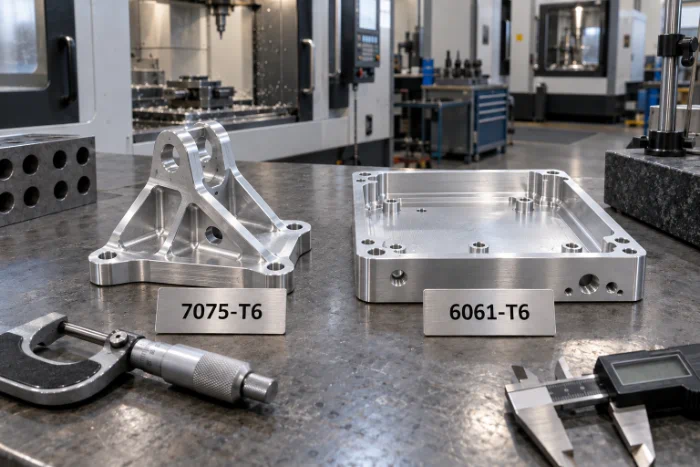
Quick Comparison of 6061 vs 7075-t6 Aluminum
6061 and 7075-T6 are both heat-treatable wrought aluminum alloys, but they belong to two different alloy families with fundamentally different design orientations:
- 6061 (6xxx series): With magnesium and silicon as the principal alloying elements, it trades peak strength for excellent machinability and well-rounded all-around performance.
- 7075-T6 (7xxx series): With zinc as the principal alloying element, supplemented by magnesium and copper, it is one of the highest-strength commonly used aluminum alloys — but at a significant cost in corrosion resistance, joinability, and price.
| Property | 6061 | 7075-T6 |
| Alloy family | 6xxx (Mg + Si) | 7xxx (Zn + Cu + Mg) |
| Tensile strength | ≈310 MPa (45 ksi, plate/bar T6, ASTM B209/B211); 290 MPa (42 ksi, extruded shapes T6, B221) | ≈572 MPa (83 ksi) |
| Yield strength | ≈276 MPa (40 ksi, plate/bar T6); 240 MPa (35 ksi, extruded T6) | ≈503 MPa (73 ksi) |
| Specific strength (strength/density) | ≈115 MPa·cm³/g | ≈203 MPa·cm³/g (≈1.77× that of 6061-T6) |
| Modulus of elasticity | ≈68.9 GPa (10.0 Msi) | ≈71.7 GPa (10.4 Msi) |
| Density | 2.70 g/cm³ (0.0975 lb/in³) | 2.81 g/cm³ (0.1015 lb/in³) |
| Thermal conductivity | ≈167 W/(m·K) (96 BTU/(hr·ft·°F)) | ≈130 W/(m·K) (75 BTU/(hr·ft·°F)) |
| Electrical conductivity (IACS) | ≈40% (T6; ≈47% in O temper) | ≈33% |
| Brinell hardness | ≈30–95 HB (temper dependent) | ≈150 HB |
| Weldability | Excellent | Poor (fusion welding not recommended) |
| Corrosion resistance | Excellent | Moderate (coating required in harsh environments) |
| Relative material cost | Low (baseline, ≈$1.4–1.9/lb) | 1.5–2.5× baseline (≈$3.0–4.4/lb) |
Unit conversions: 1 ksi = 6.895 MPa, 1 Msi = 6.895 GPa, 1 lb/in³ = 27.7 g/cm³, 1 W/(m·K) = 0.5778 BTU/(hr·ft·°F).
Three key clarifications that most comparison articles overlook:
- 7075-T6 is far stronger, but its stiffness is almost unchanged. Its modulus of elasticity is only about 4% higher than 6061’s. If the part’s failure mode is excessive deflection rather than yield, changing the alloy will not solve the problem — change the geometry, wall thickness, or rib layout instead.
- 6061 dissipates heat better. Its thermal conductivity is about 28% higher, so heat sinks, LED housings, and thermally loaded cavities should default to 6061.
- Neither is a good electrical conductor. Conductivity is only 33–47% that of pure aluminum (61%+ IACS), and 33% vs. 40% in the T6 temper — neither suits current-carrying parts. Both are non-ferromagnetic and suitable for MRI-adjacent and instrument structures (though machining must control ferrous contamination chips).
Chemical Composition: The Root of the Performance Gap
| Element (wt %) | 6061 | 7075 | Role |
| Al | Balance | Balance | Matrix |
| Zn | ≤0.25 | 5.1–6.1 | Primary source of strength in the 7xxx series |
| Mg | 0.8–1.2 | 2.1–2.9 | Strengthening, corrosion resistance |
| Cu | 0.15–0.40 | 1.2–2.0 | Strengthening (also reduces corrosion resistance) |
| Si | 0.4–0.8 | ≤0.40 | Improves castability and weld fluidity |
| Cr | 0.04–0.35 | 0.18–0.28 | Grain control, stress-corrosion resistance |
| Mn | ≤0.15 | ≤0.30 | Strengthening, grain refinement |
| Ti | ≤0.15 | ≤0.20 | Grain refinement |
| Fe | ≤0.50–0.70 | ≤0.50 | Impurity element, tightly capped |
| Others | Each ≤0.05, total ≤0.15 | Each ≤0.05, total ≤0.15 | Impurity control |
In 7075, Zn + Cu + Mg total roughly 9–10% — the direct reason it achieves near-steel-level strength, and equally the common root of its poor weldability, weak corrosion resistance, and high price. A single composition table explains the origin of the two alloys’ main performance differences.
About the Heat Treatment Tempers of 6061
The mechanical properties of 6061 span a wide range depending on the temper. Writing only “6061” is not a complete procurement specification. Common tempers:
| Temper | Treatment | Characteristics | Typical uses |
| 6061-O | Annealing | Softest, best formability | Bending, deep-drawn parts |
| 6061-T4 | Solution heat treatment + natural aging | Medium strength, can be aged further later | Parts formed before aging |
| 6061-T5 | High-temperature forming, cooling, then artificial aging | Strength between T4 and T6 | Extrusions |
| 6061-T6 | Solution heat treatment + artificial aging | General-purpose peak-strength temper, industry default | Machined parts, structural parts |
| 6061-T651 | T6 + stress-relief stretch | Same strength as T6, better dimensional stability | Precision-machined plate |
Unless otherwise noted, the industry quotes and machines to 6061-T6 by default — the reference values cited in this article are also based on the 6061-T6 temper.
The same logic applies to 7075: plate defaults to T651 (T6 + stress-relief stretch), with strength equal to T6 and better flatness and post-machining dimensional retention; for sustained load in humid environments, T73 trades about 12% of yield strength for markedly better stress-corrosion cracking resistance and is a standard choice for aerospace structures.
Procurement Specifications and Certifications (US/EU Standards Mapping)
Before placing an order, confirm four elements: alloy + temper + product form + standard. The common standards for the two materials map as follows:
| Item | 6061 | 7075-T6 |
| US standards | ASTM B209 (plate) / B211 (bar) / B221 (extruded shapes); AMS-QQ-A-250/11, AMS 4025 / 4027 | ASTM B209 / B211; AMS-QQ-A-250/12 (aerospace certified) |
| European designation | EN AW-6061 (3.3211, AlMg1SiCu) | EN AW-7075 (3.4365, AlZnMgCu1.5) |
| Material certificates | US: Mill Test Report (with ASTM standard); EU: EN 10204 3.1 | Same; aerospace parts add AMS certification per customer spec |
| Compliance declarations | RoHS / REACH conformity | Same |
| Surface treatment specs | MIL-PRF-8625 Type II / Type III; European counterpart EN 12373 | Same |
Procurement note: For the same “6061” alloy, extruded shapes (B221) and plate/bar (B209/B211) have different T6 minimum strengths (290 vs. 310 MPa). RFQs and drawing callouts must state “alloy + temper + form + standard” in full, or the delivered properties may not match expectations.
Cost of 6061 vs 7075-t6 Aluminum
Material Cost
| Item | 6061 | 7075 (T651 as an example) |
| Raw material price | ≈3.0–4.2/kg (1.4–1.9/lb) | ≈6.5–9.8/kg (3.0–4.4/lb) |
| Aerospace certified material (AMS-QQ-A-250/12) | — | 12+/kg (5.5+/lb) |
| Availability | Ample stock, full size range | Some sizes require ordering |
| Price multiple | 1× | 1.5–2.5× |
Raw material prices fluctuate with the ingot market; the ranges above are reference values. Formal RFQs are quoted at current list prices.
Machining Cost
| Cost item | 6061 | 7075-T6 |
| Cutting speed / feed | Can be run full out | Reduced 15–25%, machine-hour cost rises |
| Tool life | Long | Short, frequent tool changes |
| Thin-wall / sharp-corner features | Prone to distortion | Good dimensional retention, increased edge-chipping risk |
| Deburring | Heavier burden (continuous stringy chips, chip tangling, exit burrs) | Light burden (brittle, crisp chips, fewer burrs) |
| Overall machining cost impact | Baseline | Typically +20–40% |
Total cost picture: For large structural parts where raw material accounts for about 55% of total cost, switching from 6061 to 7075-T6 can raise per-part total cost by about 70% (estimated at a mid-case of 1.75× material price with machining unchanged; total cost can double when material runs 2.5× with a 40% machining premium). For precision thin-wall parts where raw material is only about 15%, the pull from material price increase is limited, and 7075’s crisp chip breakage offsets part of the machining premium, narrowing the total-cost gap to roughly 30–50% — but there is no single-digit gap. What determines economics is the part’s geometry and volume, not the alloy name — the safest approach is always to quote both materials in parallel.
Machining, Joining, and Surface Treatment
CNC Machining Performance
| Machining dimension | 6061 | 7075-T6 |
| Overall rating | Excellent | Good |
| Spindle speed / feed | Can be run full out | Reduced 15–25% |
| Tool wear | Low | High (coated carbide tooling required) |
| Chip form | Continuous stringy, prone to tangling | Brittle fragments, smooth chip evacuation |
| Machined surface finish | Ra 0.4 µm achievable, Ra 0.8 µm stable | Ra 0.8 µm achievable, narrower parameter window |
| Thin-wall parts | Risk of distortion | Good geometric retention |
| Achievable tolerances | ±0.01–0.02 mm (±0.0004–0.0008 in) | ±0.01–0.02 mm (comparable) |
| Preferred applications | General complex parts, prototypes | Strength-driven structural parts |
Joining Methods
| Joining method | 6061 | 7075-T6 |
| Fusion welding (MIG/TIG) | ✅ Excellent — standard filler metals, post-weld heat treatment recovers most of the strength | ❌ Not recommended — hot cracking, severe heat-affected-zone strength loss |
| Brazing | ✅ Feasible | ⚠️ Narrow temperature window, requires specialized filler metals |
| Riveting | ✅ | ✅ Standard aerospace practice |
| Bolting / fastening | ✅ | ✅ |
| Structural adhesive bonding | ✅ Good bond after surface treatment | ⚠️ Feasible, but bondline corrosion and surface-pretreatment compatibility must be controlled (PAA or sol-gel pretreatment) |
Once a part must be welded, the decision is over — 7075 is eliminated before any spec table.
Surface Treatment Performance
| Surface process | 6061 | 7075-T6 | Verdict |
| Anodizing Type II (decorative) | Uniform color, stable dyeing | Tends to darken, batch color variation | Appearance parts: 6061 |
| Hardcoat anodizing Type III | Uniform coating | Harder coating, better wear resistance | Wear parts: 7075 |
| Powder coating | ✅ Good | ✅ Good (pretreatment required) | Tie |
| Alodine (chromate/chrome-free passivation) | ✅ Excellent paint base | ✅ Standard pretreatment (MIL-DTL-5541) | Paint base: both work; 7075 coatings must fully cover — edges and cut surfaces are corrosion initiation points |
| Polishing / mirror finish | Easy to mirror polish | More effort, leaves marks more easily | High-gloss parts: 6061 |
| Plating (nickel/chrome) | ✅ Good | ⚠️ Hydrogen embrittlement and adhesion risk | Plated parts: 6061 |
Anodizing is performed per MIL-PRF-8625 (Type II / Type III); the European counterpart is EN 12373. Conclusion: apart from hardcoat anodizing, 6061 wins at every step of surface treatment. 7075-T6 is a material that is “strength-specialized, appearance-sacrificed.”
Corrosion Resistance by Environment
| Service environment | 6061 | 7075-T6 | Recommendation |
| Dry indoor | Excellent | Good | Both usable bare |
| Marine / salt spray | Good | Poor — SCC risk | 7075 must be coated/anodized; critical parts use 6061 |
| Industrial atmosphere (with SO₂) | Good | Moderate | Coating recommended for 7075 |
| High humidity + sustained load | Good | Susceptible to stress-corrosion cracking | Consider 7075-T73 (trading strength for SCC resistance) |
| Acid/alkali chemical environment | Moderate | Poor | Coating required for both; avoid 7075 |
| Outdoor UV / weathering | Excellent bare | Fully dependent on coating | Outdoor architectural parts: 6061 |
Selection Decision Guide
| Your situation | Choose |
| Part must be welded | 6061 |
| Budget priority / high-volume production | 6061 |
| Marine / high-humidity environment with no additional protection | 6061 |
| Requires yield strength > 350 MPa | 7075-T6 |
| High fatigue / cyclic loading | 7075-T6 (note its higher notch sensitivity; critical moving parts need surface integrity and protection) |
| Weight reduction is critical (aerospace, drones, robotics) | 7075-T6 (specific strength ≈1.77× that of 6061-T6) |
| Structural parts in high humidity + sustained load | 6061, or 7075-T73 |
| Static structural parts, moderate loads | 6061 |
| High-appearance anodized parts | 6061 |
| Heat dissipation is critical (heat sinks, LED housings) | 6061 |
| Requires bending / deep-draw forming | 6061-O or T4 |
| Wear-resistant surface (hardcoat anodizing) | 7075-T6 |
The most common material-selection mistake we see: Engineers default to 7075 because “aerospace grade” sounds more advanced — when the load analysis clearly passes with 6061. The result is paying a material premium of 50%+ (total part cost typically +30–70%) for zero functional gain. Run the loads first, set the safety factor, and if 6061 has margin, use 6061.
Typical Applications
6061: Electronic enclosures, brackets, mounting base plates, tooling fixtures, automotive prototypes, bicycle frames, marine hardware, architectural extrusions, heat sinks.
7075-T6: Aerospace fittings and structural parts, military hardware, drone load-bearing structures, climbing equipment, racing and robotics parts, high-load tooling and dies.
Frequently Asked Questions
Is 7075 stronger than 6061?
Yes, and by a wide margin. 7075-T6 has a tensile strength of about 572 MPa (83 ksi), roughly 1.8× that of 6061-T6 plate/bar (about 310 MPa, 45 ksi); yield strength is about 503 MPa (73 ksi) versus about 276 MPa (40 ksi). But the two alloys have almost identical elastic moduli (about 69–72 GPa), so 7075 is not a stiffness upgrade.
Can 7075 aluminum be welded?
Conventional fusion welding is not recommended: with its high zinc and copper content, 7075 is prone to hot cracking during welding, and heat-affected-zone strength drops sharply. Use riveting, bolting, or adhesive bonding instead — or simply specify 6061 for welded parts.
How much more expensive is 7075 than 6061?
At the raw material level, 7075 typically runs 1.5–2.5× the price of 6061 (up to 3× for aerospace certified material). Once cutting speed, tool consumption, and yield differences are factored in, finished part total cost is typically 30–70% higher, depending on part geometry and volume.
What does the “T6” temper mean?
T6 denotes solution heat treatment plus artificial aging to peak strength. The industry default temper for 6061 is T6; T651 adds a stress-relief stretch on top of T6 for dimensional stability in precision-machined plate. The 7075 T73 temper trades part of its strength for markedly better stress-corrosion cracking resistance.
Is 7075 worth the extra cost?
Only when your load analysis or specification genuinely requires it. For the vast majority of general-purpose parts, 6061-T6 delivers sufficient strength at a far lower total cost — and outperforms across welding, corrosion resistance, and surface treatment.
Which is better for CNC machining?
6061 machines faster, with less tool wear and better surface consistency, making it the better default for most parts. 7075-T6 also machines well, but requires reduced spindle speeds and tighter process control — specify it when strength requirements, rather than machinability, drive the design.
Does 7075 anodize as well as 6061?
Both can be anodized, but 6061 offers far better color uniformity and appearance than 7075. 7075 tends to darken with batch-to-batch color variation, making decorative Type II anodizing risky — but its hardcoat anodizing (Type III) performs excellently and suits wear applications.
Quote Both Materials in Parallel
Not sure which alloy your part should use? Upload your STEP / IGES / SLDPRT / X_T files or PDF drawings, and within 1 business day we will provide parallel quotes for both 6061 and 7075-T6, along with a DFM review — pointing out exactly which features genuinely require 7075 and which can use 6061 to save cost without affecting performance. NDAs can be signed first for confidential drawings. Every order ships with a material certificate (Mill Test Report / EN 10204 3.1) and full batch traceability.
One-line takeaway: Strength is a requirement, not a default. Let the load case choose the alloy.