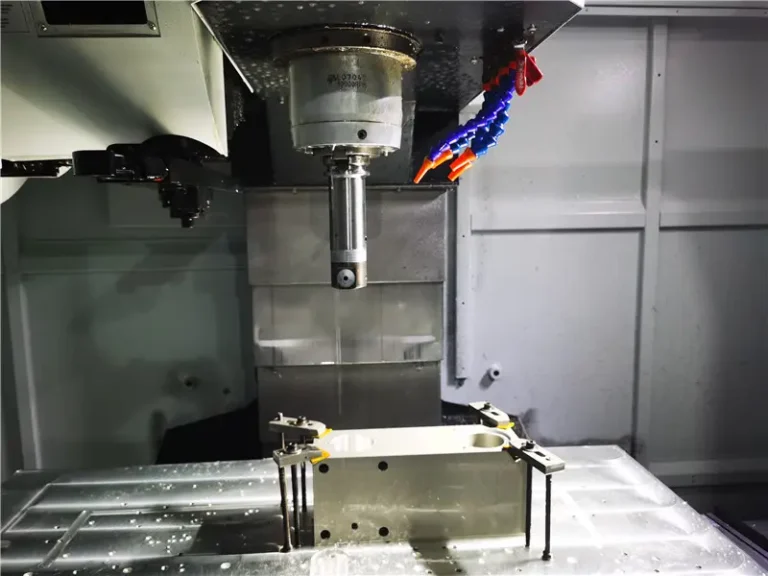
3-Axis CNC Machining Services
Custom metal and plastic parts milled to your drawing, from functional prototypes to repeat production. Weldo machines accessible profiles, pockets and hole patterns with a process planned around your material, geometry and critical dimensions.
- Metal & plastic parts
- Drawing-based precision
- От прототипа до производства
What Is 3-Axis CNC Machining?
A rotating cutting tool moves relative to the workpiece along the X, Y and Z linear axes. Coordinated movement removes stock to create flat faces, steps, pockets, slots and accessible three-dimensional contours.
Tool orientation stays fixed during a standard 3-axis setup. Features on other faces may need repositioning; undercuts and difficult angled features can require special tooling or another process.
Profiles & pockets
Machine outlines, slots, recesses and locating features accessible from the cutting direction.
Depth & contours
Control steps, pocket floors and reachable curved surfaces with suitable cutters and toolpaths.
Drilling & tapping
Add holes and threads from the available machining direction, with depth and access checked during review.
Materials for 3-Axis CNC Machining
Compare metals and engineering plastics by strength, stiffness, wear, chemical exposure and service temperature. Expand each material for grades, uses and machining considerations.
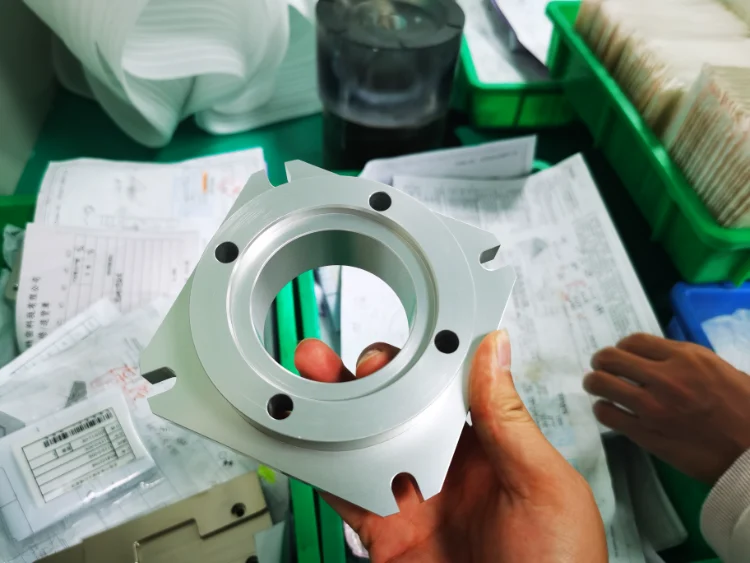
Алюминий
Low weight and good machinability make aluminum a practical choice for pockets, plates and structural parts.
View material details
- Распространенные сорта
- 6061, 6082, 7075, 2024, 5052, 6063, MIC-6
- Типовые детали
- Brackets, housings, mounting plates and prototype fixtures.
- Machining considerations
- Thin walls and large pockets can move as residual stress is released. Select the temper and plan the stock-removal sequence.
- Варианты отделки
- Anodizing, bead blasting, brushing or powder coating; suitability depends on the alloy.
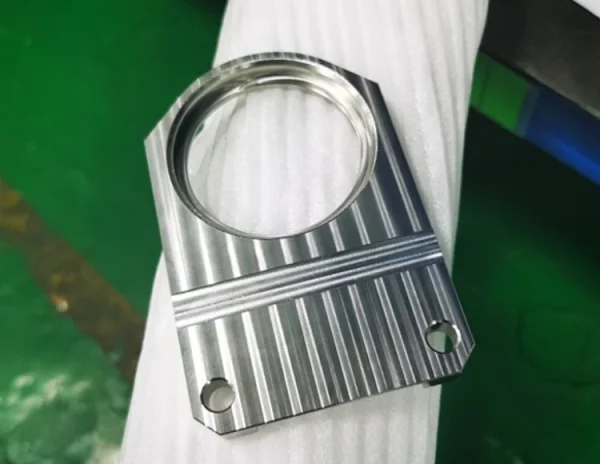
Нержавеющая сталь
Corrosion-resistant grades suit durable parts; machinability varies with alloy and heat-treatment condition.
View material details
- Распространенные сорта
- 304, 316, 410, 420, 440C, 17-4 PH, 2205
- Типовые детали
- Equipment housings, manifolds, mounting blocks and medical-equipment components.
- Machining considerations
- Control heat and work hardening with suitable tooling, chip load and coolant. Specify the required material condition.
- Варианты отделки
- Passivation, bead blasting, brushing or polishing.
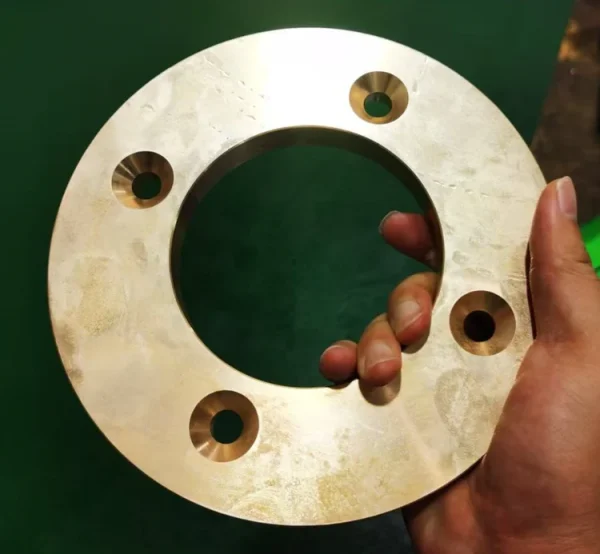
Copper & Copper Alloys
High conductivity is useful for electrical and thermal components; pure copper can be ductile and prone to burrs.
View material details
- Распространенные сорта
- C101, C110 and grade-specific copper alloys
- Типовые детали
- Electrical contacts, heat-transfer components and conductive mounting blocks.
- Machining considerations
- Use sharp tools and reliable chip evacuation. Brass and beryllium-copper grades require distinct process choices; identify the exact alloy.
- Варианты отделки
- Deburring, polishing or specified plating.

Бронза
Copper-based bronze alloys offer useful wear, sliding and corrosion properties, depending on the grade.
View material details
- Распространенные сорта
- Tin bronze, aluminum bronze, silicon bronze
- Типовые детали
- Wear plates, valve components, bearing blocks and locating parts.
- Machining considerations
- Confirm the alloy and stock form. Machinability and tool wear differ substantially between bronze grades.
- Варианты отделки
- Deburring, polishing or compatible protective plating.
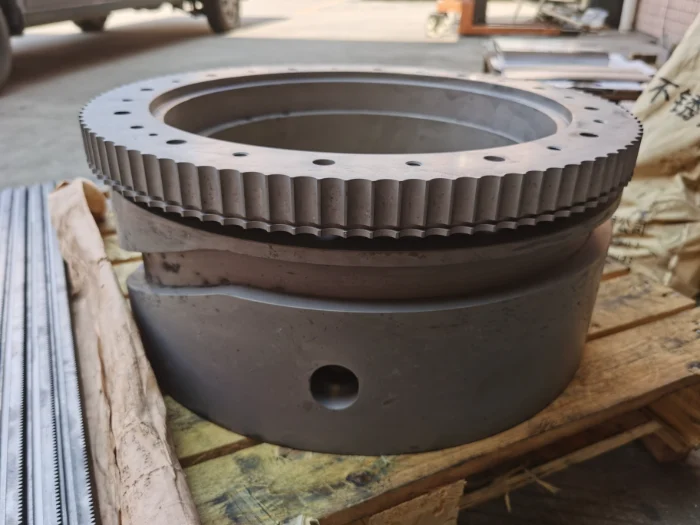
Сталь
Carbon, alloy and tool steels provide a wide range of strength, toughness and wear resistance.
View material details
- Распространенные сорта
- S45C, 4130, 4140, H13, D2, A2, M2
- Типовые детали
- Tooling plates, fixtures, machine brackets and hardened wear components.
- Machining considerations
- Plan machining around heat treatment, hardness and distortion. Most carbon and alloy steels need corrosion protection.
- Варианты отделки
- Black oxide, plating, paint or selected PVD coatings.
Магний
Very low density and good machinability support weight-sensitive housings and structural parts.
View material details
- Распространенные сорта
- AZ31, AZ91, ZK60, WE43
- Типовые детали
- Lightweight enclosures, brackets and equipment components.
- Machining considerations
- Chip collection, fire precautions and coolant selection require a magnesium-specific machining plan.
- Варианты отделки
- Conversion coating, compatible anodizing or protective painting.
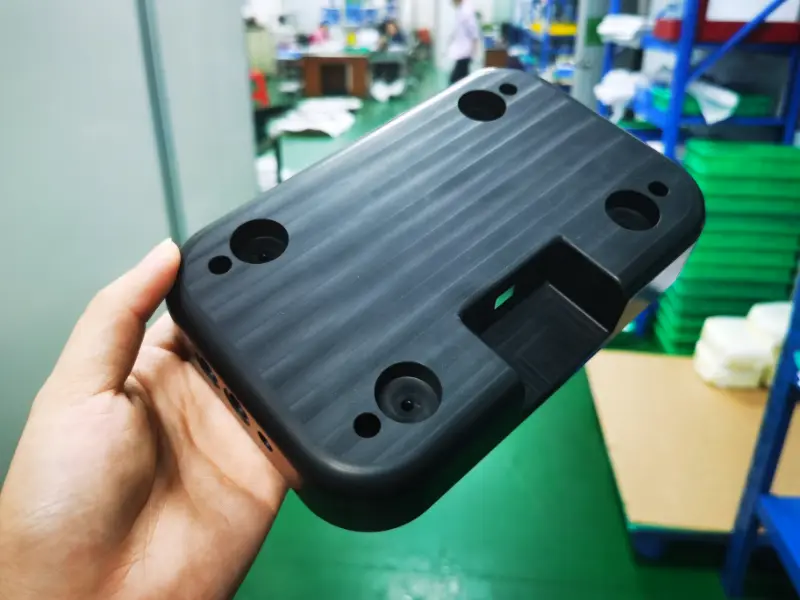
ABS
A tough, economical plastic for functional prototypes and enclosure components.
View material details
- Распространенные сорта
- General-purpose, high-impact and heat-resistant grades
- Типовые детали
- Covers, equipment housings and interior brackets.
- Machining considerations
- Manage cutting heat and clamping pressure to avoid softening, distortion or surface marking.
- Варианты отделки
- Deburring, sanding, painting or compatible printing.
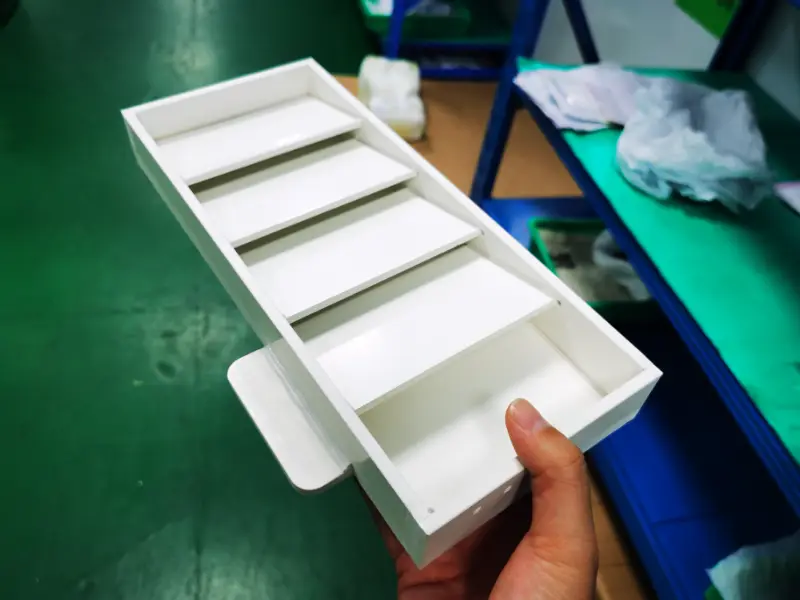
ПВХ
Rigid PVC offers chemical resistance for many wet-process and equipment applications.
View material details
- Распространенные сорта
- Rigid PVC; other grades by review
- Типовые детали
- Chemical-equipment housings, manifolds and mounting components.
- Machining considerations
- Control heat and chip removal; do not overheat the polymer. Confirm chemical compatibility for the actual service conditions.
- Варианты отделки
- Deburring and compatible painting or printing.

POM / ацеталь
Low friction, good machinability and useful dimensional stability suit precision mechanical components.
View material details
- Распространенные сорта
- POM-C, POM-H
- Типовые детали
- Gears, guide blocks, bushings and fixture components.
- Machining considerations
- Avoid excessive clamping and uneven stock removal. Account for temperature when inspecting tight fits.
- Варианты отделки
- Fine machining and deburring; coating or bonding needs special surface preparation.

ПММА / Акрил
A transparent plastic for optical covers and visual prototypes; machined surfaces need finishing for clarity.
View material details
- Распространенные сорта
- Clear, colored and impact-modified grades
- Типовые детали
- Windows, light guides, display covers and inspection panels.
- Machining considerations
- Sharp tools and gentle clamping reduce chipping and cracking. Check chemical and solvent compatibility.
- Варианты отделки
- Mechanical polishing; other clarity treatments depend on geometry and stress.
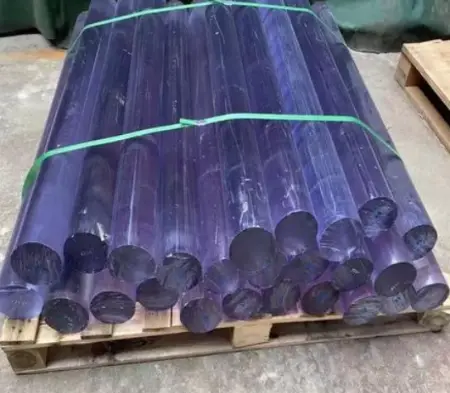
PC / Polycarbonate
High impact strength makes PC useful for tough covers and transparent protective components.
View material details
- Распространенные сорта
- General-purpose and selected modified grades
- Типовые детали
- Guards, electronic housings and impact-resistant equipment covers.
- Machining considerations
- Control heat and residual stress. Some solvents and finishing processes can cause stress cracking.
- Варианты отделки
- Fine machining, compatible polishing or qualified hard coating.
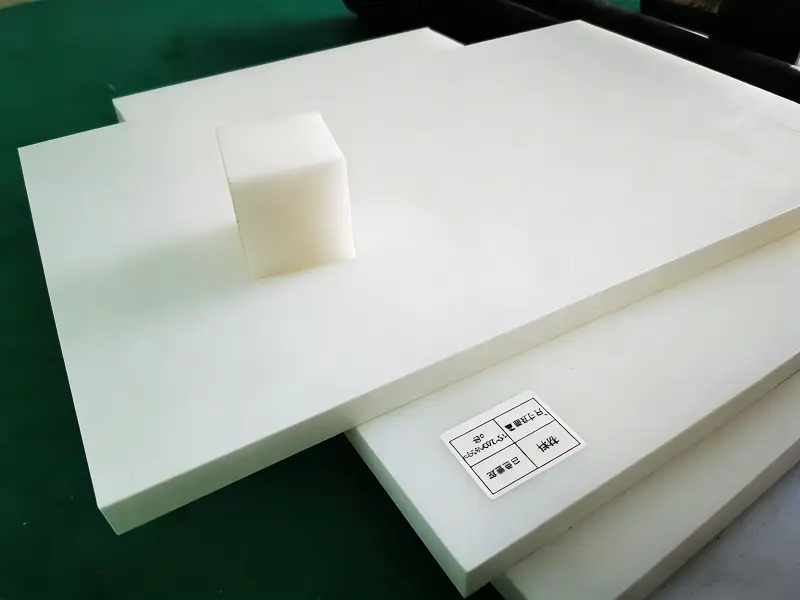
PA / нейлон
Wear resistance and toughness suit sliding and load-bearing mechanical parts.
View material details
- Распространенные сорта
- PA6, PA66; reinforced grades by review
- Типовые детали
- Gears, guides, wear pads and support blocks.
- Machining considerations
- Moisture absorption affects size and fit. Define conditioning and measurement conditions for critical dimensions.
- Варианты отделки
- Deburring and fine machining; coatings require compatibility review.

PE
A chemically resistant, low-friction family used for sliding surfaces and equipment parts.
View material details
- Распространенные сорта
- LDPE, HDPE, UHMWPE
- Типовые детали
- Guides, liners, contact blocks and conveyor components.
- Machining considerations
- Low stiffness and thermal expansion can affect size. Allow for deflection, burr removal and service temperature.
- Варианты отделки
- Clean machining and deburring; adhesion treatments need separate review.

PEEK
A high-performance polymer for elevated-temperature service and demanding chemical environments.
View material details
- Распространенные сорта
- Unfilled, glass-filled, carbon-filled and bearing grades
- Типовые детали
- Insulating components, high-temperature fixtures and wear components.
- Machining considerations
- Manage residual stress and heat. Filled grades are more abrasive; medical uses require grade-specific qualification.
- Варианты отделки
- Fine machining, deburring or qualified surface treatment.
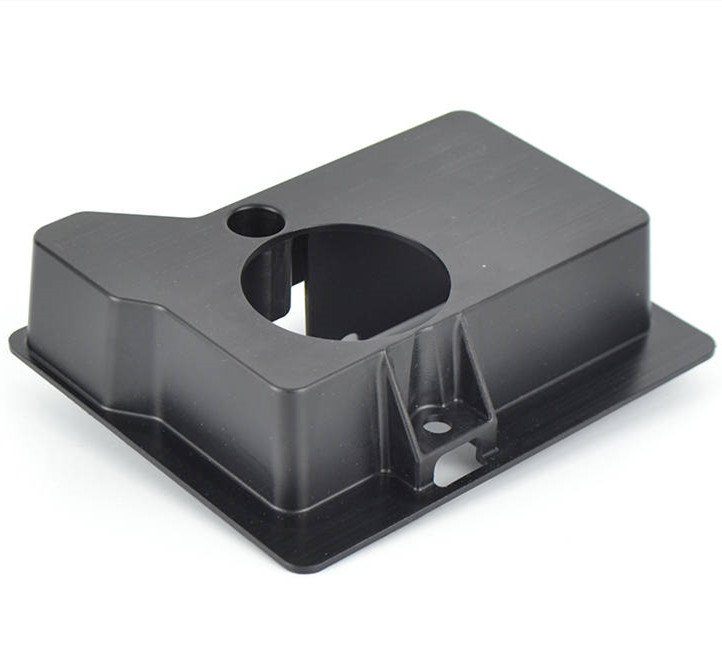
PP
Low density and chemical resistance suit equipment components where high stiffness is not essential.
View material details
- Распространенные сорта
- PP-H, PP copolymers and selected filled grades
- Типовые детали
- Fluid-handling parts, covers, fittings and prototype housings.
- Machining considerations
- Flexible sections can deflect during cutting. Control heat, support the part and allow for thermal movement.
- Варианты отделки
- Deburring and compatible marking; coating requires adhesion review.
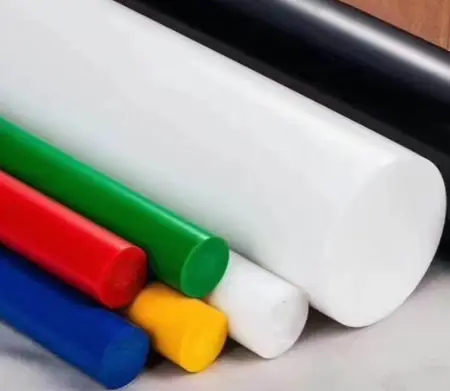
ПНД
HDPE is a polyethylene grade with useful impact strength and chemical resistance.
View material details
- Распространенные сорта
- Standard, UV-stabilized and selected modified grades
- Типовые детали
- Wear strips, fluid-handling blocks, guides and equipment components.
- Machining considerations
- Large thermal expansion and low stiffness limit tight-tolerance stability. Define inspection temperature and service conditions.
- Варианты отделки
- Machined finish and deburring; special preparation is needed for coatings.
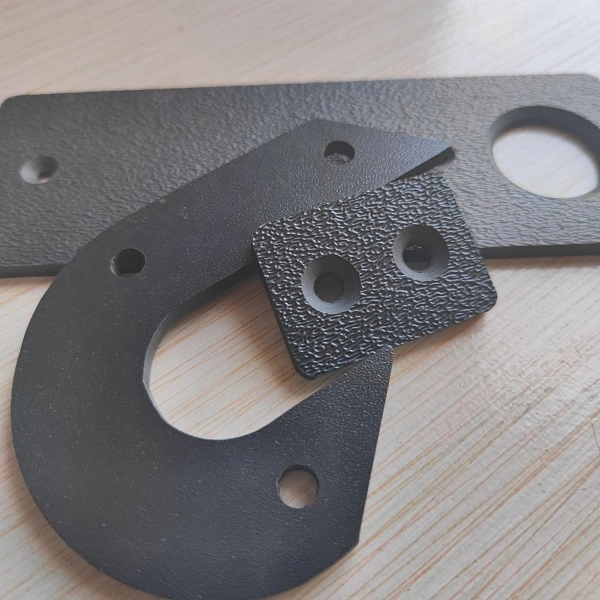
HIPS
An economical, impact-modified polystyrene for appearance models and lightly loaded housings.
View material details
- Распространенные сорта
- Standard and selected modified grades
- Типовые детали
- Display components, covers and product-development prototypes.
- Machining considerations
- Keep cutting temperatures controlled and avoid incompatible solvents; heat resistance is limited.
- Варианты отделки
- Sanding, compatible painting or printing.
Need a different grade or composite? Share its specification for review. Stock availability, machining behavior and finishing compatibility are confirmed with your quotation.
3-Axis CNC Machining Specifications
Key tolerances, finish targets and lead times for your drawing-based project.
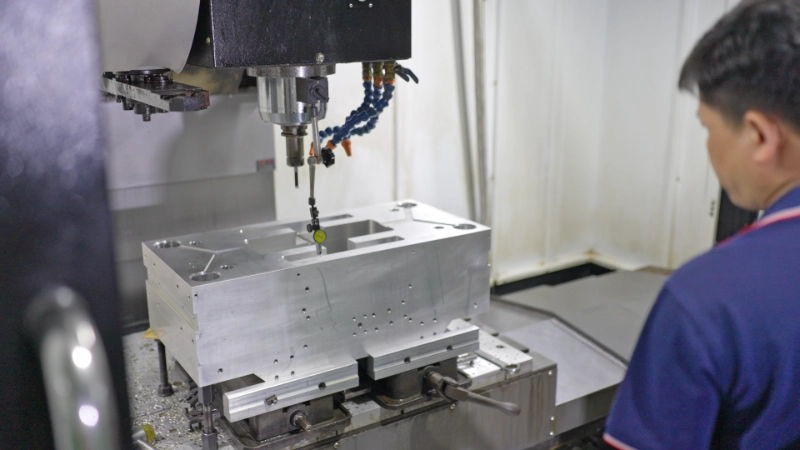
- General tolerances
- ISO 2768-1: class f for metals; class m for plastics, when specified.
- Tolerance examples
- >6–30 mm: ±0.10 (f) / ±0.20 (m).
>30–120 mm: ±0.15 (f) / ±0.30 (m).
All values in mm. - Precision features
- Down to ±0,005 мм on selected metal features.
- Шероховатость поверхности
- Down to Ra 0,8 мкм on selected fine-milled metal surfaces.
- Inspection references
- ISO 1101: geometrical tolerances.
ISO 21920-1: surface-texture indications.
As specified on the drawing. - Время выполнения
- 1-5 дней for eligible prototypes and small batches; finishing and shipping extra.
Drawing callouts take priority. Precision, finish and lead time are subject to part review and quotation confirmation.
Practical Cost
Accessible features and straightforward setups can make three-axis milling an economical choice.
Repeatable Setups
Defined datums, stable fixtures and controlled programs support consistent repeat production.
Combined Operations
Milling, drilling and tapping can be grouped when features are accessible from one setup.
Controlled Toolpaths
Reviewed tool motion and suitable cutting conditions help manage collisions, wear and surface quality.
Design Guidance for Better Machined Parts
Use these starting points to improve tool access and reduce unnecessary machining time. Final limits depend on the complete part and material.
Internal corners
Use the largest practical corner radius. Allow room for a round cutter; sharp internal corners need a relief feature or a secondary process.
Walls & floors
As a starting point, allow about 1.5 mm for metal walls and 2 mm for plastic walls. Feasibility also depends on wall height, support and material.
Отверстия
Use standard drill sizes where possible. Holes deeper than about 5× diameter need additional review for tool reach and chip evacuation.
Темы
Specify the thread standard, size, depth and tolerance class. Required engagement depends on material strength and the fastener load.
Pockets & tool access
Keep pockets accessible from the machining direction. Deep, narrow cavities increase tool overhang, machining time and deflection.
Text & critical features
Use readable engraved text and identify functional datums. Apply tight tolerances to the features that control fit and performance.
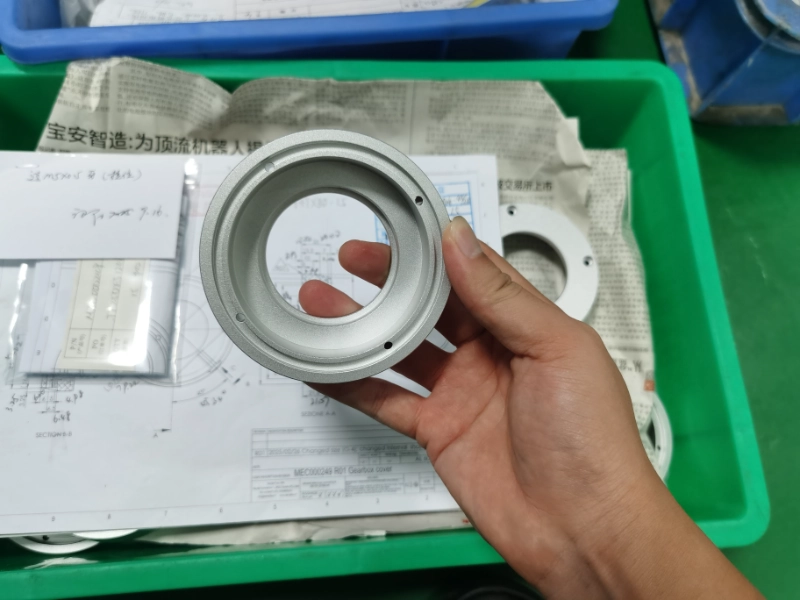
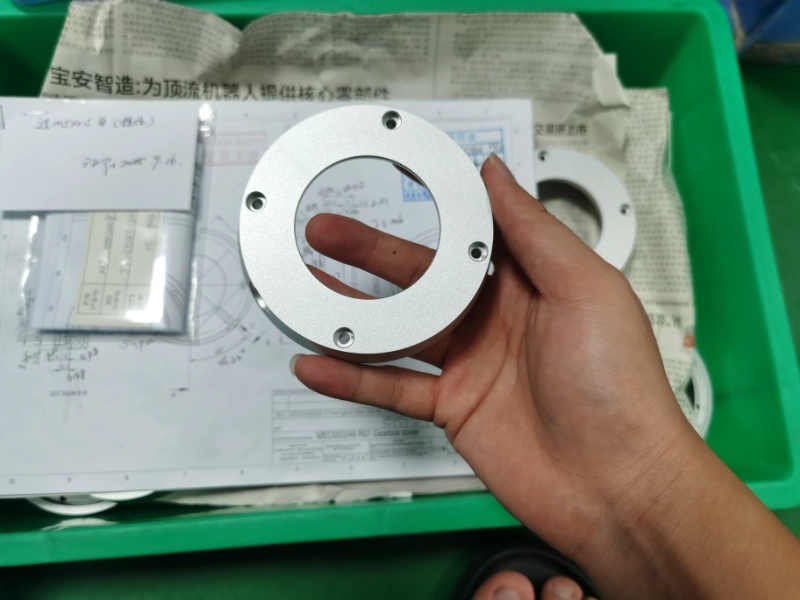
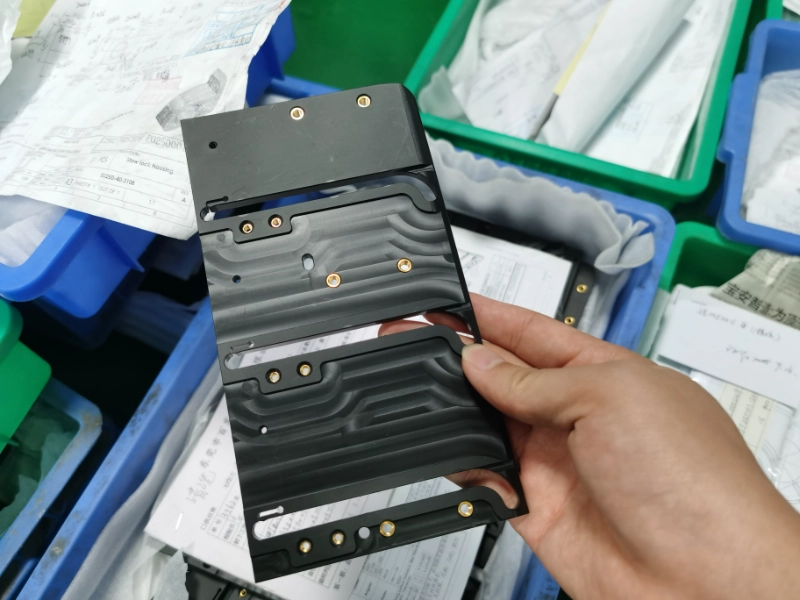
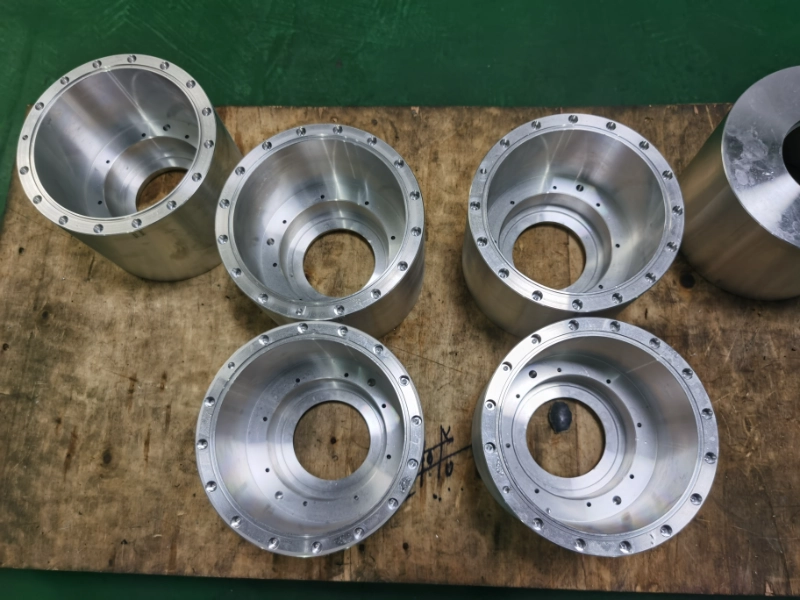
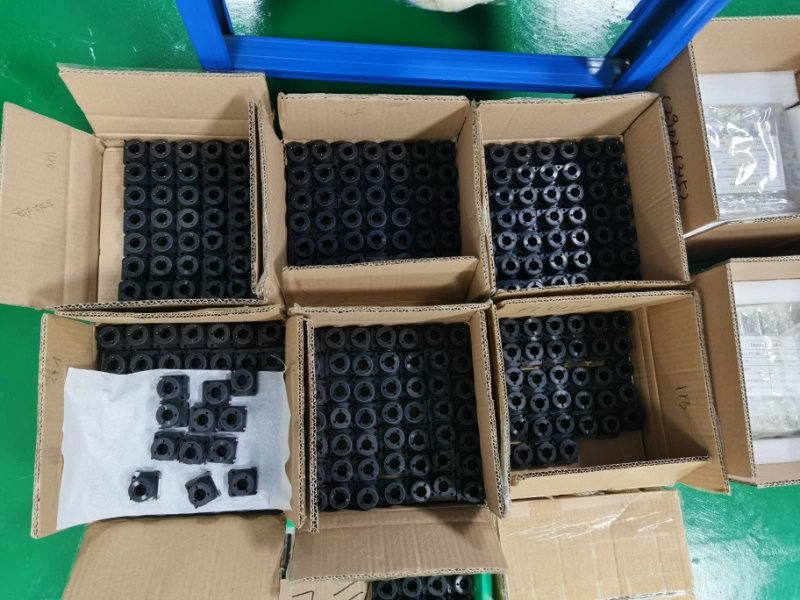
Weldo 3-Axis Machining Projects
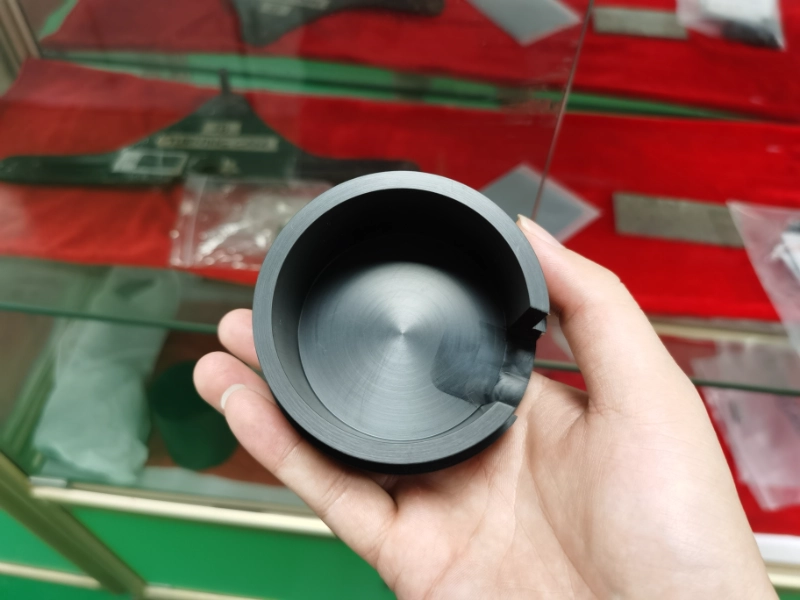
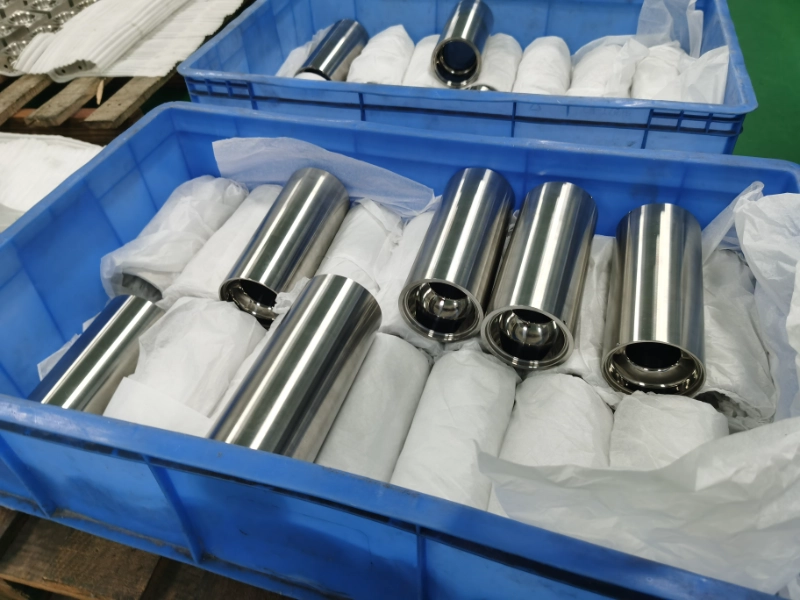
Explore examples from Weldo’s machining work, including metal components, plastic parts and batch production. The gallery shows representative shapes and features for project discussion.
Applications for 3-Axis Milled Parts
Match the manufacturing process to the part geometry, material and qualification requirements.
Automotive & Mobility
Mounting brackets, prototype housings, fixture plates and accessible structural components.
Aerospace Equipment
Sensor mounts, equipment panels and support parts, with material and documentation requirements defined by the project.
Медицинское оборудование
Instrument fixtures, equipment housings and mold components. Patient-contact applications need material and process qualification.
Электроника
Heat sinks, mounting plates, prototype enclosures and connector blocks.
Сельскохозяйственная техника
Blade mounts, wear plates, mounting blocks and service components selected for load and environmental exposure.
Industrial Tooling
Workholding fixtures, locating plates, machine brackets and production aids.
3-Axis CNC Machining FAQ
Practical answers on geometry, accuracy and production planning.
Which parts are suitable for 3-axis CNC machining?
Plates, brackets, enclosures, pockets, grooves, hole patterns and accessible contoured surfaces are common candidates. The tool must be able to reach each feature without interference. Additional faces may require a new setup.
Can a 3-axis machine produce curved surfaces?
Yes. Three-axis interpolation and suitable cutters can machine many three-dimensional contours. The limitation is tool orientation and access, especially around undercuts, steep walls and features on several faces.
When should I choose 5-axis machining instead?
Consider five-axis machining when tilted tool access, complex surface geometry or fewer setups offers a clear benefit. We review the part geometry, datums and cost before recommending a process.
What affects dimensional accuracy?
Machine condition, fixture rigidity, tool wear, heat, material stress and setup changes all matter. Critical dimensions and the inspection method should be agreed before production.
How are cutting parameters selected?
Spindle speed and feed are calculated from the material, tool diameter, cutting speed, tooth count and chip load. Cutter engagement, tool reach, machine power and coolant strategy also influence the final settings; a single RPM range is not suitable for every part.
How do you address broken tools or poor surface finish?
Review tool condition and runout, workholding, chip evacuation and the cutting load. A shorter tool, a more rigid setup or revised roughing and finishing passes may resolve the issue; parameter changes depend on the cause.
How do you support repeat production?
A repeatable fixture, controlled CAM program and defined first-article checks help stabilize production. Multi-part setups and optimized toolpaths can reduce handling and cycle time when the geometry and quantity justify them.
Что нужно отправить для получения ценового предложения?
Send the 3D model, a dimensioned drawing with datums and tolerances, material and condition, quantity, finishing requirements and target date. Highlight fit-critical features and any inspection or traceability requirements.
Let’s Review Your 3-Axis Part
Send your drawing, material and quantity. We’ll review the machining approach and prepare a practical quotation.