Lorsque l'on compare les 7050 vs 7075 aluminum, both alloys are suitable for manufacturing high-strength, lightweight parts.
7075 is well suited to high-strength parts and general machining applications,
while 7050 is preferred for load-bearing structures that require reliable thick-section properties, fracture toughness, and resistance to stress corrosion cracking.
Based on more than ten years of machining experience, I recommend evaluating the alloy designation, temper, stock thickness, loading direction, and operating environment. A thickness of 25 mm is not a fixed dividing line, and thicker stock does not automatically rule out 7075.
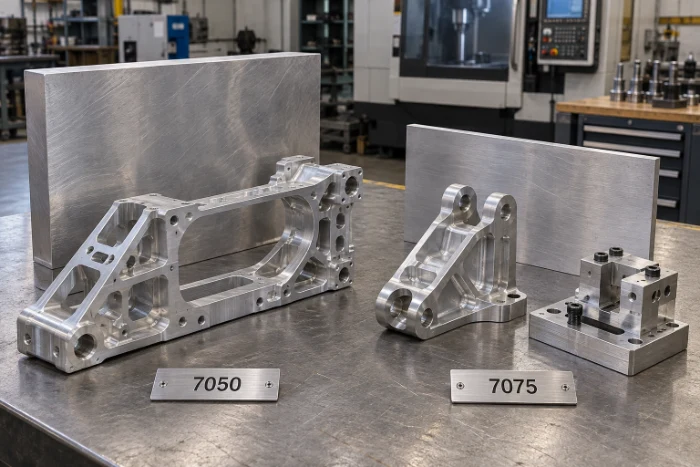
What Are the Core Differences Between 7050 and 7075?
Both are heat-treatable Al-Zn-Mg-Cu aluminum alloys that achieve high strength through solution heat treatment, quenching, and artificial aging.
7075 is widely used for high-strength connectors, mechanical parts, jigs, and fixtures.
The alloy design of 7050 improves the balance between strength, fracture toughness, and corrosion resistance, making it particularly suitable for thick plate and products with large cross sections.
7050 has lower quench sensitivity than 7075. As the cooling rate decreases at the center of thick stock, 7050 retains its properties after heat treatment more effectively. This is an important reason for its use in integral load-bearing structures machined from thick plate, although it does not mean that its strength exceeds that of 7075 in every temper. Alcoa 7050 Technical Data
7050 vs 7075: Comparison of Key Chemical Compositions
The following values are the weight percentages of the main elements, with aluminum making up the balance.
| Élément | Aluminium 7050 | 7075 |
| Zn | 5.7–6.7% | 5.1–6.1% |
| Mg | 1.9–2.6% | 2.1–2.9% |
| Cu | 2.0–2.6% | 1.2-2.0% |
| Cr | ≤0.04% | 0.18–0.28% |
| Zr | 0.08–0.15% | No specified addition range |
| Fe | ≤0,15% | ≤ 0,501 TP3T |
| Si | ≤0.12% | ≤0.40% |
7050 uses zirconium-containing dispersoids to control its microstructure and strictly limits iron and silicon impurities;
7075 primarily uses chromium-containing dispersoids to control its microstructure. The absence of a separately specified zirconium addition range for 7075 does not mean that the material contains absolutely no zirconium. Full chemical composition acceptance should be checked against the applicable specification and the batch material certificate.
Comparison of Key Mechanical Properties
The table below summarizes typical room-temperature values for common plate tempers.
The reference tempers are T7451 and T7651 for 7050, and T651 and T7351 for 7075. The ranges in the table span the typical values for these common material tempers, rather than the performance ranges of all grades.
| Propriété mécanique | 7050 | 7075 |
| Ultimate résistance à la traction | 524–552 MPa | 503–572 MPa |
| Yield strength, 0.2% proof stress | 469–489 MPa | 434–503 MPa |
| Conductivité électrique | Approx. 11% | Approx. 11–13% |
| Ultimate shear strength | 303–324 MPa | 303–331 MPa |
| Dureté Brinell | 140 HB, T7451; 150 HB, T7651 | Approx. 150 HB, T651 |
| Module d'Young | Approx. 70–72 GPa | Approx. 70–72 GPa |
| Coefficient de Poisson | Environ 0,33 | Environ 0,33 |
What Else Should Be Checked for Thick-Section Structures?
Check the raw material thickness, the location from which the part is taken within the plate, and the loading direction. Even when the finished wall is thin, material taken from the center of thick plate remains affected by the heat treatment conditions of the original plate.
Load-bearing frames, thick attachment lugs, and critical joints also require checks of short-transverse properties, fracture toughness, and fatigue requirements. Fracture toughness should be specified together with the test orientation and applicable thickness; a single value cannot represent an entire alloy grade. The conditional value K_Q can be treated as K_IC only after the test validity requirements have been satisfied. ASTM E399
Comparison of Key Physical Properties
The thermal and electrical conductivity data use the same common tempers as the table above.
| Propriété physique | 7050 | 7075 |
| Densité | Approx. 2.83 g/cm³ | Approx. 2.80–2.81 g/cm³ |
| Thermal conductivity, approx. 20°C | 154–157 W/(m·K) | 130–155 W/(m·K) |
| Electrical conductivity, approx. 20°C | 39.5–40.5% IACS | 33–40% IACS |
| Mean coefficient of linear thermal expansion, 20–100°C | Approx. 23.5 × 10⁻⁶/K | Approx. 23.4 × 10⁻⁶/K |
| Specific heat capacity, approx. 100°C | Approx. 860 J/(kg·K) | Approx. 960 J/(kg·K) |
| Magnétisme | Non-ferromagnetic; not attracted to a conventional magnet | Non-ferromagnetic; not attracted to a conventional magnet |
The two alloys have similar coefficients of thermal expansion. Precision shaft-and-bore fits, mounting seats, and assemblies using dissimilar materials should account for dimensional changes caused by the operating temperature difference.
Performance Differences Between Common Tempers
| Material Temper | Performance Characteristics | Selection Priority |
| 7050-T7451 | Combines high strength, fracture toughness, and resistance to stress corrosion cracking | Integral load-bearing structures machined from thick plate |
| 7050-T7651 | Higher strength than T7451, with lower resistance to stress corrosion cracking than T7451 | Structures requiring higher strength while meeting the corresponding corrosion requirements |
| 7075-T6/T651 | High strength, with lower resistance to stress corrosion cracking than T73-type tempers | High-strength parts with controlled corrosion risk |
| 7075-T7351 | Overaged to improve resistance to stress corrosion cracking, with lower strength than T651 | 7075 parts with higher corrosion-resistance requirements |
The “51” in T651, T7351, T7451, and T7651 indicates the specified stress-relief treatment by stretching. It reduces residual stress but does not eliminate it completely.
7075-T6 is solution heat treated and then artificially aged; 7075-T651 adds stress relief by stretching after solution heat treatment, followed by artificial aging. The two have similar strength, while 7075-T651 has lower residual stress and is more favorable for controlling machining distortion.
Comparison of Corrosion and Stress Corrosion Cracking Resistance
Using the common 7050-T7451 and 7075-T651 tempers as examples, 7050-T7451 combines high strength with resistance to stress corrosion cracking and exfoliation corrosion, as well as fracture toughness, making it suitable for thick-section load-bearing structures in humid, salt-containing environments.
The advantage of 7075-T651 is its higher strength. It is suitable for mechanical parts used in dry indoor environments, inside sealed equipment, and in equipment with a complete protective system. When a project needs to retain the 7075 grade while improving resistance to stress corrosion cracking, 7075-T7351 can be selected, with the structural dimensions checked against its strength.
At locations exposed to salt spray, water-trapping crevices, and dissimilar-metal connections, both alloys should have surface treatment, assembly sealing, and drainage measures. Around hole edges, attachment lugs, and interference fits, fillets, interference allowances, and preload should be used to control local tensile stress.
CNC Machining Performance and Distortion Control
7050 and 7075 both support CNC milling, turning, turn-milling, drilling, precision boring, and thread machining, making them suitable for complex surfaces, precision hole patterns, and integral deep-cavity structures.
7050-T7451 is suitable for frames, bulkheads, and large load-bearing parts with curved surfaces machined from thick plate. Its material-selection advantage is the combination of properties within thick sections and fracture toughness, making it suitable for integral parts with substantial material removal and thick load-bearing regions.
7075-T651 is suitable for high-strength brackets with curved surfaces, connectors, mounting seats, and precision tooling. Its typical Brinell hardness is approximately 150 HB, compared with approximately 140 HB for 7050-T7451. Tooling, feed, and finishing allowance should be matched to the actual hardness and structural rigidity during machining.
How Should Machining Stability Be Controlled?
7050-T7451 and 7075-T651 are both stress relieved by stretching, providing a basis for dimensional stability. Prioritize 7050-T7451 for integral load-bearing parts machined from thick plate;
For brackets and tooling where high strength and purchasing economy are priorities, 7075-T651 can be evaluated first.
Large, thin-walled parts in either material should follow the machining sequence below:
- Blank selection: Define the rolling direction, location within the plate, and machining datums.
- Staged rough machining: Balance material removal on both sides and control clamping force and local temperature rise.
- Unclamping inspection and finish machining: Measure distortion in the free state, correct the datums, and then finish critical holes, mating surfaces, and thin-wall dimensions.

Comparison of Surface Treatment Performance for 7050 and 7075
The main reference tempers below are 7050-T7451 and 7075-T651. Under the same performance requirements, some treatments deliver similar results, with the main differences arising from the substrate and coating quality.
1. Conventional Anodisation
The two alloys have the same anodizing response rating, and both are suitable for corrosion protection and coloring. 7050 has a higher copper content, and the two alloys can differ in film color and the distribution of film-formation defects. Actual corrosion resistance is compared using test results obtained after anodizing and sealing.
2. Anodisation dure
Both can receive a hard, wear-resistant anodic film and use the same acceptance requirements for film thickness, wear resistance, and sealing. Differences in wear performance after treatment are mainly reflected in film hardness, defects, and wear loss. Substrate strength advantages and film wear-resistance advantages should be assessed separately.
3. Alodine
Both can meet specified corrosion protection and low electrical contact resistance classes. When the film is damaged and exposed to a corrosive medium, 7050-T7451 retains a stronger underlying resistance to stress corrosion cracking, while 7075-T651 requires closer control of protection integrity in regions under tensile load.
4. Electroless Nickelage
Both can use the same targets for nickel-phosphorus coating hardness and wear resistance. Surface performance is mainly determined by phosphorus content and post-plating treatment. The differences between the grades primarily concern adhesion following pretreatment and the retention of substrate properties after heating, so the plating process needs to be qualified for each material.
5. Primer and Topcoat
Both can use the same grade of coating system, with weathering resistance mainly determined by the coating material, film thickness, and curing quality. When coating damage is followed by corrosion exposure under sustained tensile load, the substrate resistance to stress corrosion cracking of 7050-T7451 is superior to that of 7075-T651.
6. Sablage or Glass Bead Blasting
Both can achieve the same specified matte texture and surface roughness. Based on typical substrate hardness, 7050-T7451 at approximately 140 HB is more susceptible to impact indentations than 7075-T651 at approximately 150 HB. This engineering assessment is used to differentiate blasting parameters, with the final texture confirmed against a sample.
7. Grenaillage de précontrainte
Both improve fatigue performance through surface compressive stress. Based on typical yield strength, 7050-T7451 undergoes surface plastic deformation more readily than 7075-T651. The depth of compressive stress and the fatigue improvement should be determined separately through residual stress measurement and fatigue testing.
you can click here to know the details of shot peening vs sandblasting vs shot blasting.
Joining Methods and Welding Performance
Bolted Connections
Both are suitable for removable load-bearing connections. 7050 is commonly used for thick-section frames, while 7075 is commonly used for high-strength brackets and connecting plates. Hole locations, edge distances, and preload are the key controls.
Riveting
Both are suitable for compact, lightweight permanent connections. 7050 is used for connections in load-bearing frames, while 7075 is used for connecting plates and structural attachments. Hole-wall quality and riveting distortion are the key controls.
Adhesive Bonding
Both are suitable for bonding over large overlap areas, distributing loads and reducing drilling. Bond strength is mainly determined by surface pretreatment, bondline thickness, and curing quality. The adhesive is selected according to operating temperature, humidity, and load.
Soudage
7050 and 7075 are not recommended for load-bearing structures joined by conventional TIG/MIG fusion welding. The main limitations are hot cracking and reduced properties in the heat-affected zone. Preheating or post-weld heat treatment cannot be used as a general guarantee of restoring the original as-delivered properties.
Friction stir welding can join these high-strength aluminum alloys, but joint performance requires separate validation. Structures that specifically require conventional fusion welding should first be evaluated for suitable 5xxx or 6xxx series alloys. TWI Guide to Welding Aluminum Alloys
Contact with Dissimilar Materials
In the presence of moisture or another electrolyte, direct electrical contact with copper alloys, stainless steel, titanium alloys, or carbon fiber increases the risk of galvanic corrosion on the aluminum side. This is not an unconditional prohibition on joining; it requires the connection design to control electrical contact and electrolyte ingress.
Insulating bushings or washers, protective coatings, assembly sealing, and drainage features can be used. Where electrical bonding is required, the conductive contact surfaces and sealing measures should be specified separately.
Applications and Common Parts
7050: Load-Bearing Parts Machined from Thick Stock
7050 is commonly used for aircraft bulkheads, fuselage frames, wing spar components, and large load-bearing joints.
Its advantage is that, when machining parts from thick plate, it provides a better balance of internal strength, crack resistance, and resistance to stress corrosion cracking. This makes it suitable for large integral structures carrying high loads.
7075: High-Strength Mechanical Parts and Tooling
7075 is commonly used for load-bearing brackets, connecting plates, racing mounting seats, and precision fixtures.
7075-T651 can be selected when higher strength is required and the operating environment is dry or well protected;
When resistance to stress corrosion cracking is the higher priority, 7075-T7351 can be selected, with part dimensions checked against its lower strength to confirm that they meet the load requirements.
Cost Comparison: Which Offers Better Value, 7050 or 7075?
When budgeting for common 7050-T7451 and 7075-T651 plate, 7050 usually has a higher material cost, while 7075 is relatively more economical. Obtain a quotation based on blank dimensions, quantity, and inspection requirements to establish the actual price.
| Comparaison | 7050 | 7075 |
| Material purchasing cost | Plus élevé | Relativement plus faible |
| Availability of common sizes | Lower; mainly thick plate and aerospace specifications | Higher; a broader range of general machining sizes |
| Cost priority | Invest in thick-section properties and crack resistance | Balance high strength with machining economy |
Machining Cost Mainly Depends on Part Complexity
Both materials can be cut efficiently. Machining prices are mainly determined by geometry, accuracy, and machining time.
| Complexité des pièces | Typical Geometry | Relative Machining Cost |
| Simple | Flat plates, basic bushings, and a small number of holes and slots | Plus bas |
| Modéré | Hole patterns on multiple faces, steps, and pockets | Modéré |
| Complex | Deep cavities, thin walls, complex curved surfaces, and multiple setups | Plus élevé |
| High-precision complex parts | Tight geometric tolerances, precision fits, and many dimensions to inspect | Haut |
For general brackets, connecting plates, and tooling, evaluate 7075 first to control costs. For integral load-bearing parts machined from thick plate, assess the investment in 7050 against the performance requirements.
FAQ: Further Guidance on Selecting 7050 and 7075
1. How Do 7050 and 7075 Differ When Machining Parts with Complex Curved Surfaces?
7075-T651 is suitable for brackets with curved surfaces, mounting seats, and tooling. 7050-T7451 is better suited to large load-bearing parts with curved surfaces machined from thick plate. Both can be machined using five-axis CNC equipment, with surface profile accuracy and finish controlled through tooling, toolpaths, and workholding.
2. Which Should You Choose for Dry, Humid, and Salt-Spray Environments?
High-strength 7075-T651 can be evaluated first for dry environments. For parts under tensile load in humid or salt-spray environments, evaluate 7050-T7451 or 7075-T7351 first, together with corrosion-protective coatings and assembly sealing.
3. Which Should You Choose for Sustained Loading and Repeated Loading?
7050-T7451 has an advantage over 7075-T651 when parts are under sustained tensile load and exposed to a corrosive medium. For repeatedly loaded parts, select the material using the corresponding fatigue data and reduce crack initiation sites through filleted transitions, smooth hole walls, and good surface quality.
How Should You Choose Between 7050 and 7075?
For high strength and cost control, choose 7075-T651. It is suitable for brackets, connecting plates, precision tooling, and mounting seats, especially in dry environments or well-protected equipment.
For load-bearing thick plate where crack resistance and corrosion resistance matter, choose 7050-T7451. It is suitable for large integral frames, aircraft bulkheads, and thick attachment lugs, combining thick-section properties, fracture toughness, and resistance to stress corrosion cracking.
To use 7075 while improving resistance to stress corrosion cracking, choose 7075-T7351. Its strength is lower than that of T651, so load capacity and part dimensions should be checked again when selecting it.
To use 7050 while pursuing higher strength, evaluate 7050-T7651. Compared with T7451, it has higher strength and lower resistance to stress corrosion cracking, making it suitable for projects where the design has explicitly accepted this performance tradeoff.
Evaluate 7075-T651 first for general mechanical parts and 7050-T7451 first for critical load-bearing parts machined from thick plate. Where an existing drawing specifies the material, purchase the specified grade and temper, and obtain confirmation from the designer before making a substitution.
Weldo Machining provides a complete range of multi-axis CNC machining, precision grinding, wire EDM cutting, and surface finishing services. Submit your drawing, quantity, and operating environment to discuss how to match 7050 or 7075 to your requirements and obtain a quotation.